
Product
- Core Customization Service
- Health Care
- Electronic Appliances and Instruments
- Maternal and Child Supplies Molds
- Recreational Sports
- Home Furnishing Art
- Auto Accessories
- Transportation and Warehousing
- Lighting Fixtures
- Construction Equipment
- Packaging Product
- Educational & Laboratories
- Clothing Luggage Accessories
- Care and Cleaning Products
- Agriculture & Forestry
- Mechanical Equipment
- Pet Supplies
- Kitchenware
Digital calculator housing moulding
Ningbo (P&M) Plastic Metal Products Co., Ltd. has 17 years of mold manufacturing technology and can customize Digital calculator housing moulding. We provide professional customized Digital calculator housing moulding services, and we are a professional Digital calculator housing moulding manufacturer. We have sufficient experience in selecting product raw materials and mold materials..
Send Inquiry
Product Description
In the process of customizing Digital calculator housing moulding, our factory can provide one-stop service. We have design and production capabilities related to Digital calculator housing moulding, such as: CAD design, mold manufacturing, injection molding, plastic product production, assembly and other technologies. In addition, our company has established cooperative relationships with plastic raw material suppliers, printing manufacturers, etc. to ensure the supply of raw materials and printing quality. Through our rich experience and perfect supply chain, our company can provide customers with high-quality customized Digital calculator housing moulding products to meet their specific needs. At the same time, we have 10 years of professional foreign trade service experience, understand the foreign trade process, and better serve our customers. For Digital calculator housing moulding products, we can make corresponding plastic parts, which is mainly done through injection molds.
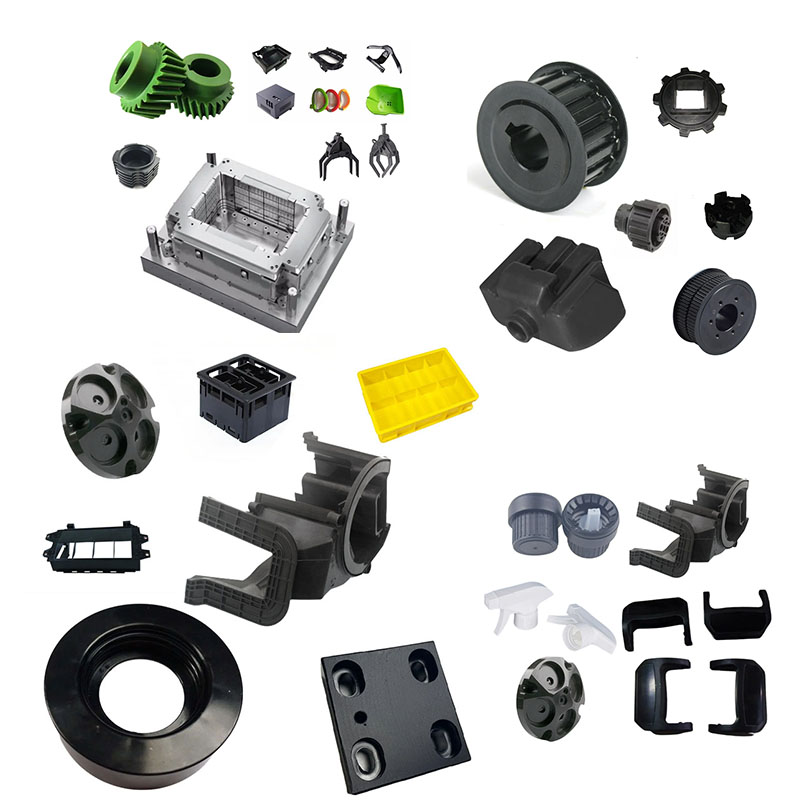
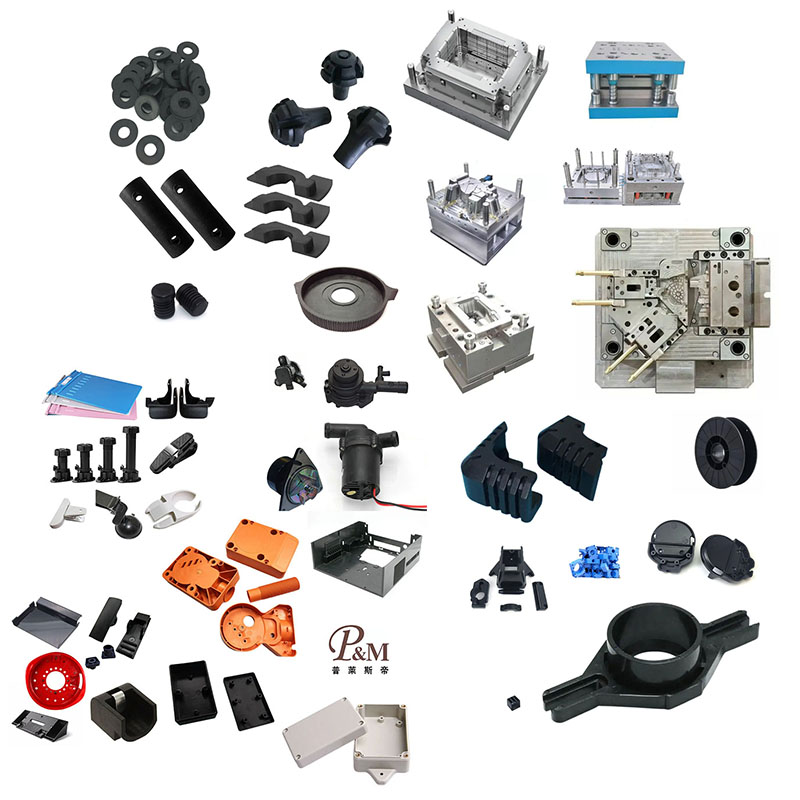
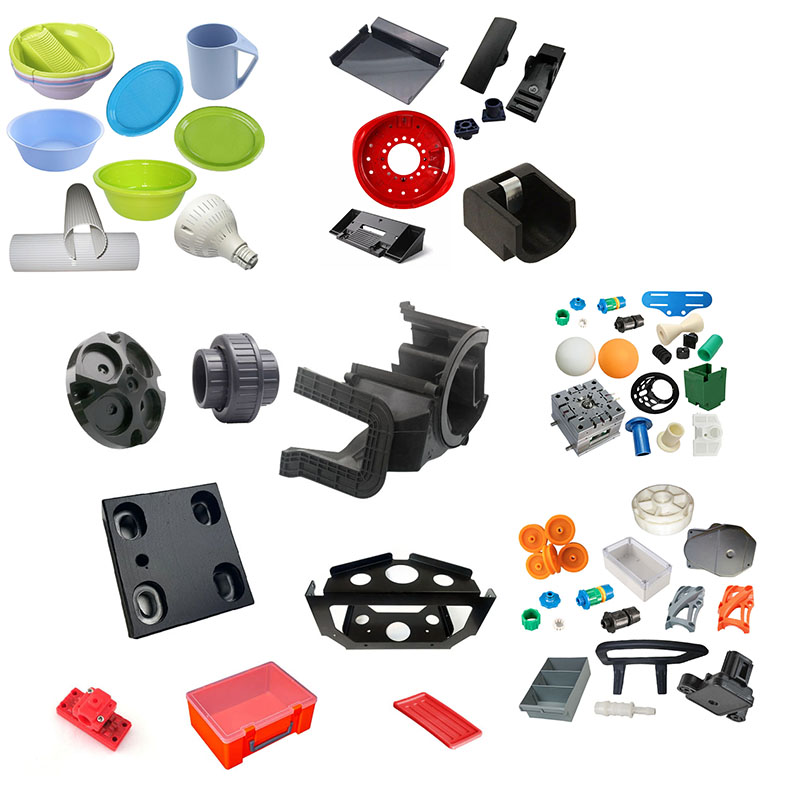
Key Points for Calculator Housing Injection Molding (Consumer electronics for export; primarily ABS; focus: aesthetics, button apertures, top/bottom shell mating, and warpage control)
I. Material Selection (Standard calculators: ABS)
1. **Standard student/office calculators:** **High-flow ABS** (MFR ≥ 22g/10min); shrinkage rate **0.4%–0.5%**. Shrinkage varies between the top and bottom shells due to differences in the number of apertures (the top shell, with many button holes, tends to shrink less, while the bottom shell shrinks slightly more). **Ideally, use separate molds for each part rather than a combined mold.**
2. High-end/drop-resistant models: **PC/ABS alloy** (drop-resistant, superior dimensional stability, higher cost); PP is rarely used (too soft, snap-fits tend to loosen).
3. Environmental compliance: **RoHS** compliance is mandatory for exports; some clients require halogen-free materials.
4. Drying: ABS at 80°C for 2–4 hours; moisture content <0.05%. **Failure to dry properly easily leads to silver streaks, surface splash marks, and brittleness/cracking.**
>
> Recommended wall thickness: **1.4–1.8mm** (1.5mm is most common); keep thickness variation within 25% to prevent warpage caused by uneven shrinkage. > Rib thickness: **0.5–0.6 times the main wall thickness** to prevent sink marks on the outer surface; rib height ≤ 3 times wall thickness; root fillet radius ≥ 0.3mm.
II. Mold Design Priorities (Calculators are the most challenging: numerous small button holes + display window + snap-fits)
1. Gates and Runners
- Common choice: **Pin-point gate**, located on the back or at a corner to ensure no gate marks on the cosmetic surface; multi-cavity molds require **runner balancing** to ensure consistent part weight across cavities.
- Direct large gates on the front surface are not recommended; they leave large scars that interfere with printing or screen printing.
- Small calculators: 2-cavity or 4-cavity; high-volume production: 8-cavity. **Hot runner systems (valve gate type)** are essential to reduce gate waste, shorten cycle times, and minimize weld lines—ideal for high-volume export orders.
### 2. Button Holes & Lifters (Core Challenge)
The front housing features dozens or hundreds of square button through-holes; **lifters must be used for all of them**—relying solely on inserts is insufficient. Lifters require slow-feeding wire-cut EDM processing with a fit clearance of 0.01–0.02mm to prevent **flash, material jamming, or scratching of the hole walls**.
- Lifter angle: 3°–5°; lifters for small square holes must be polished to ensure smooth demolding.
- Large display window through-hole: Use inserts + venting to prevent burning and short shots.
>
> Critical Pitfall: Thin wall sections around button holes are prone to **short shots, burning, and burrs**; venting channels must be placed at the hole edges.
3. Venting (Easily Overlooked)
Calculators have many holes, leading to severe trapped air issues:
- Parting line venting channels: 0.015–0.02mm deep, 3–5mm wide.
- Provide separate venting for lifters, inserts, and button-hole areas to prevent burn marks, short shots, and air bubbles.
4. Cooling & Warpage Control (Mating seam between upper and lower shells is a frequent source of customer complaints)
- **Independent cooling circuits** for upper and lower shells; maintain mold temperature differential <5°C (uneven mold temperature leads directly to warpage and inconsistent mating seam gaps).
- Mold core materials: P20/718H; S136 (polished) for high-gloss surfaces; 718 (pre-hardened) for standard matte surfaces.
- Draft angles: 1°–1.5° for cosmetic surfaces; 0.5° for internal ribs; minimum 0.3° for inner walls of button holes to prevent surface scuffing/dragging.
5. Key Dimensions for Mold Fitting
- Mating interface (snap-fits) between upper and lower shells: Allow a **0.02–0.03mm** clearance per side (too tight causes scuffing/whitening during assembly; too loose results in large gaps).
- Screw bosses: Outer diameter ≤ 2× wall thickness; design a "crater" (recess) at the base to prevent sink marks on the outer surface; apply a fillet radius (R-angle) at the base of self-tapping screw bosses.
III. Injection Molding Process Parameters (ABS Reference)
1. Barrel temperature: 210–240°C; Mold temperature: 60–80°C.
2. Multi-stage injection: **Low speed through the gate → Medium speed to fill button-hole areas → Low speed at the end** to avoid weld lines, jetting marks, and burning.
3. Holding pressure: Two-stage holding; high pressure first to compensate for shrinkage, followed by low pressure to maintain stability; **excessive holding pressure causes high internal stress, leading to cracking after screen printing**.
4. Cooling: Ensure uniform cooling; insufficient cooling leads to continued shrinkage and warpage after ejection.
5. Slow ejection speed; thin-walled parts are prone to stress whitening or deformation at ejection points; distribute ejector pins evenly and place additional pins near button holes.
IV. Common Defects & Countermeasures (High-frequency issues with calculator housings)
1. **Warpage and uneven seam between upper and lower shells**: Uneven wall thickness / significant left-right mold temperature difference / excessive holding pressure; optimize cooling, reduce holding pressure, add reinforcing ribs.
2. **Burrs or flash at key openings**: Excessive clearance in angle lifters / insufficient clamping force / excessively high melt temperature; adjust mold fit to tighten angle lifter clearance.
3. **Surface flow marks and silver streaks**: Material not dried / incorrect gate location; ensure thorough drying, adjust injection speed.
4. **Scorching near key openings**: Trapped air; add venting to inserts/angle lifters, reduce injection speed.
5. **Cracking after screen printing or laser engraving**: Excessive internal stress; reduce holding pressure, appropriately increase mold temperature, perform annealing if necessary.
6. **Sink marks (on the reverse side of screw bosses)**: Bosses are too thick; create a "crater" (recess) around the base, reduce boss wall thickness.
We are a Digital calculator housing moulding manufacturer, providing high-quality Digital calculator housing moulding manufacturing. As long as you want to customize/develop Digital calculator housing moulding products, you can find us. We have professional injection mold design and mature manufacturing technology, providing you with one-stop service, from product design-mold making-product production-product packaging-product transportation, we can help you in every link. As long as you come to us, we will provide you with the ultimate service and satisfy you in terms of product quality, production time, information dialogue, etc.
|
Product Name |
Treadmill moulding |
|
Pls provide |
2D, 3D, samples, or the size of the multi-angle pictures |
|
Mould Time |
20-35 Days |
|
Product time |
7-15 Days |
|
Mould precision |
+/-0.01mm |
|
Mould life |
50-100 million shots |
|
Producing Process |
Audit drawings - mold flow analysis - design validation - Custom Materials - mold processing - core processing - electrode machining - Runner system processing - parts processing and procurement - machining acceptance - cavity surface treatment process - complex mode Die - The entire mold surface coating - Mounting plate - mold sample - sample test - sending samples |
|
Mould cavity |
One cavity, multi-cavity or same different products be made together |
|
Mould material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Runner system |
Hot runner and cold runner |
|
Base material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Finish |
Pitting the word, mirror finish, matte surface, striae |
|
Standard |
HASCO, DME or dependent upon |
|
Main technology |
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes, surface Finish, etc. |
|
Software |
CAD,PRO-E,UG Design Time: 1-3 days (normal circumstances) |
|
Product material |
ABS,PP,PC,PA6,PA66,TPU,POM,PBT,PVC,HIPS,PMMA,TPE,PC/ABS,TPV,TPO,TPR,EVA,HDPE,LDPE,CPVC,PVDF,PPSU.PPS. |
|
Quality system |
ISO9001:2008 |
|
Establish time |
20days |
|
Equipment |
CNC,EDM,Cutting off Machine,plastic machinery,etc plastic suitcase mould zhe jiang |


Plastic Injection Mould making

Plastic molding specifications

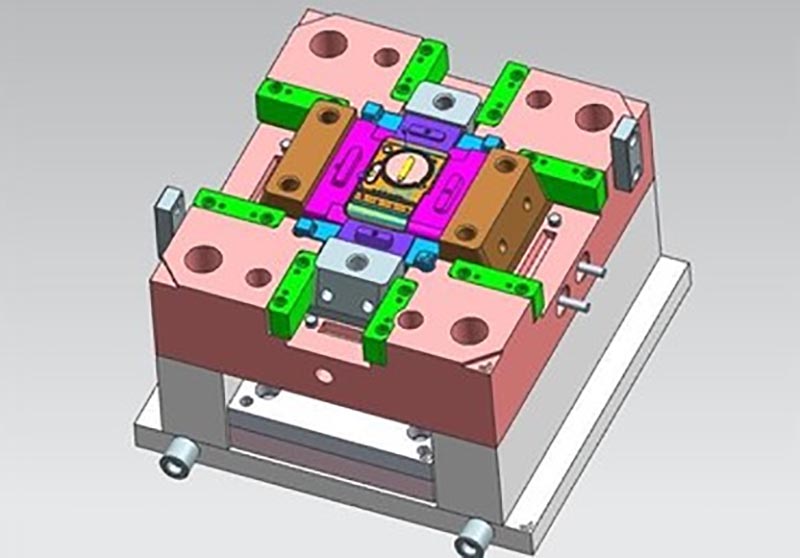
Mold design:



Transaction process:

Mold testing:


Product packaging

Factory
We are Custom Plastic Mold factory. Our factory is plastic injection mold maker. we has 17 years of experience in professional custom plastic mold and 10 years of foreign trade experience. We are custom Plastic Mold supplier. We can provide custom Plastic Mold service. Our factory can make the Injection molded plastic parts, and the quality of the products will satisfy you.
We have more than 50 high-end machines and hundreds of engineers and designers. We can provide one-stop service, from product design - mold making - product production - product packaging - transportation. We have a complete production chain. We can meet all your requirements.
Services we provide:
Professional custom mold service, Plastic mold design and manufacturing .plastic product production, product design, mold design, blow mold customization, rotational mold customization, die-casting mold customization. 3D printing services, CNC manufacturing services, product packaging, customized packaging, shipping services.










We always adhere to the principles of quality first and time first. While providing customers with the highest quality products, try to maximize the production efficiency and shorten production time. We are proud to tell every customer that our company has not lost any customer since its establishment.If there is a problem with the product, we will seek a solution actively and take responsibility to the end.

FAQ
Q1: Are you trading company or manufacturer ?
A: We are manufacturers.
Q2. When can I get the quotation?
A: We usually quote within 2 days after we get your inquiry.
If you are very urgent, please call us or tell us in your email so that we can quote for you first.
Q3. How long is the lead-time for mold?
A: It all depends on the products' size and complexity. Normally, the lead time is 25 days.
Q4. I have no 3D drawing, how should I start the new project?
A: You can supply us a molding sample, we will help you finish the 3D drawing design.
Q5. Before shipment, how to make sure the products quality?
A: If you don't come to our factory and also don't have the third party for inspection, we will be as your inspection worker.
We will supply you a video for production process detail include process report, products size structure and surface detail, packing detail and so on.
Q6. What is your payment terms?
A: Mold Payment: 40% deposit by T/T in advance, 30% second mold payment before sending out the first trial samples, 30% mold balance after you agree the final samples.
B:Production Payment: 50% deposit in advance, 50% before sending out the final goods.
Q7: How do you make our business long-term and good relationship?
A:1. We keep good quality and competitive price to ensure our customers benefit for best quality products.
2. We respect every customer as our friend and we sincerely do business and make friends with them, no matter where they come from.
Hot Tags: Digital calculator housing moulding, China, Manufacturer, Supplier, Factory, Customized, Wholesale, Buy, Quality, Latest Selling, Made in China
Related Category
Send Inquiry
Please feel free to give your inquiry in the form below. We will reply you in 24 hours.