
Product
- Core Customization Service
- Health Care
- Electronic Appliances and Instruments
- Maternal and Child Supplies Molds
- Recreational Sports
- Home Furnishing Art
- Auto Accessories
- Transportation and Warehousing
- Lighting Fixtures
- Construction Equipment
- Packaging Product
- Educational & Laboratories
- Clothing Luggage Accessories
- Care and Cleaning Products
- Agriculture & Forestry
- Mechanical Equipment
- Pet Supplies
- Kitchenware
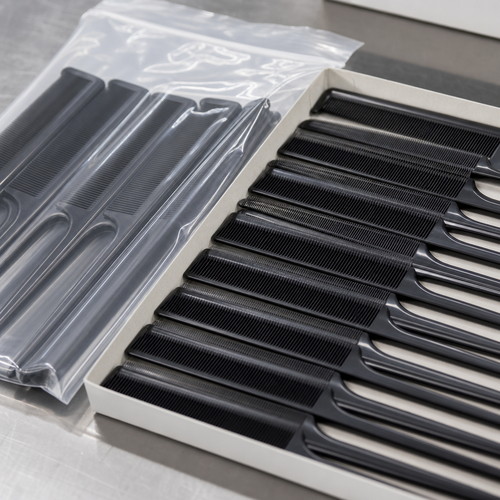
Parting Combs Custom
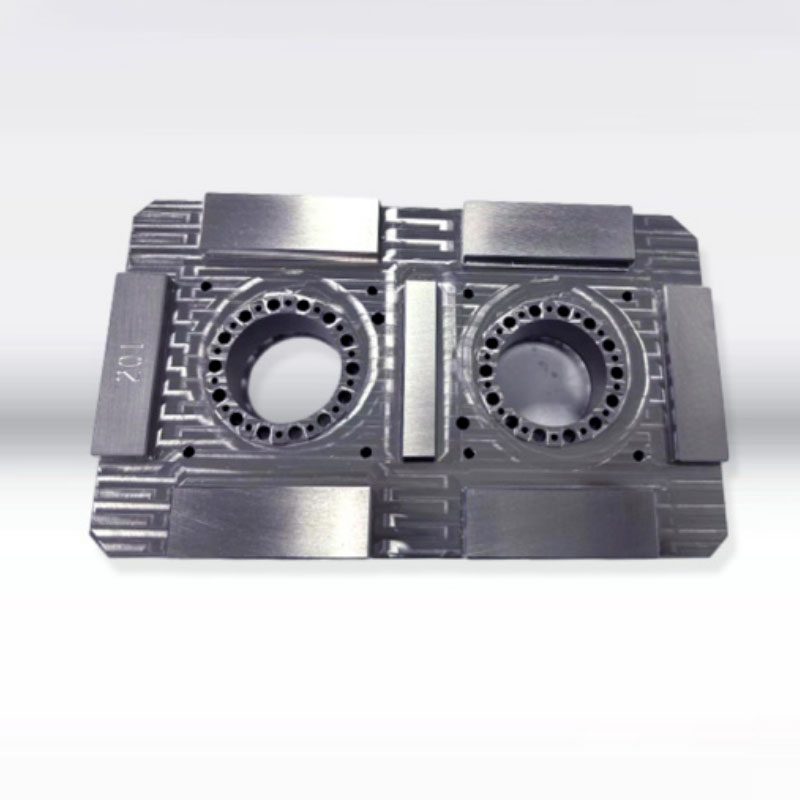
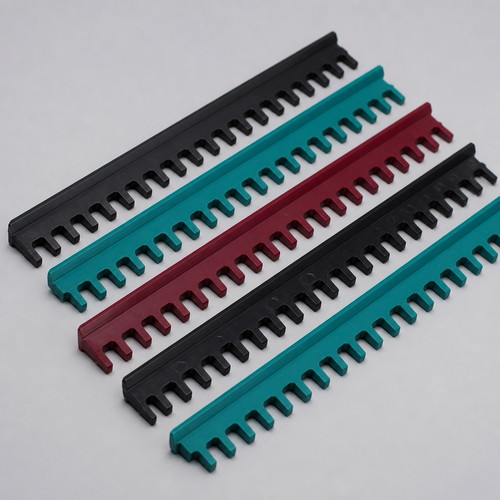
Custom parting combs from P&M are precision injection-molded guide components for textile, wire, and fiber lines. This guide covers parting-line design, resin selection, cavitation, tolerances, and the checks that keep parting combs custom dimensionally stable in high-cycle production.
Send Inquiry
Product Description
Parting combs are the quiet workhorses of any line that has to split, align, or guide a dense bundle of strands, filaments, or wires without crushing them. When a standard catalog part cannot match your pitch, throat geometry, or mounting footprint, the answer is a custom tool built around your drawing. As an injection-molding manufacturer, P&M develops parting combs custom to the exact tooth count, spacing, and profile your machine needs, then holds those dimensions across the entire production life of the mold.
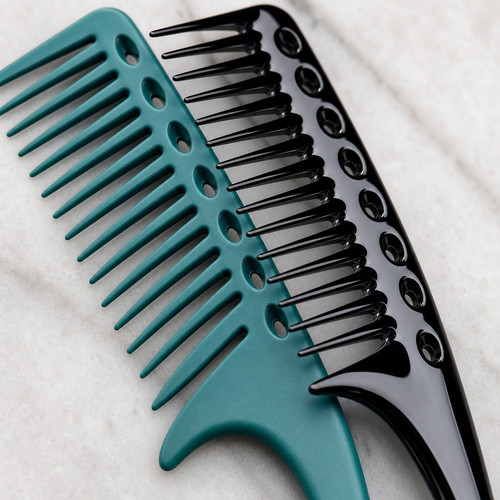
A parting comb looks simple: a row of teeth, slots, or fingers separated by precisely controlled gaps. In practice, every gap is a functional dimension. If pitch drifts by a few hundredths of a millimeter, downstream tensioning equipment starts to mis-feed. If a tooth root is too sharp, filaments abrade and break. If the resin creeps under sustained load, the comb loses alignment within weeks.
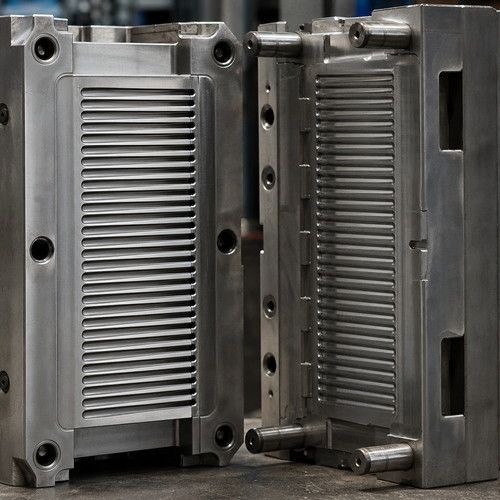
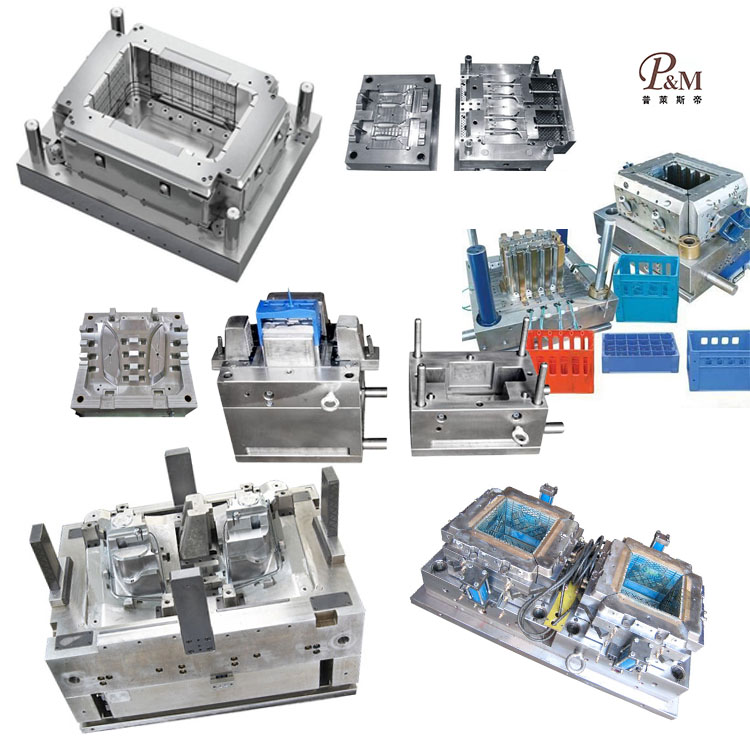
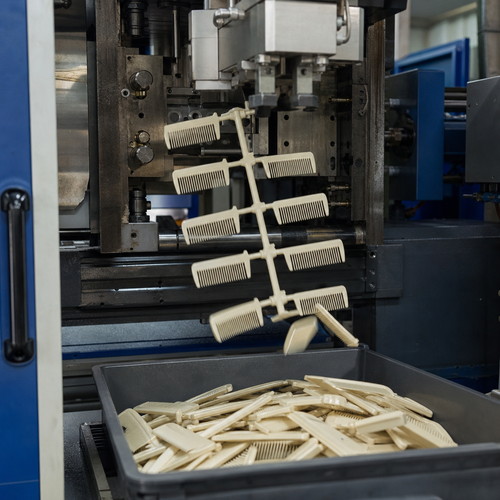
P&M approaches every project the same way: we start with the strand population, line speed, operating temperature, and mounting interface. Our tooling engineers then define the parting line, gate position, cooling layout, and ejection strategy that will produce parting combs custom with repeatable geometry at sustainable cycle times. Prototype, bridge, and hardened multi-cavity production molds are all available from one partner, so the part you validate is the part you receive in volume.
Because the comb sits between machine and material, it is also a consumable. Designing it as a custom molded part lets you tune wear life deliberately: choose a filled engineering resin for abrasion resistance, add ribs where the mounting ears carry load, and thicken tooth roots only where fatigue occurs. That freedom is what separates a durable custom parting comb from a generic spare.
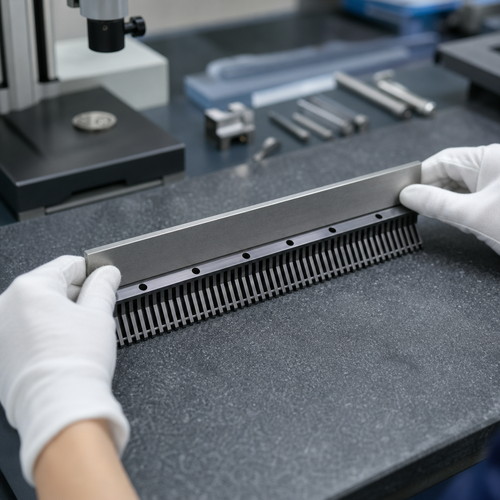
P&M Parting Combs Custom Molding Introduction
A parting comb performs three jobs at once: it establishes pitch, it maintains separation without tension spikes, and it provides a repeatable reference plane for everything downstream. Whether the comb sits in a textile creel, a wire-drawing line, or a packaging unwind station, it must do that work at every cycle, at every shift, for the life of the tool.
### Why off-the-shelf combs usually fall short
Standard combs are designed around the most common pitch and tooth counts on the market, which means they almost always compromise somewhere. Common failure modes reported by our customers include:
- Pitch mismatch. The catalog comb has 40 teeth at 2.54 mm; the machine needs 44 at 2.31 mm.
- Throat geometry. The profile is optimized for coarse yarn and destroys fine denier filament.
- Mounting interface. The bolt pattern or rail width does not match the existing bracket, so the buyer ends up fabricating adapters.
- Material mismatch. An unfilled commodity resin works at ambient temperature but softens and loses pitch control near a heated godet or oven exit.
- Availability. A discontinued spare forces an emergency tooling project at the worst possible time.
### What P&M needs to quote a custom parting comb
Tooling quotes move quickly when the inputs are complete. For custom parting combs, we ask for the following:
- A 2D drawing or 3D model of the comb, including tooth profile, pitch, throat radius, and overall envelope.
- The strand or wire population: count, diameter range, material, and surface finish.
- Line conditions: running speed, ambient or process temperature, humidity, and any chemical exposure such as oils, sizes, or lubricants.
- The mounting interface: bolt pattern, rail width, locating features, and the direction of applied pull.
- Annual volume, target cycle time, and whether a validated pilot run is required before full production.
If only a sample or a worn part exists, our engineers reverse-engineer the geometry, produce a CAD model for approval, and proceed with a single-cavity prototype mold. That path keeps the development budget predictable while still delivering a production-intent part.
### Parting-line and gate design
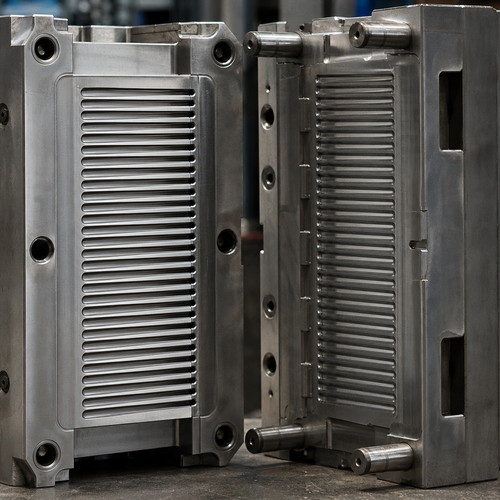
The parting line is where tooling quality is won or lost on a comb. Because the teeth are thin and closely spaced, the parting line must sit on a plane that lets the cavity and core halves close without trapping flash across the slots. Where geometric necessity pushes the parting line across a functional face, we use stepped parting surfaces, shut-off lands, and relieved non-functional zones so that flash forms somewhere harmless.
Gate location matters just as much. A single side gate that fills a long comb end to end tends to leave the last-filled teeth with weld lines and weak roots. On multi-tooth parts we favor a balanced runner with multiple gates, or a hot-tip configuration that fills the tooth array from a central spine. Simulation-driven fill analysis is standard on any new custom parting comb so we can see air traps, weld lines, and pressure loss before steel is cut.
### Resin selection for durability
Material choice determines whether a parting comb lasts one season or five years. The table below summarizes the options we mold most often.
| Resin | Best for | Key strengths | Watch-outs | |---|---|---|---| | Glass-filled PA66 | Abrasive filaments, high-cycle lines | Stiffness, wear resistance, thermal stability | Must be dried correctly; anisotropic shrinkage | | POM (acetal) | Low-friction sliding contact | Natural lubricity, fatigue resistance | Limited bond strength for inserts | | PBT with 30% GF | Hot, chemically exposed lines | Dimensional stability, low moisture uptake | Higher tool wear on hardened steel | | PA12 / PA11 | Wet or humid environments | Low moisture absorption, toughness | Higher resin cost | | TPU / TPE | Delicate filaments needing cushioning | Compliance, grip, no abrasion | Lower stiffness requires ribbing |
### Tolerances, cavitation, and repeatability
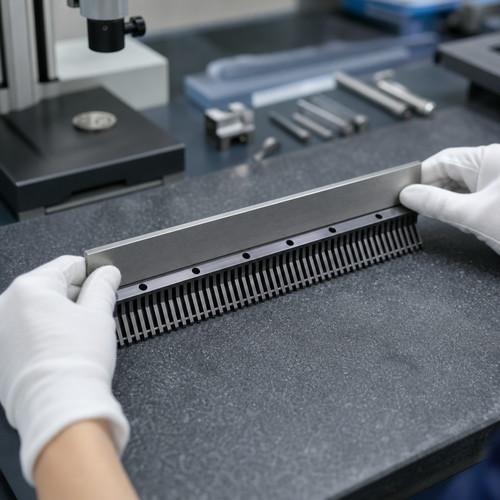
Pitch tolerance on a parting comb is typically held to ±0.05 mm, with critical throat dimensions tighter where the customer's process demands it. Tooth-to-tooth pitch is usually the controlling feature rather than overall length, because accumulated pitch error is what causes mis-feed. Cavitation is decided by volume and geometry: 4, 8, and 16-cavity layouts are common, and any multi-cavity tool ships with valve-gate balancing or a family-layout review so that every cavity produces an interchangeable parting comb.
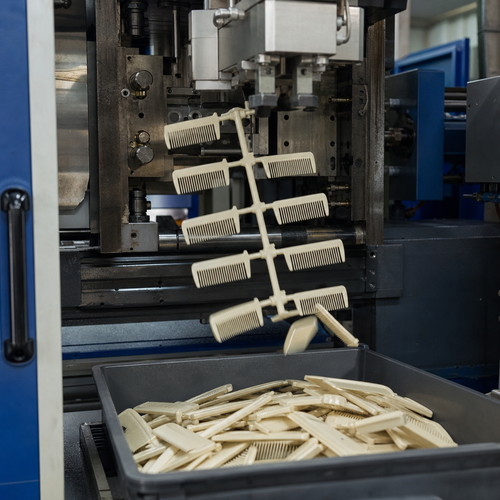
P&M Parting Combs Custom Molding(Specification)
|
Mould Name |
Parting Combs Custom Molding |
|
We promise |
All customer-centric, never for short-term profit, and sell long-term benefits |
|
We produce |
Mold, prototype, injection molding, product assembly, surface printing, spraying the surface integration |
|
Pls provide |
2D, 3D, samples, or the size of the multi-angle pictures |
|
Mould Time |
About 25 working days |
|
Product time |
7-15 Days |
|
Moud precision |
±0.1mm |
|
Mould life |
50-100 million shots |
|
Producing Process |
Audit drawings - mold flow analysis - design validation - Custom Materials - mold processing - core processing - electrode machining - Runner system processing - parts processing and procurement - machining acceptance - cavity surface treatment process - complex mode Die - The entire mold surface coating - Mounting plate - mold sample - sample test - sending samples |
|
Mould cavity |
One cavity, multi-cavity or same different products be made together |
|
Mould material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Runner system |
Hot runner and cold runner |
|
Base material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Finish |
Pitting the word, mirror finish, matte surface, striae |
|
Standard |
HASCO, DME or dependent upon |
|
Main thechnology |
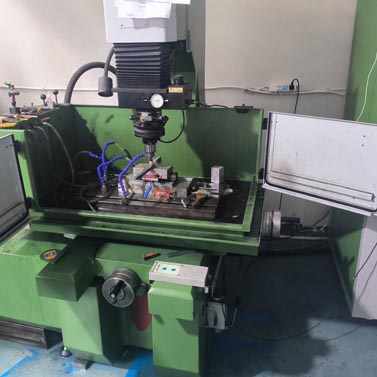
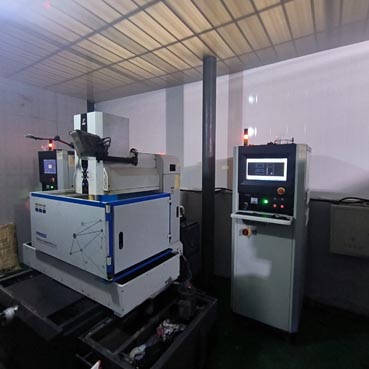
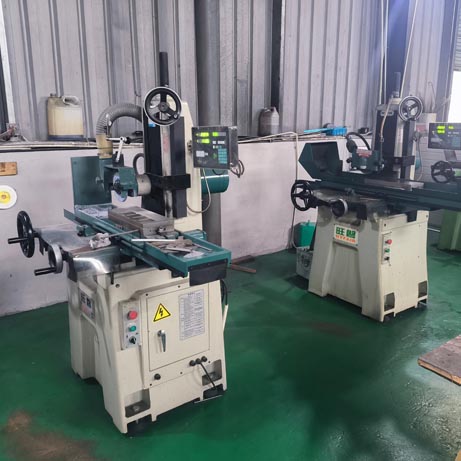
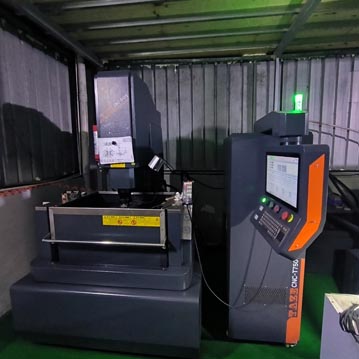
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes, surface Finish, etc. |
|
Software |
CAD,PRO-E,UG Design Time: 1-3 days (normal circumstances) |
|
Product material |
Food grade plastic raw materials |
|
Origin |
Made in China |
P&M Parting Combs Custom Feature And Application
- Line conditions: running speed, ambient or process temperature, humidity, and any chemical exposure such as oils, sizes, or lubricants.
- The mounting interface: bolt pattern, rail width, locating features, and the direction of applied pull.
- Annual volume, target cycle time, and whether a validated pilot run is required before full production.
If only a sample or a worn part exists, our engineers reverse-engineer the geometry, produce a CAD model for approval, and proceed with a single-cavity prototype mold. That path keeps the development budget predictable while still delivering a production-intent part.
### Parting-line and gate design
The parting line is where tooling quality is won or lost on a comb. Because the teeth are thin and closely spaced, the parting line must sit on a plane that lets the cavity and core halves close without trapping flash across the slots. Where geometric necessity pushes the parting line across a functional face, we use stepped parting surfaces, shut-off lands, and relieved non-functional zones so that flash forms somewhere harmless.
Gate location matters just as much. A single side gate that fills a long comb end to end tends to leave the last-filled teeth with weld lines and weak roots. On multi-tooth parts we favor a balanced runner with multiple gates, or a hot-tip configuration that fills the tooth array from a central spine. Simulation-driven fill analysis is standard on any new custom parting comb so we can see air traps, weld lines, and pressure loss before steel is cut.
### Resin selection for durability
Material choice determines whether a parting comb lasts one season or five years. The table below summarizes the options we mold most often.
| Resin | Best for | Key strengths | Watch-outs | |---|---|---|---| | Glass-filled PA66 | Abrasive filaments, high-cycle lines | Stiffness, wear resistance, thermal stability | Must be dried correctly; anisotropic shrinkage | | POM (acetal) | Low-friction sliding contact | Natural lubricity, fatigue resistance | Limited bond strength for inserts | | PBT with 30% GF | Hot, chemically exposed lines | Dimensional stability, low moisture uptake | Higher tool wear on hardened steel | | PA12 / PA11 | Wet or humid environments | Low moisture absorption, toughness | Higher resin cost | | TPU / TPE | Delicate filaments needing cushioning | Compliance, grip, no abrasion | Lower stiffness requires ribbing |
### Tolerances, cavitation, and repeatability
Pitch tolerance on a parting comb is typically held to ±0.05 mm, with critical throat dimensions tighter where the customer's process demands it. Tooth-to-tooth pitch is usually the controlling feature rather than overall length, because accumulated pitch error is what causes mis-feed. Cavitation is decided by volume and geometry: 4, 8, and 16-cavity layouts are common, and any multi-cavity tool ships with valve-gate balancing or a family-layout review so that every cavity produces an interchangeable parting comb.
Customization Process
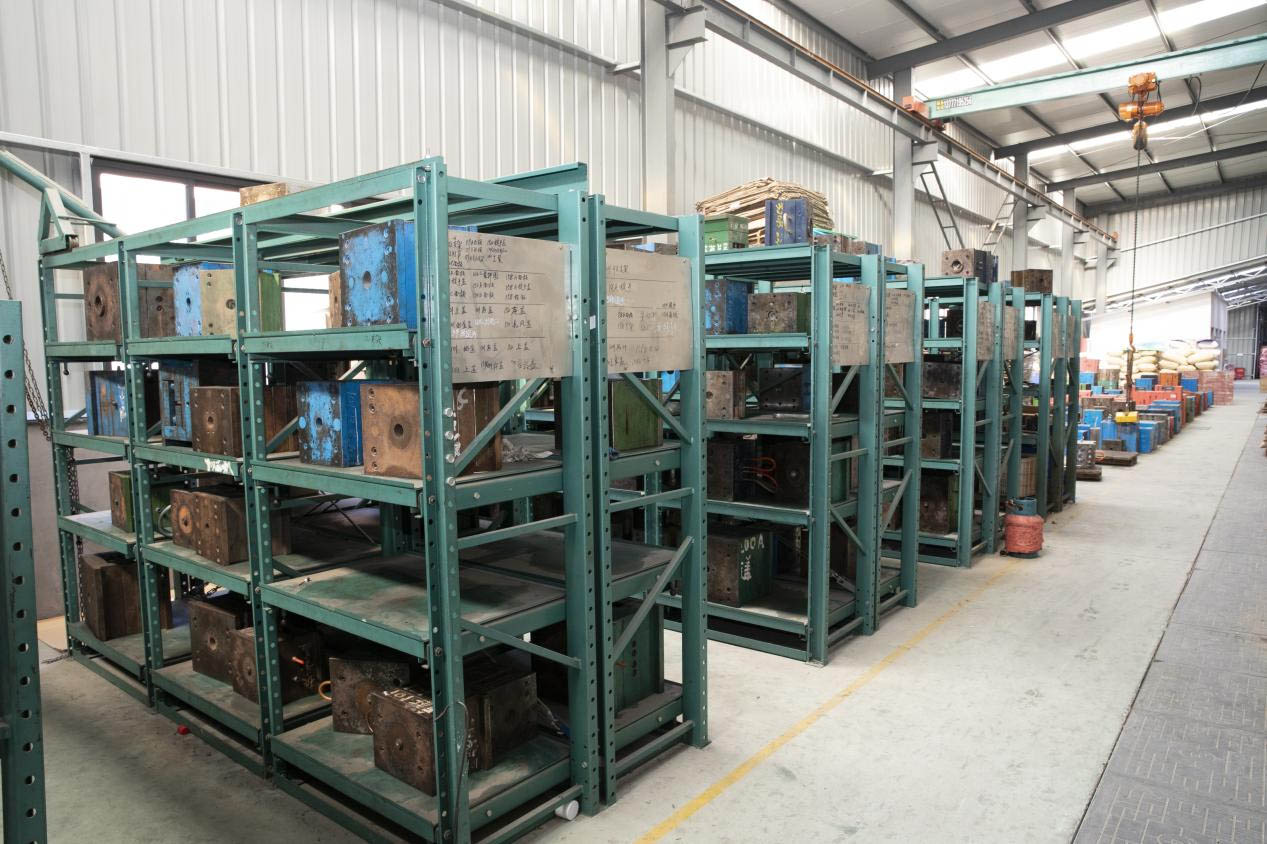
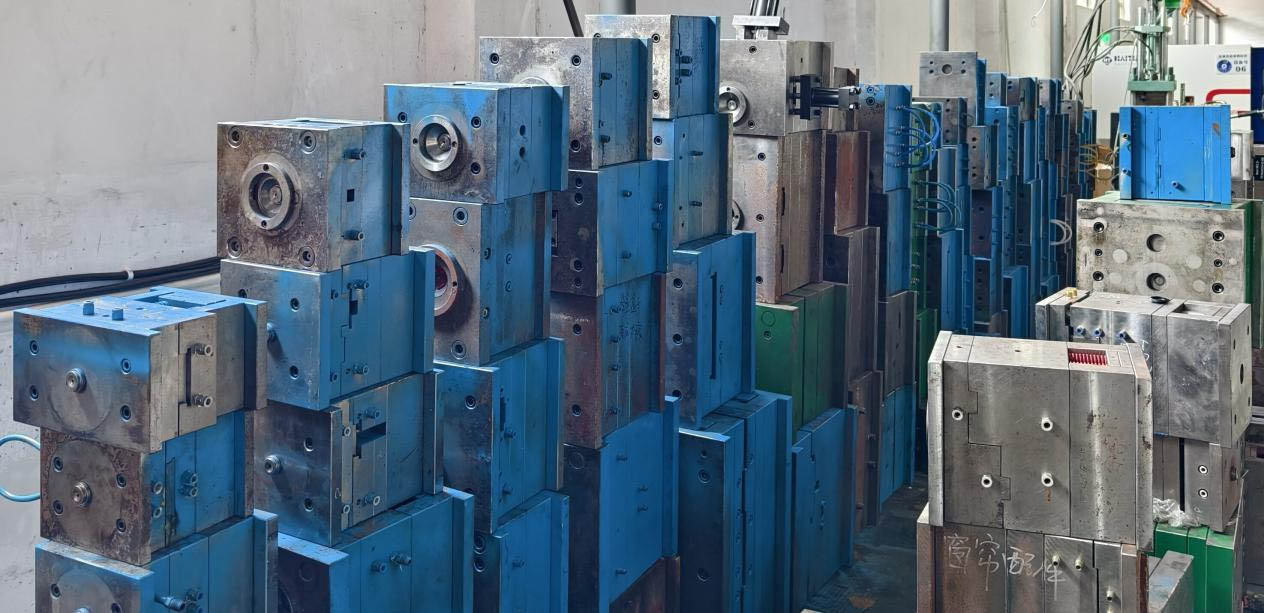
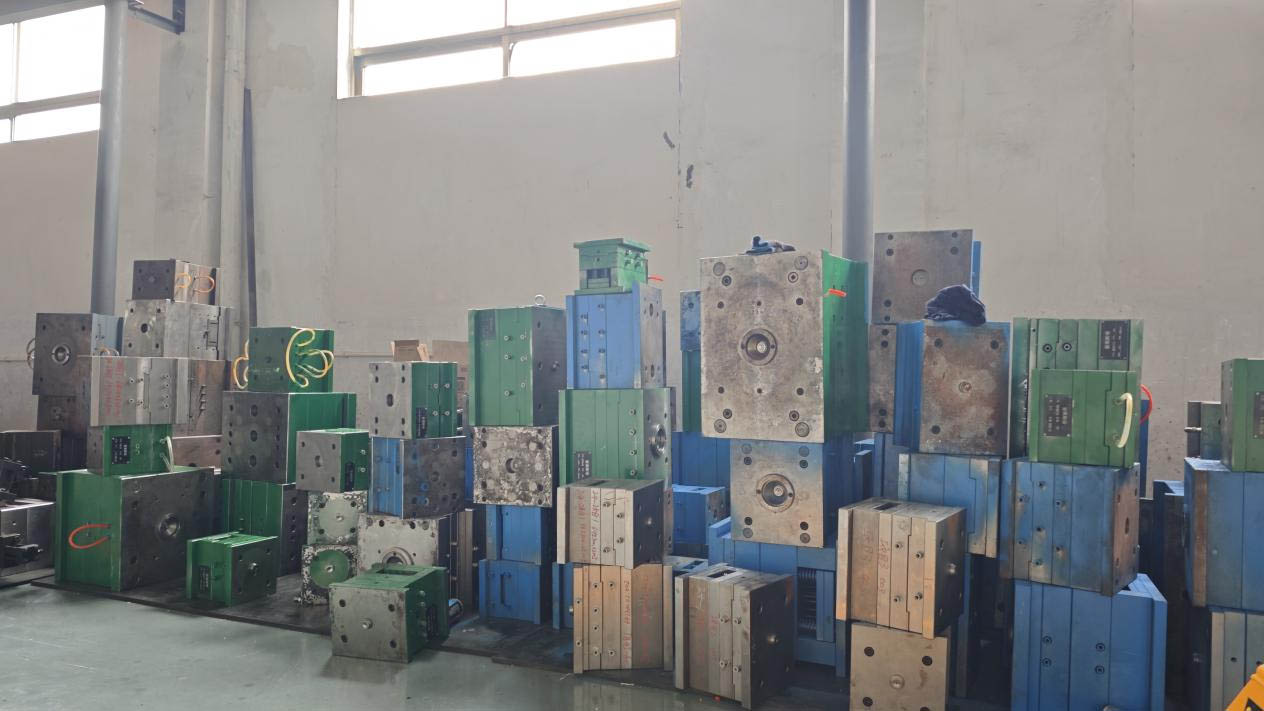
Factory&About US
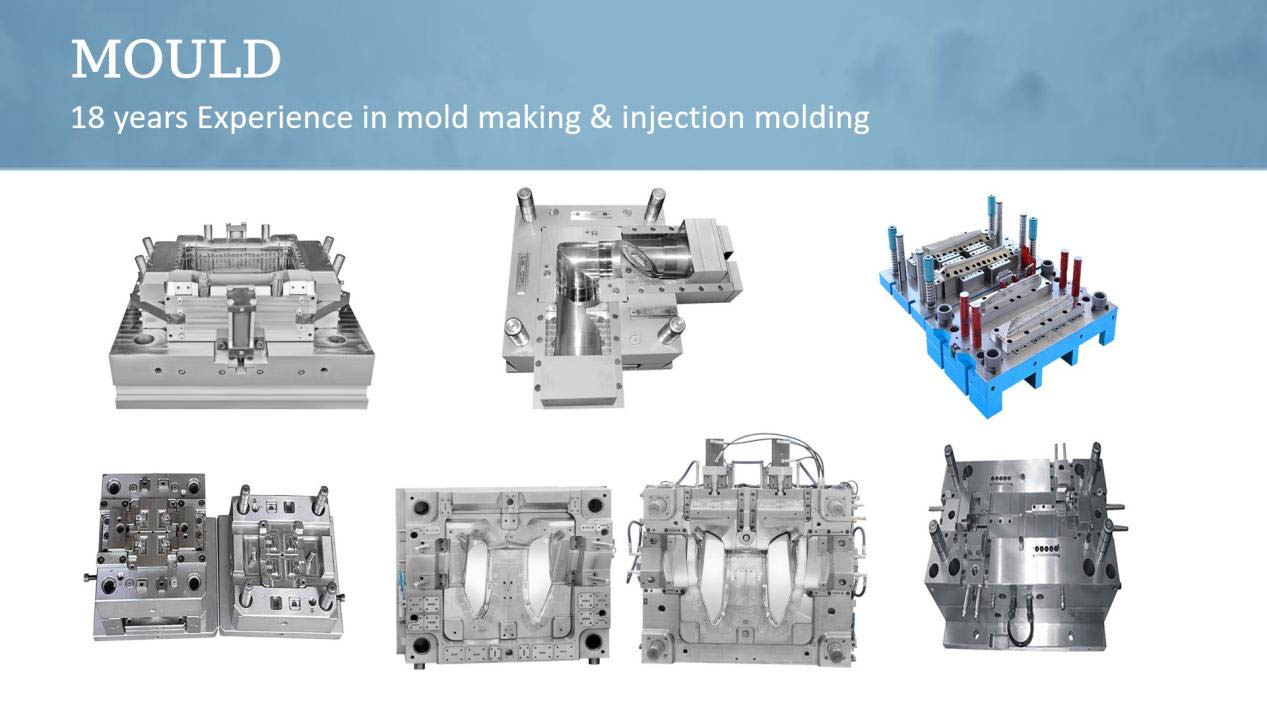
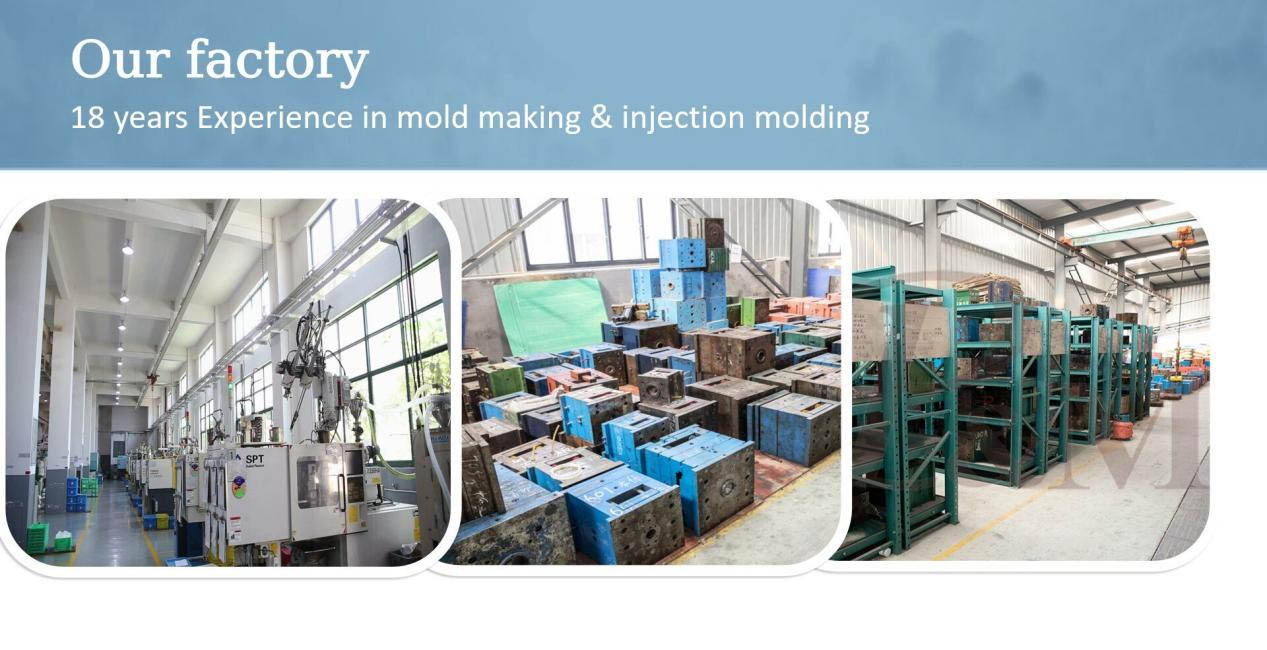
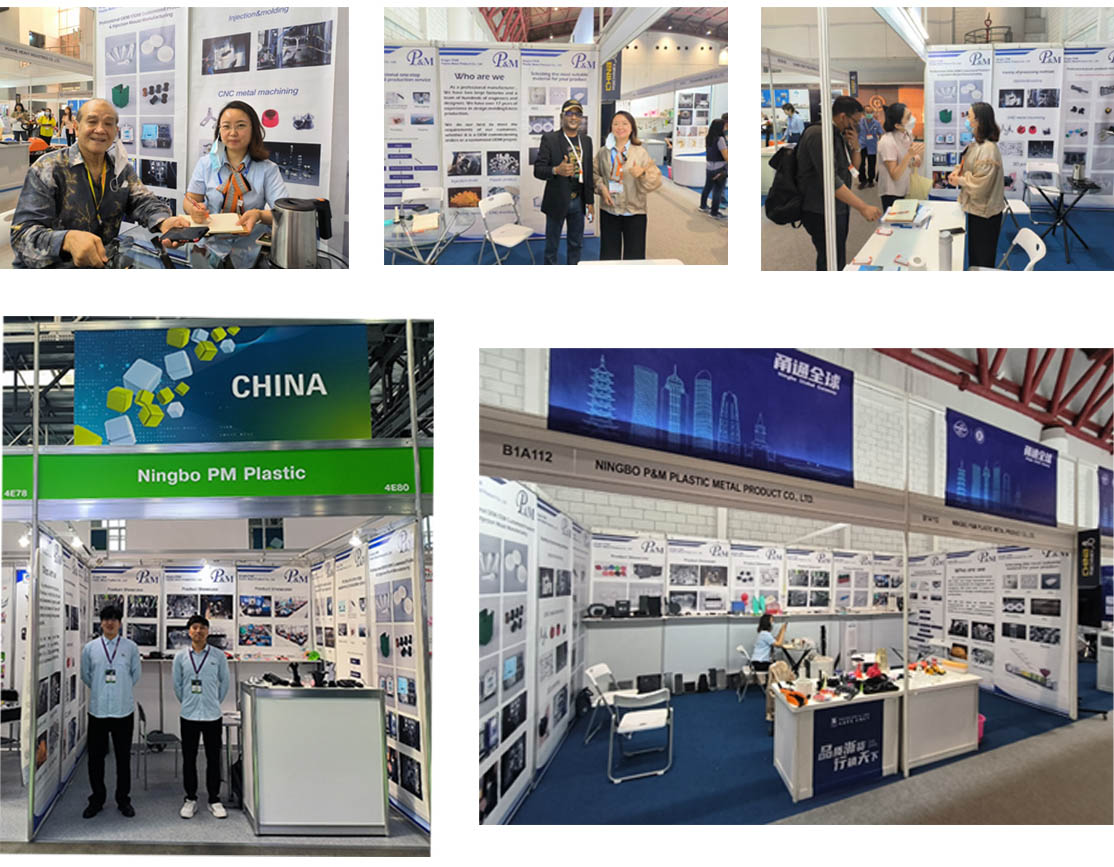
NingBo Plastic Metal Product Co.,Ltd (P&M) is located in Yuyao, the so-called Mould City, Plastic Kingdom, in the southern tip of Hangzhou Bay Bridge,north of Shanghai, the east of Ningbo Port,tight double line of State Road 329 on land, sea and air trafic into a network to facilitate transport.
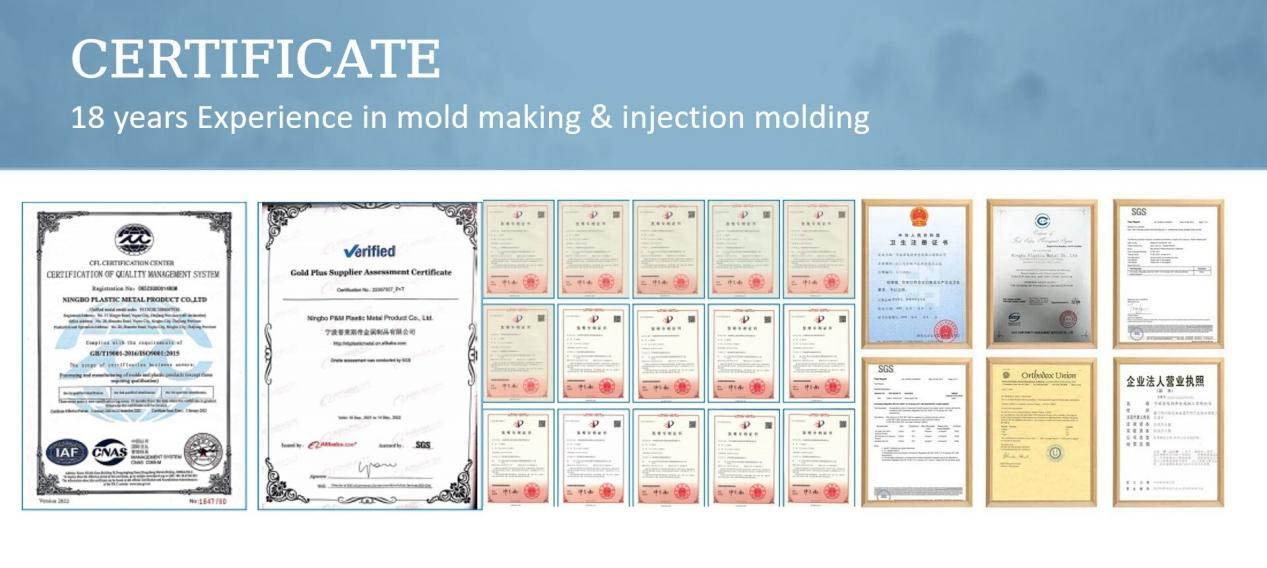
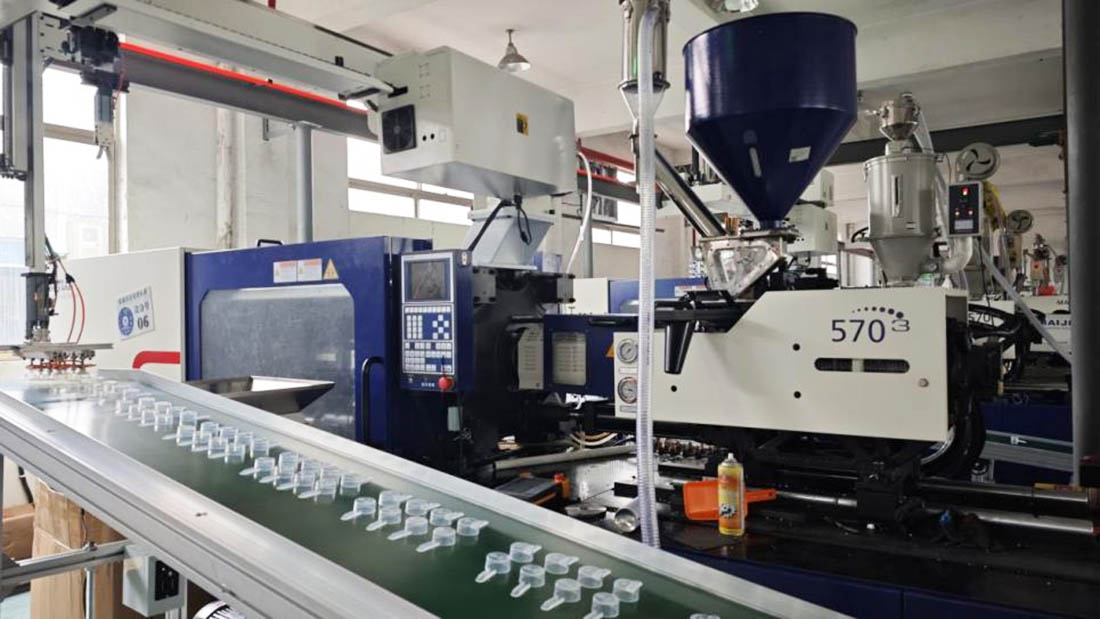
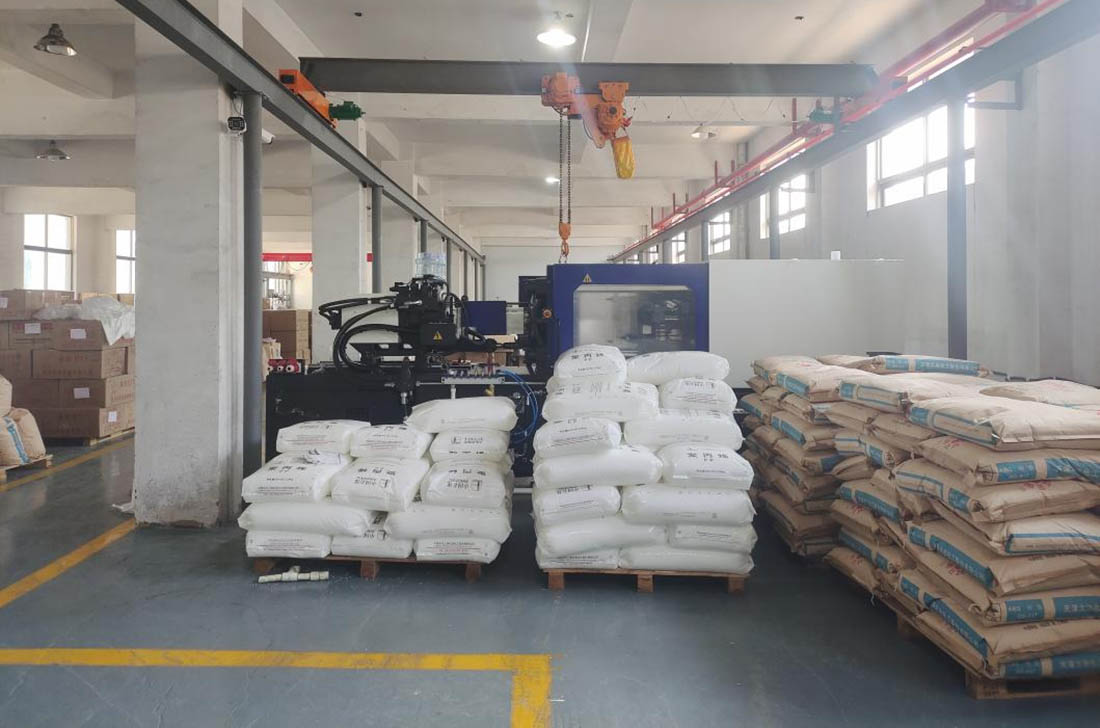
By the abundant technical strength,scientific management methods and good after-sales service, product deeply trusted and welcomed by customers from all over the world. P&M holds improved system of development and production, to achieve mold design, plastic products manufacturing and automatic production. Our main products is design and manufacturing of plastic mold, plastic product, metal product. 90% products of our enterprise are exported to America, Europe, Germany, Japan, Australia, etc. For many years, the company has been committed to the research of raw materials. The company has its own trademark and dozens of patents, providing more convenient technical support for mold making and product production. P&M started domestic business from 2008,named Shundi Mould Factory. And opened the international market from 2014. We always adhere to the principles of quality first and time first. While providing customers with the highest quality products, try to maximize the production efficiency and shorten production time. We are proud to tell every customer that our company has not lost any customer since its establishment.If there is a problem with the product, we will seek a solution actively and take responsibility to the end.
P&M adheres to market-oriented to the quanlity of life and focus on quality service and continuous development of new products,determined to establish a better corporate image,and our friends at home and abroad to carry a wide range of business exchanges and cooperation, create brilliant.
Packing
Packaging according to your needs
1. By air ,it takes 3-7 days for delivery.
The goods can be shipped by DHL , Fedex , UPS .
2. By sea ,the delivery time is based on your port.
To South East Asian Countries takes about 5-12 days.
To Middle east countries takes about 18-25 days.
To European countries takes about 20-28 days.
To American countries takes about 28-35 days.
To Australia takes about 10-15 days.
To African countries takes about 30-35 days.
P&M Bike parts, centered around children, balances safety, health, and fun, aiming to add a bright color to children's beautiful childhood. We look forward to working together with you to serve our children.
The path of a child's growth is paved with bricks and tiles.
FAQ
1.Who are we?
We are based in Zhejiang, China, start from 2014,sell to North America(30.00%),Southern Europe(10.00%),Northern Europe(10.00%),Central America(10.00%),Western Europe(10.00%),Mid East(10.00%),Eastern Europe(10.00%),South America(10.00%). There are total about 51-100 people in our office.
2.How can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.What can you buy from us?
Mould, Plastic Product, Metal Product, Dental Product, CNC machining.
4.Why should you buy from us not from other suppliers?
We main do all kinds of 3d design, 3d printing and plastic metal molds tooling and products. We have our own engineer and factory. One-stop supply: 3d design - 3d printing - mold making - plastic injection.
5.What services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency: USD, EUR;
Accepted Payment Type: T/T,L/C,PayPal,Western Union,Escrow;
Language Spoken:English,Chinese,Spanish,French,Russian.
6.What are the characteristics of your service?
1. Your inquiry related to our products or prices will be replied within 24 hours.
2. Well-trained and experienced staffs to answer all your enquiries in fluent English.
3. Offering the support to solve the problem in the application or selling period.
4. Competitive prices based on same quality.
5. Guarantee samples quality same as mass production quality.
Hot Tags: Parting Combs Custom, China, Manufacturer, Supplier, Factory, Customized, Wholesale, Buy, Quality, Latest Selling, Made in China
Related Category
Send Inquiry
Please feel free to give your inquiry in the form below. We will reply you in 24 hours.