
Home
>
Product > Core Customization Service > Custom Molding > Custom Kitchen Plastic Parts Injection moulding
Product
- Core Customization Service
- Health Care
- Electronic Appliances and Instruments
- Maternal and Child Supplies Molds
- Recreational Sports
- Home Furnishing Art
- Auto Accessories
- Transportation and Warehousing
- Lighting Fixtures
- Construction Equipment
- Packaging Product
- Educational & Laboratories
- Clothing Luggage Accessories
- Care and Cleaning Products
- Agriculture & Forestry
- Mechanical Equipment
- Pet Supplies
- Kitchenware
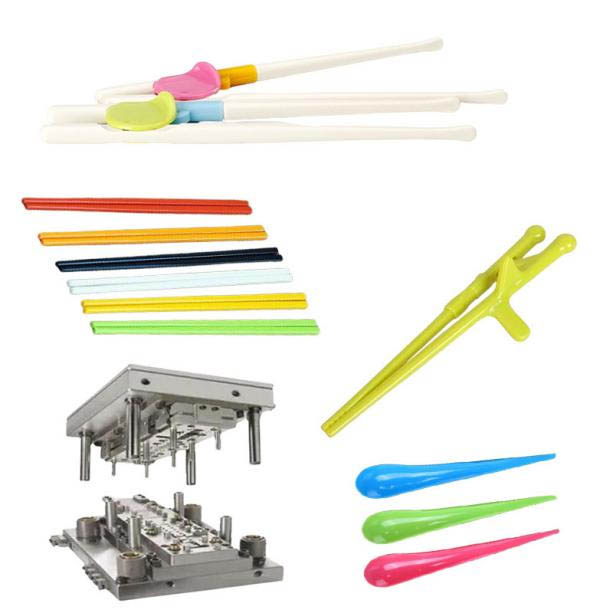
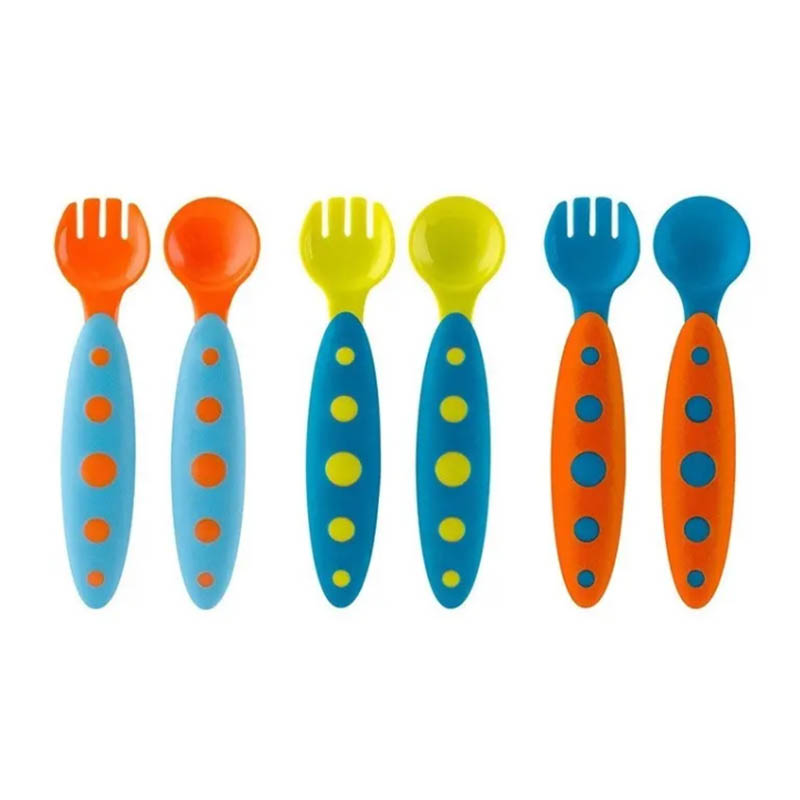
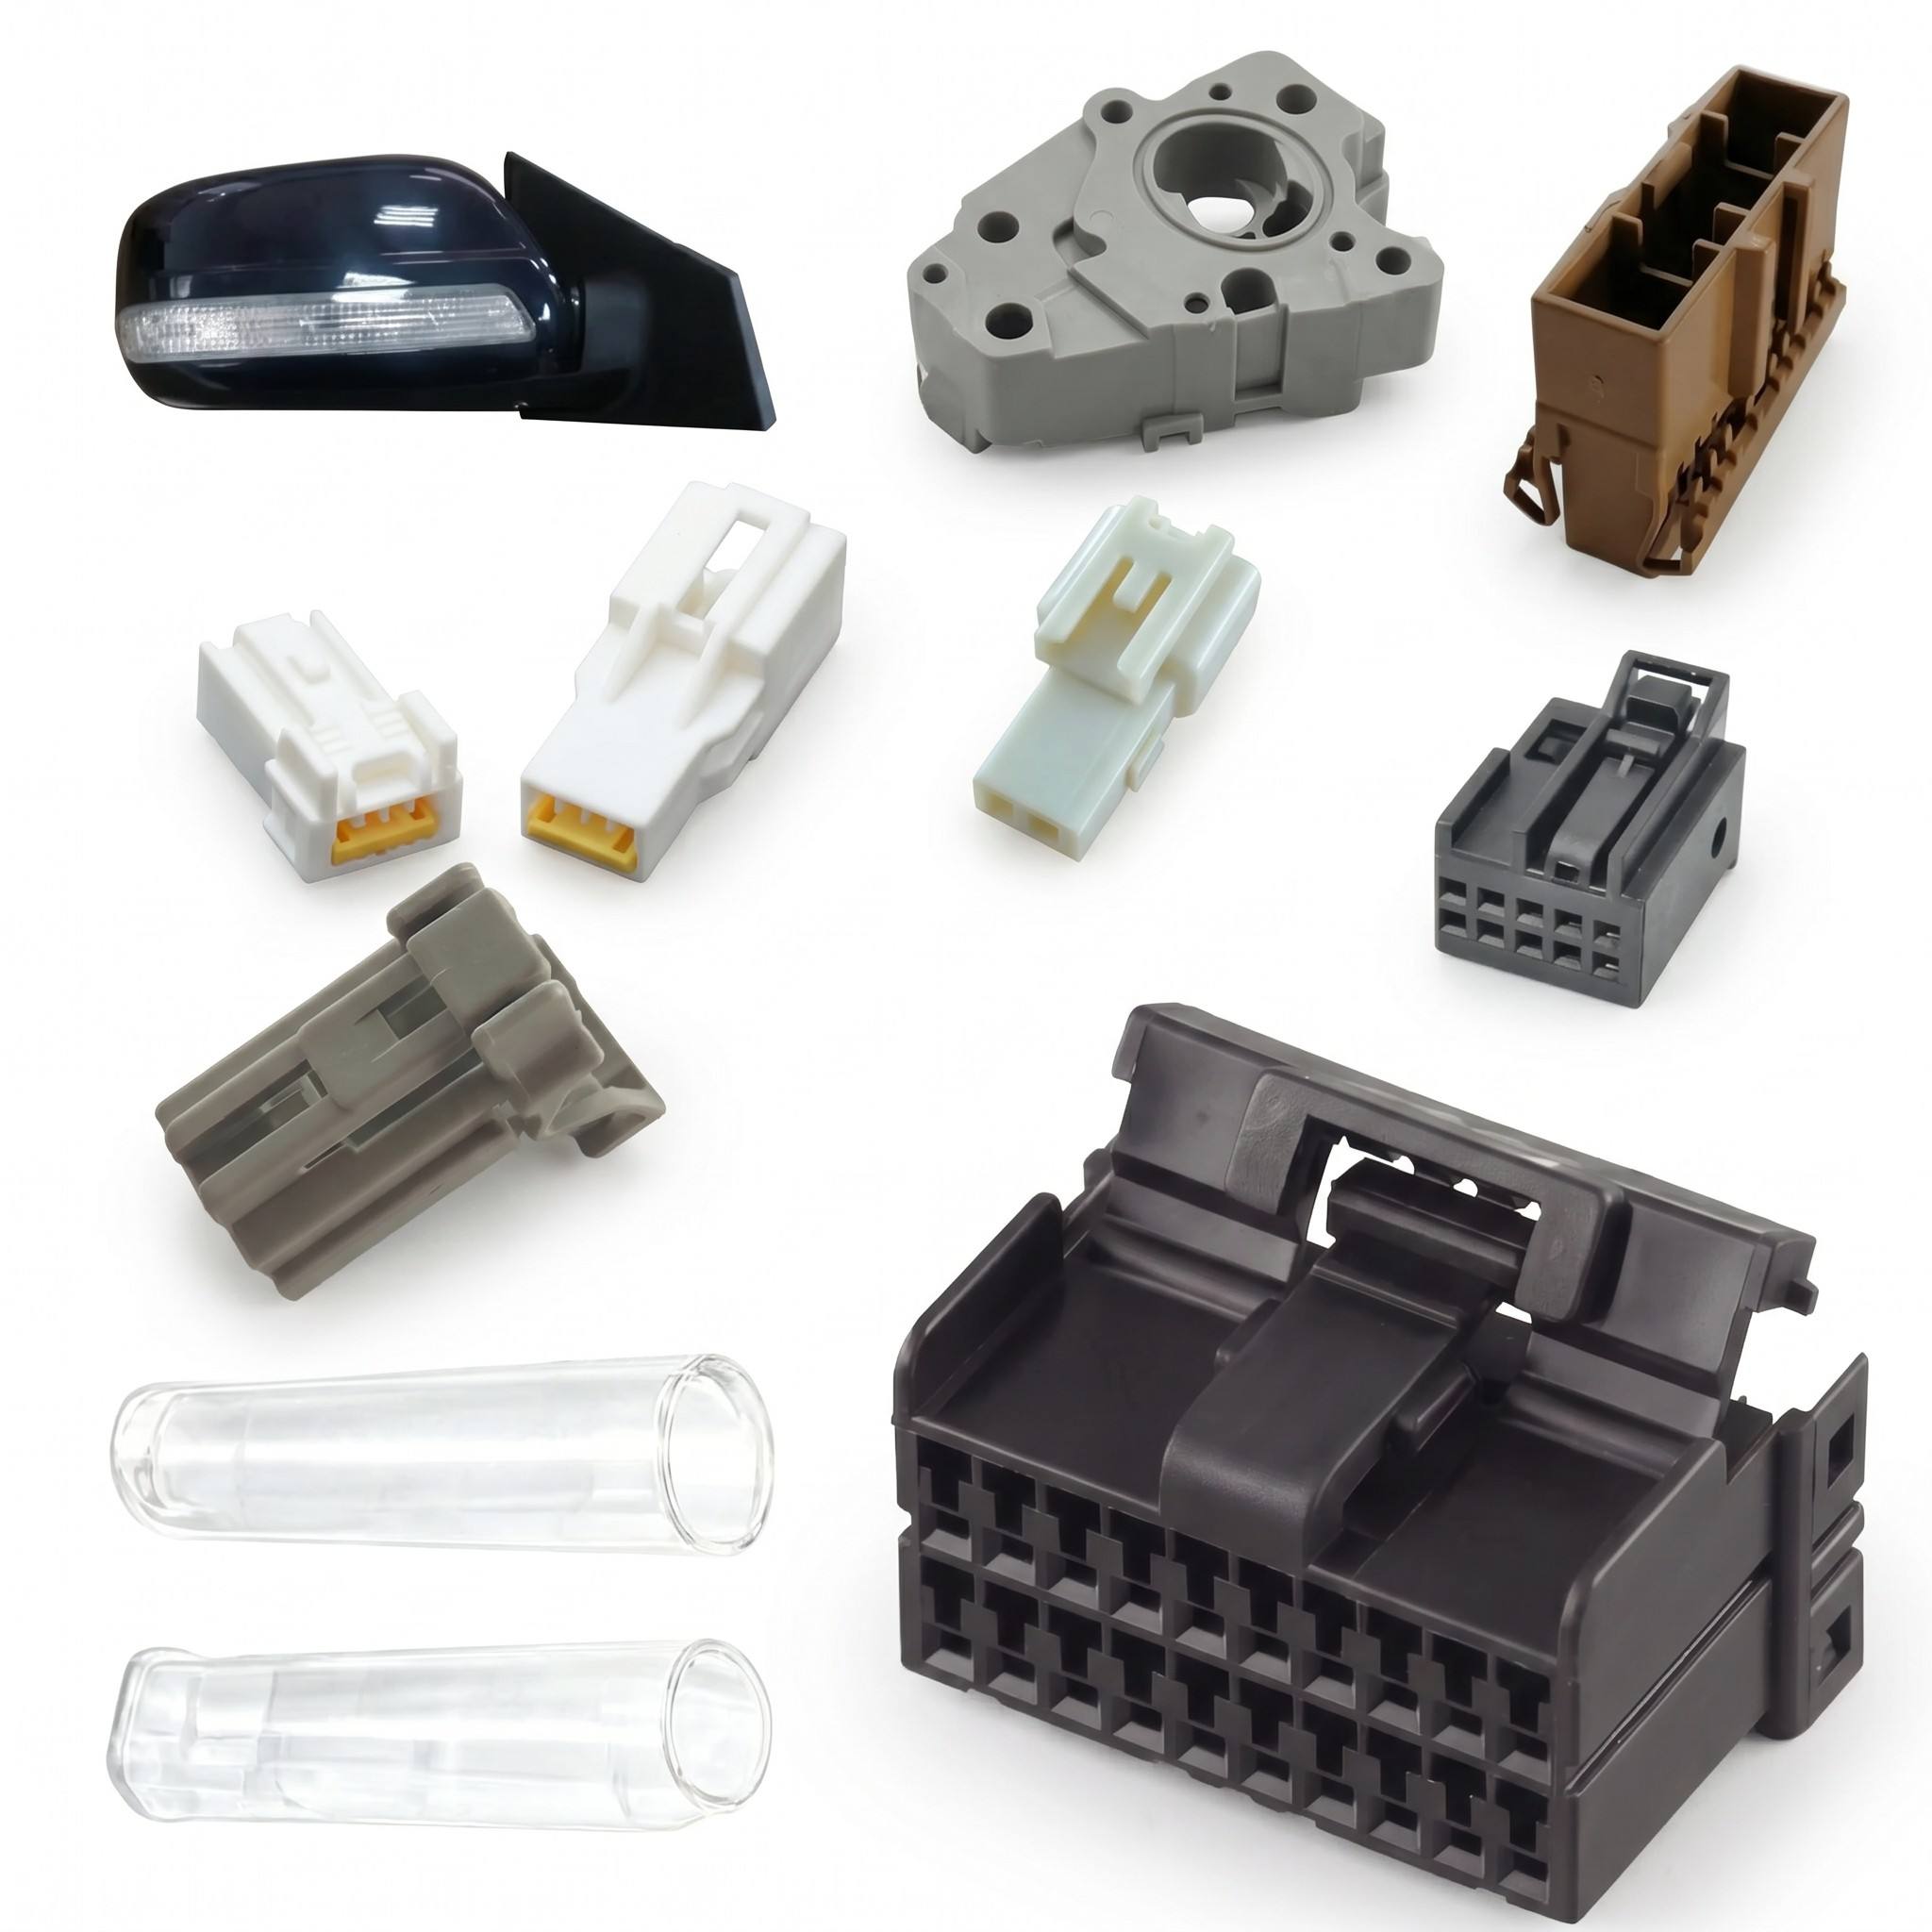
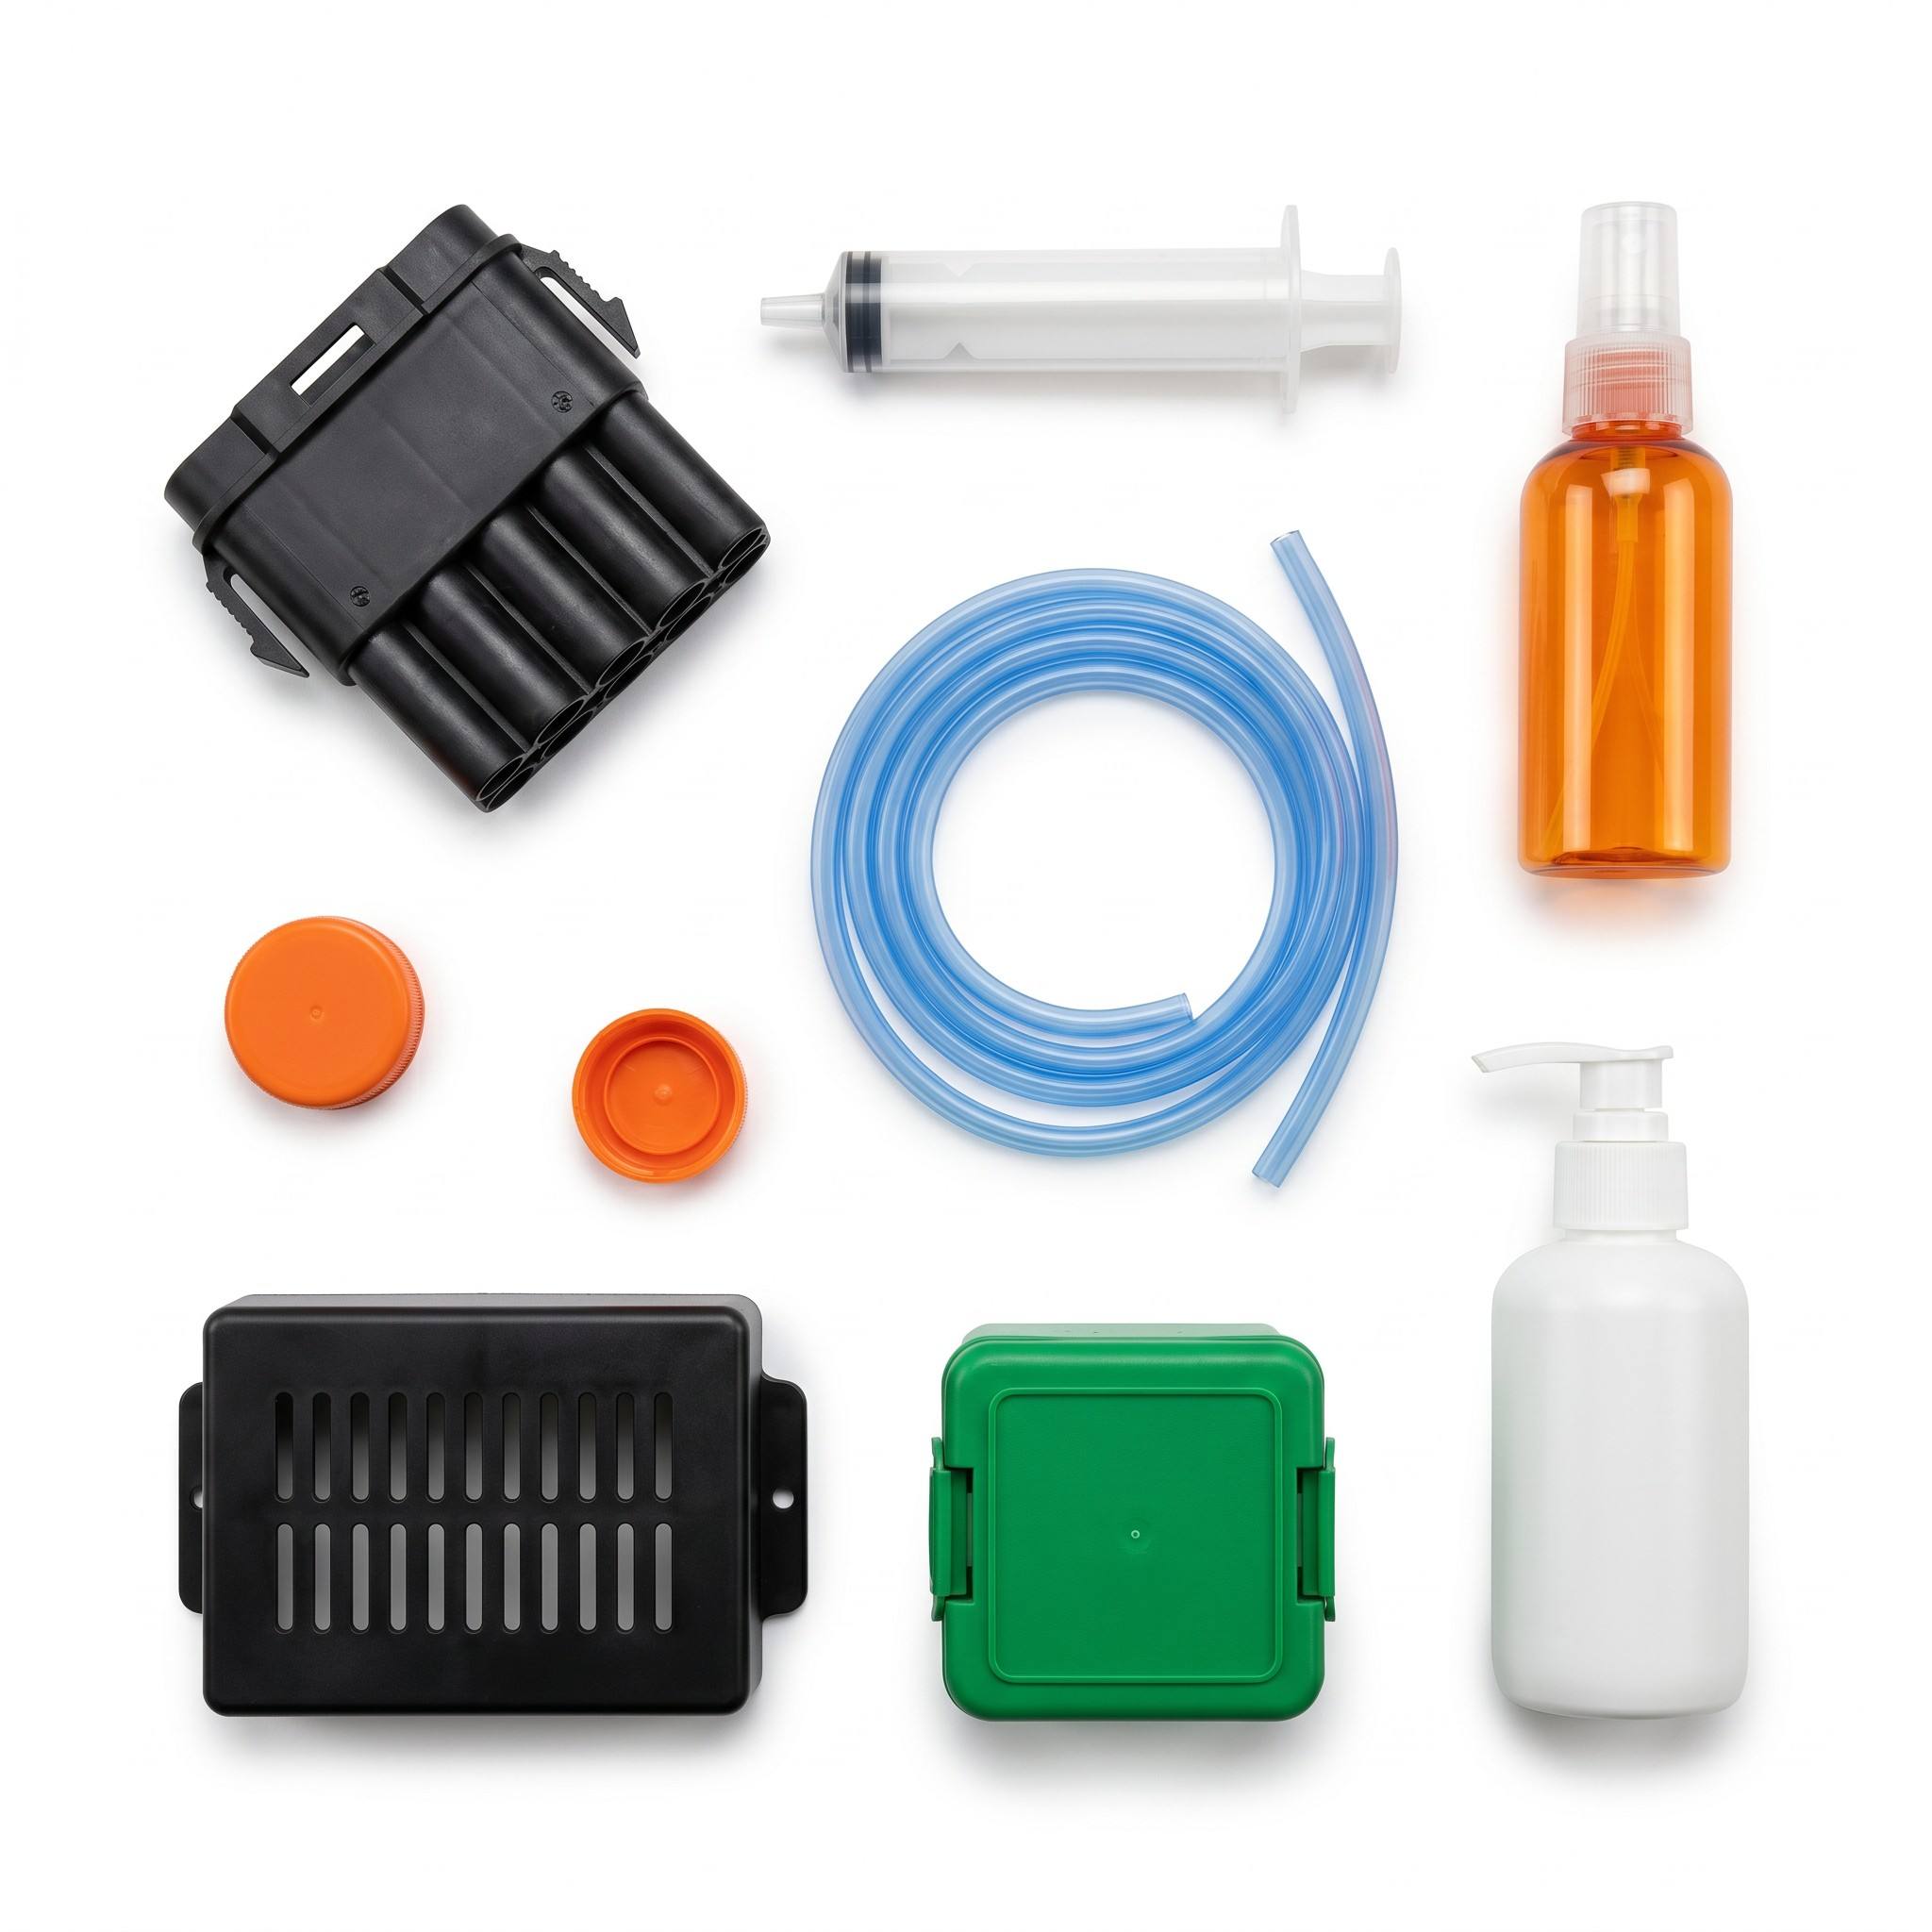
Custom Kitchen Plastic Parts Injection moulding
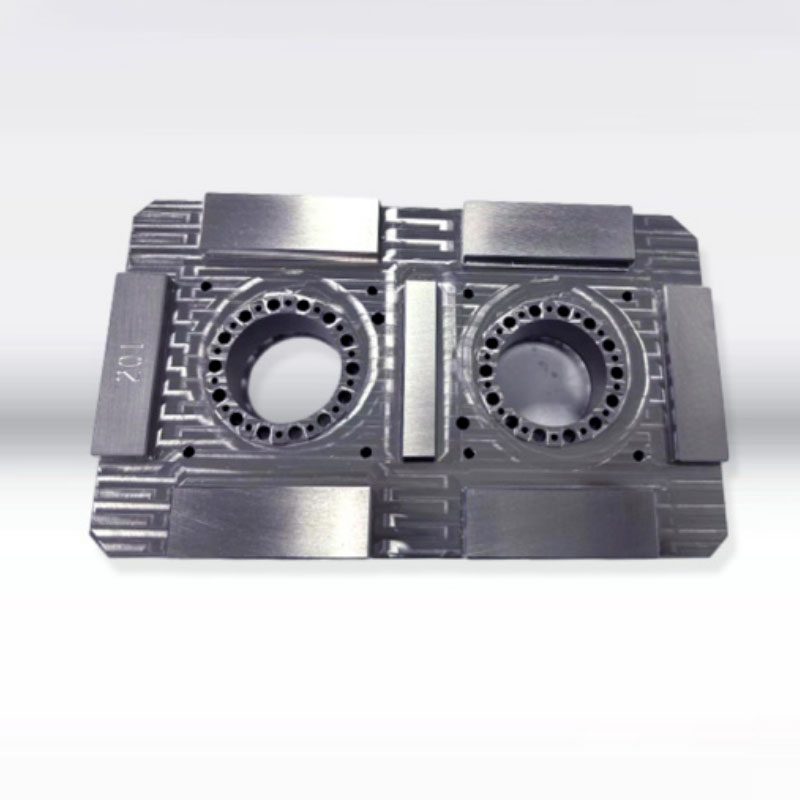
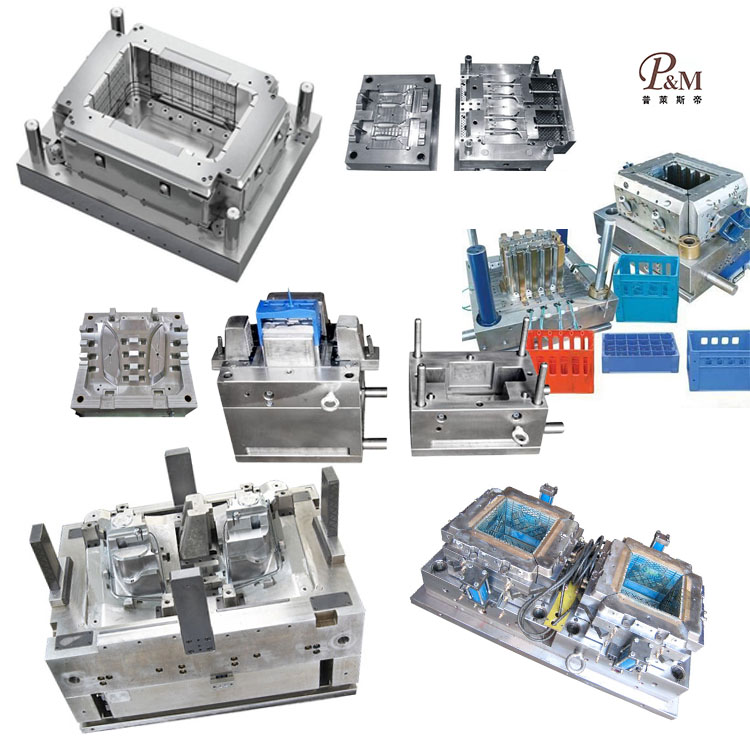
Ningbo (P&M) Plastic Metal Products Co., Ltd. has 18 years of mold manufacturing technology and can customize Custom Kitchen Plastic Parts Injection moulding. We provide professional customized Custom Kitchen Plastic Parts Injection moulding services, and we are a professional Custom Kitchen Plastic Parts Injection moulding manufacturer. We have sufficient experience in selecting product raw materials and mold materials. In the process of customizing Custom Kitchen Plastic Parts Injection moulding, our factory can provide one-stop service. We have design and production capabilities related to Custom Kitchen Plastic Parts Injection moulding, such as: CAD design, mold manufacturing, injection molding, plastic product production, assembly and other technologies.
Send Inquiry
Product Description
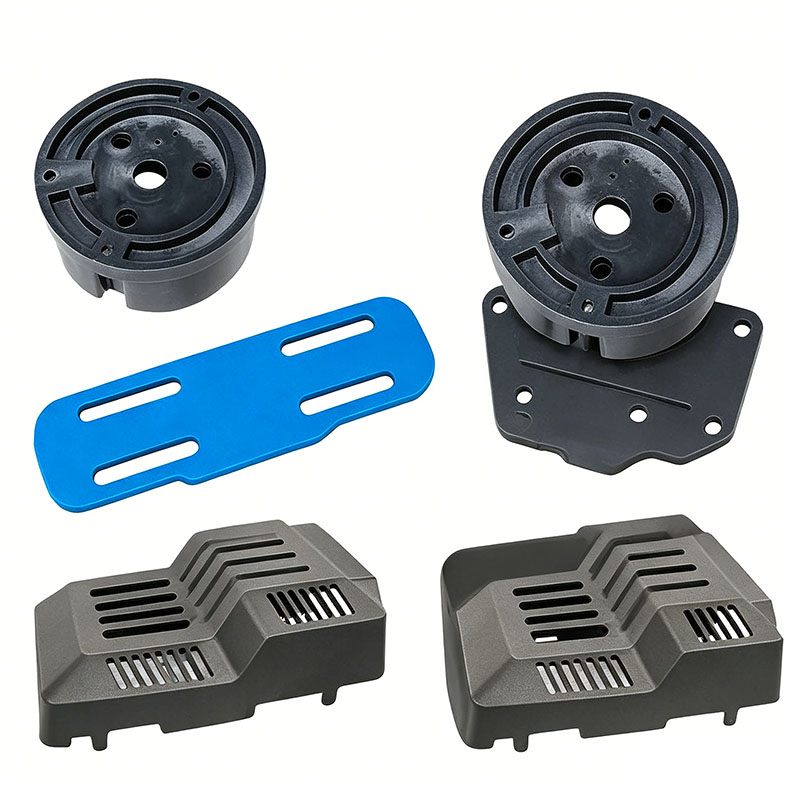
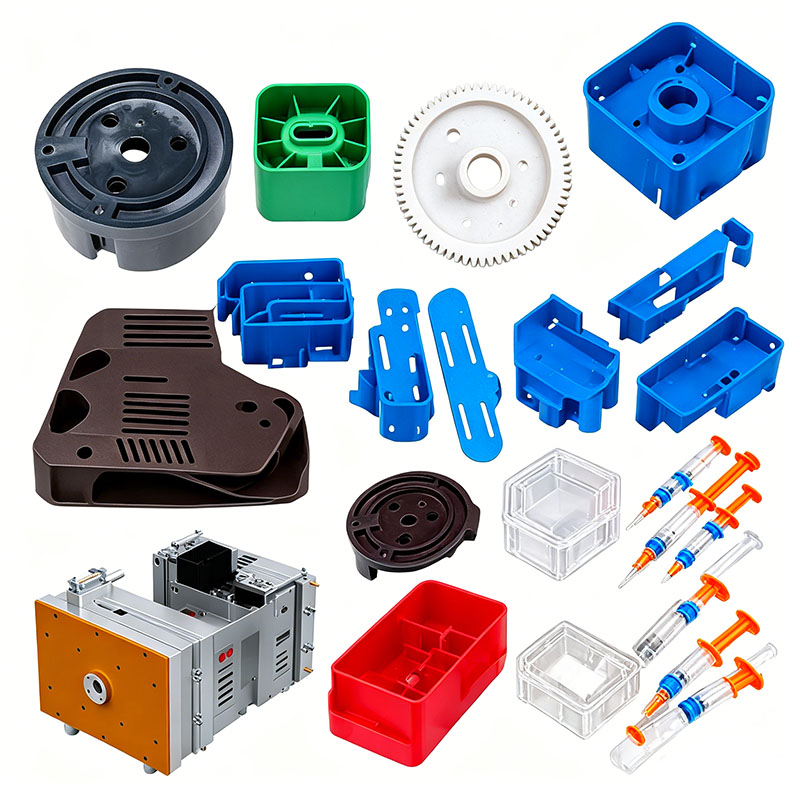
In addition, our company has established cooperative relationships with plastic raw material suppliers, printing manufacturers, etc. to ensure the supply of raw materials and printing quality. Through our rich experience and perfect supply chain, our company can provide customers with high-quality customized Custom Kitchen Plastic Parts Injection moulding products to meet their specific needs. At the same time, we have 10 years of professional foreign trade service experience, understand the foreign trade process, and better serve our customers. For Custom Kitchen Plastic Parts Injection moulding products, we can make corresponding plastic parts, which is mainly done through injection molds.
## Key Injection Molding Parameters (Focusing on PP Food Containers—the Most Common Application)
>
> Principles: **Use medium-to-low injection speeds, implement multi-stage holding pressure, and maintain a stable mold temperature. Avoid excessive shear-induced heating to prevent material degradation and the leaching of substances beyond permissible limits.**
### Reference Parameters for PP
1. Barrel Temperature (from hopper to nozzle): 180 → 190 → 200 → 210°C; Nozzle: 200–215°C
- Avoid prolonged exposure to temperatures above 230°C; extended residence time at high temperatures will cause PP to degrade and develop an unpleasant odor.
2. Mold Temperature: **40–60°C**
>
> Tip: Conduct "boiling water resistance" tests to determine the optimal mold temperature.
- Low mold temperature: Faster molding and shorter cycle times, but results in uneven crystallization and high internal stress, making the product prone to deformation during subsequent hot-water sterilization.
- Higher mold temperature: Promotes uniform crystallization and dimensional stability, improving resistance to hot water; however, it increases cycle times and may cause the part to stick to the mold.
3. Filling:
- Thin-walled containers: Use a slow speed initially, transition to medium speed after passing the gate, and slow down toward the end to prevent air entrapment. Avoid using high-speed injection throughout the entire process.
- Pressure: Injection pressure 60–90 bar (depending on the specific machine).
4. Holding Pressure (Crucial for food containers! Controls sink marks and dimensional accuracy.)
- Multi-stage holding: Use high pressure in the first stage to compensate for shrinkage, followed by lower pressure in the second stage to prevent excessive internal stress and warping.
- Holding duration: Should be based on the "gate freeze-off" point. If the holding time is too long, the container rim may expand outward or deform; if too short, surface sink marks (depressions) may occur.
5. Cooling:
- Ensure cooling water channels are positioned close to the mold cavities and distributed uniformly. Provide sufficient cooling time; a lower part temperature at the time of ejection results in less post-molding deformation.
- PP Crystallization-induced shrinkage continues even after demolding, making **post-mold stabilization (setting)** crucial. For many food containers, a stabilization fixture (jig) is applied after demolding and kept in place until the part cools to room temperature; this prevents warping and ensures the lid fits properly.
6. Back pressure: 5–10 bar. Keep back pressure low to minimize shear-induced heating while ensuring uniform dispersion of colorants. Excessive back pressure raises the melt temperature, which can lead to material degradation and the development of unpleasant odors.
7. Screw speed: Use a low-to-medium speed to avoid overheating caused by excessive shear.
## Specifics for Transparent Tritan Parts
- Melt temperature: 240–270°C; Mold temperature: 60–80°C.
- Avoid excessive shear, as it can cause stress marks. When production stops, purge the barrel (e.g., using PP) to prevent carbon buildup or the formation of black specks.
- Post-molding annealing (holding at 70–80°C) can reduce internal stress and prevent cracking when the product is exposed to hot water.
## IV. Common Defects and Countermeasures (Frequently encountered in kitchenware)
1. **Sink marks, depressions (on outer walls or near ribs of PP containers)**
- Causes: Ribs are too thick; insufficient holding pressure; gate freezes off too early.
- Countermeasures: Reduce rib thickness; enlarge the gate; extend holding pressure duration; increase mold temperature; adjust gate location.
2. **Warping, lids that won't close, or deformation at the opening**
- Causes: Uneven shrinkage; uneven cooling; excessive holding pressure; high demolding temperature.
- Countermeasures: Optimize cooling channels; use a post-mold stabilization fixture; implement multi-stage holding pressure; balance the gating system; optimize structural ribs.
3. **Silver streaks, bubbles**
- Causes: Moisture in the raw material (especially common in transparent resins); trapped air; material degradation.
- Countermeasures: Dry the material; improve venting; lower the melt temperature; reduce residence time in the barrel.
4. **Black specks, black streaks**
- Causes: Carbonization of material in "dead zones" of the hot runner system; residual impurities in the barrel; poor dispersion of masterbatch.
- Note: For food-contact items, black specks are considered a critical defect; such parts must not be shipped.
5. **Visible Weld Lines and Poor Strength**
- Position weld lines away from load-bearing areas; increase mold and melt temperatures; improve venting; adjust gate sequencing.
6. **Unpleasant Odor in Products**
- Caused by substandard raw materials, material degradation due to excessive barrel temperatures, impure regrind, or improper use of mold release agents. ⚠️ **Note:** The use of standard oil-based mold release agents is **strictly prohibited** for kitchenware. Use water-based, food-grade alternatives if necessary, or ideally, polish the mold to eliminate the need for release agents.
7. **Deformation or Leakage After Boiling Water Test**
- Caused by insufficient crystallization or high internal stress. Increase mold temperature, ensure adequate cooling/setting time, or switch to a high-heat-resistant grade of PP.
## V. Production Process Control & Additional Food-Compliance Requirements
1. Machine Segregation: Dedicate specific machines to food-grade production; avoid using the same equipment for industrial-grade or non-food materials. Perform thorough machine purging during material changes and maintain purge records.
2. Environment: Maintain a dust-free workshop to prevent particulate matter from adhering to the inner surfaces of the products.
3. Additives: All lubricants and antioxidants must be food-compliant. Do not incorporate recycled plastics of unknown origin.
4. Post-Processing:
- Gate Removal: Ensure cutting tools are smooth to prevent burrs.
- Printing/Laser Marking: Use food-grade, water-resistant, and detergent-resistant inks; conduct migration testing.
- Overmolded Products: Perform peel tests to ensure the soft-touch material does not detach.
5. Quality Inspection Items: Dimensional fit, visual appearance, boiling water resistance (100°C for 30 minutes), drop testing, migration testing, and odor testing.
## VI. Summary: Implementation Roadmap
Select compliant food-grade raw materials → Ensure thorough drying → Design molds for uniform wall thickness, balanced gating, and sufficient venting; use S136 steel with a mirror-polish finish. During molding, maintain **moderate melt temperatures, stable mold temperatures, and multi-stage holding pressure**, followed by proper cooling/setting upon ejection. Strictly control residence time to minimize degradation and odors. Always perform a boiling water aging test on the first article before proceeding to mass production. If you need it, I can provide you with a separate copy of the **Standard Injection Molding Parameter Sheet for PP Food Containers (Arburg Machine Version)**, or a checklist for mold-flow analysis of plastic kitchenware.
We are a Custom Kitchen Plastic Parts Injection moulding manufacturer, providing high-quality Custom Kitchen Plastic Parts Injection moulding manufacturing. As long as you want to customize/develop Custom Kitchen Plastic Parts Injection moulding products, you can find us. We have professional injection mold design and mature manufacturing technology, providing you with one-stop service, from product design-mold making-product production-product packaging-product transportation, we can help you in every link. As long as you come to us, we will provide you with the ultimate service and satisfy you in terms of product quality, production time, information dialogue, etc.
|
Product Name |
Treadmill moulding |
|
Pls provide |
2D, 3D, samples, or the size of the multi-angle pictures |
|
Mould Time |
20-35 Days |
|
Product time |
7-15 Days |
|
Mould precision |
+/-0.01mm |
|
Mould life |
50-100 million shots |
|
Producing Process |
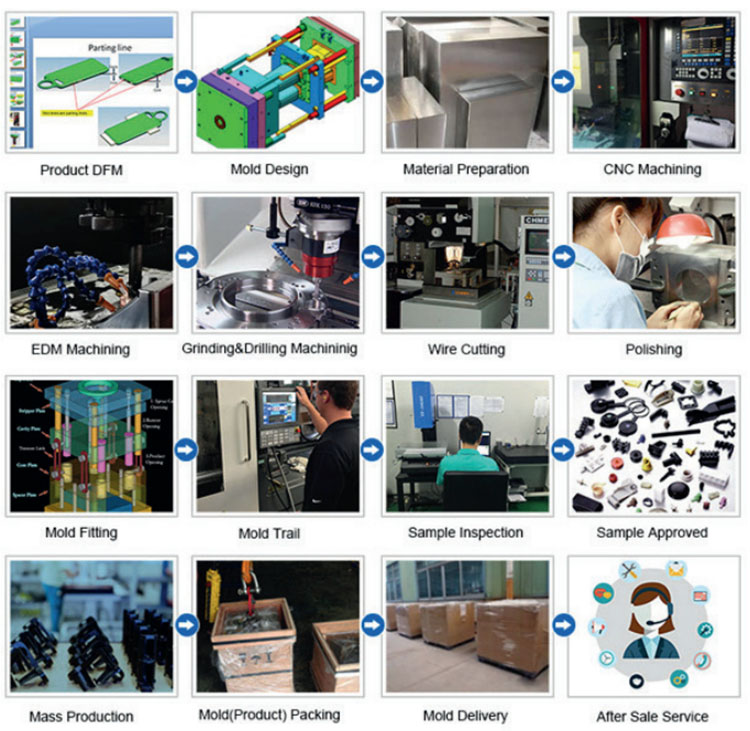
Audit drawings - mold flow analysis - design validation - Custom Materials - mold processing - core processing - electrode machining - Runner system processing - parts processing and procurement - machining acceptance - cavity surface treatment process - complex mode Die - The entire mold surface coating - Mounting plate - mold sample - sample test - sending samples |
|
Mould cavity |
One cavity, multi-cavity or same different products be made together |
|
Mould material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Runner system |
Hot runner and cold runner |
|
Base material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Finish |
Pitting the word, mirror finish, matte surface, striae |
|
Standard |
HASCO, DME or dependent upon |
|
Main technology |
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes, surface Finish, etc. |
|
Software |
CAD,PRO-E,UG Design Time: 1-3 days (normal circumstances) |
|
Product material |
ABS,PP,PC,PA6,PA66,TPU,POM,PBT,PVC,HIPS,PMMA,TPE,PC/ABS,TPV,TPO,TPR,EVA,HDPE,LDPE,CPVC,PVDF,PPSU.PPS. |
|
Quality system |
ISO9001:2008 |
|
Establish time |
20days |
|
Equipment |
CNC,EDM,Cutting off Machine,plastic machinery,etc plastic suitcase mould zhe jiang |
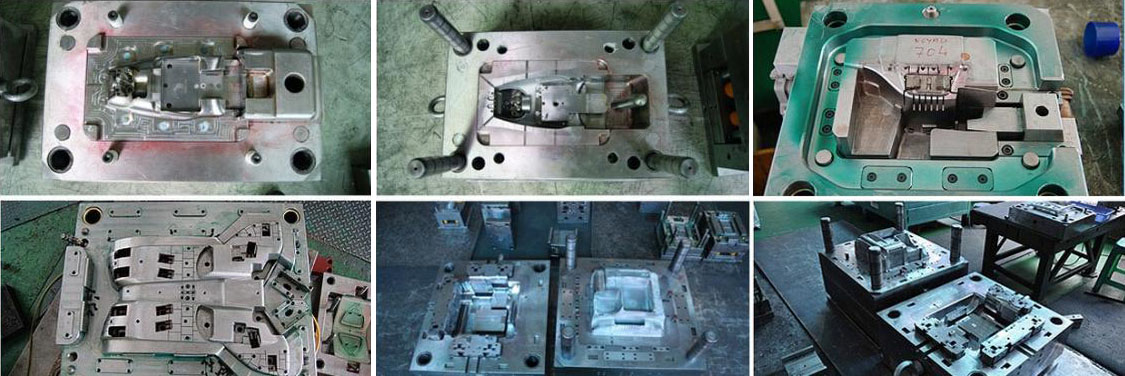
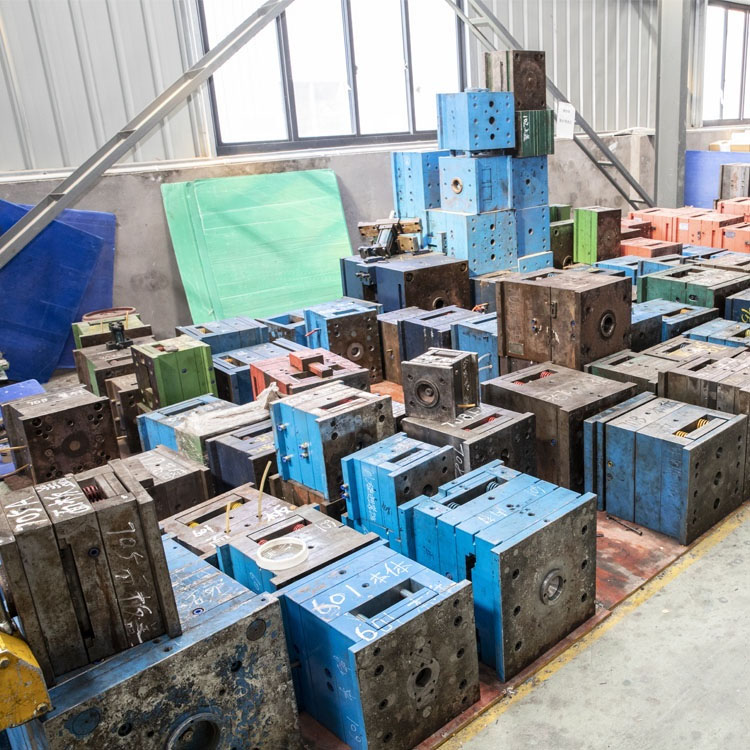
Plastic Injection Mould making
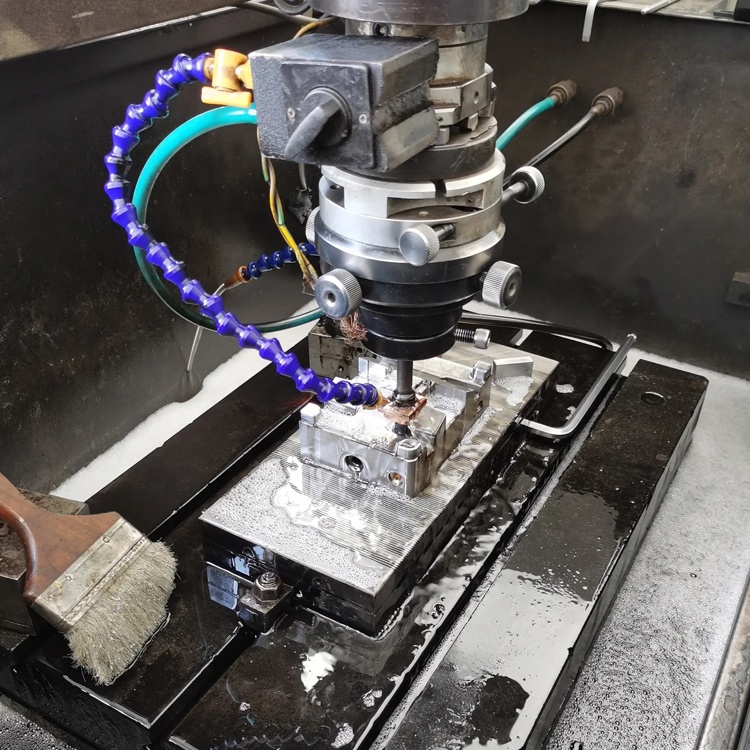
Plastic molding specifications
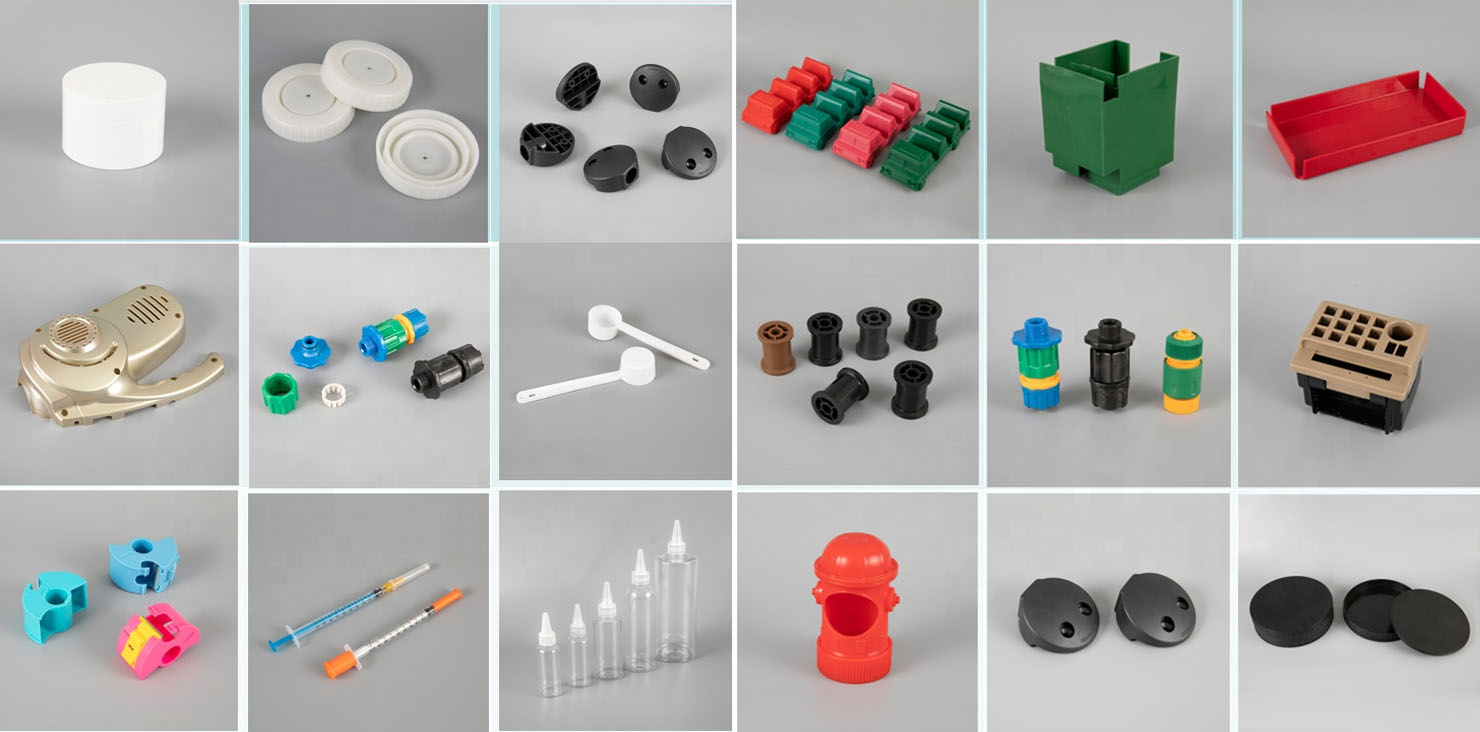
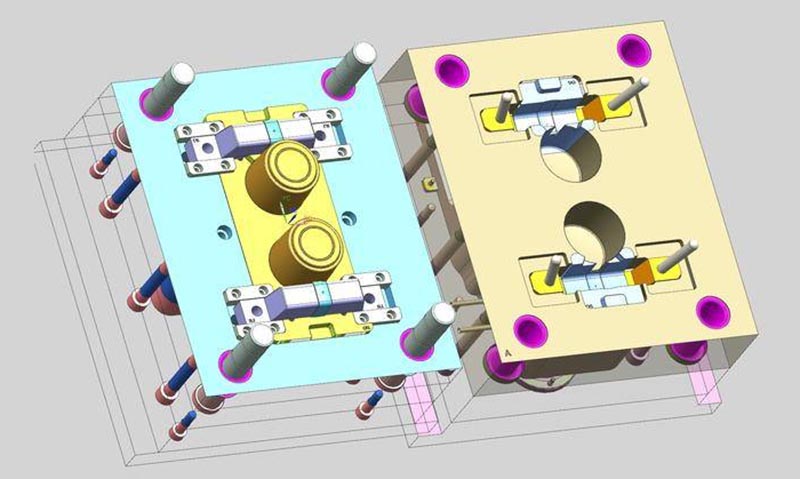
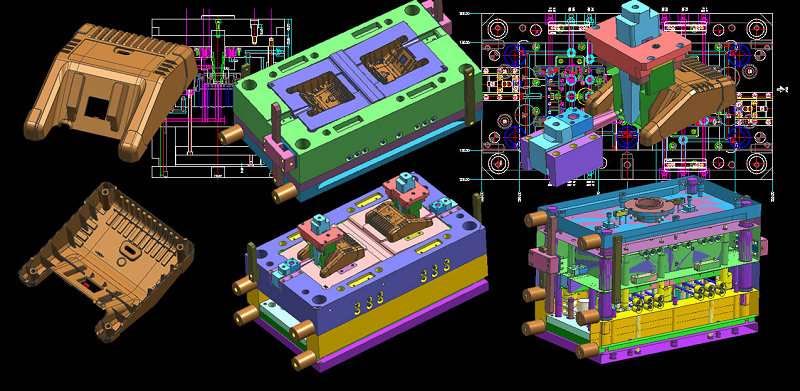
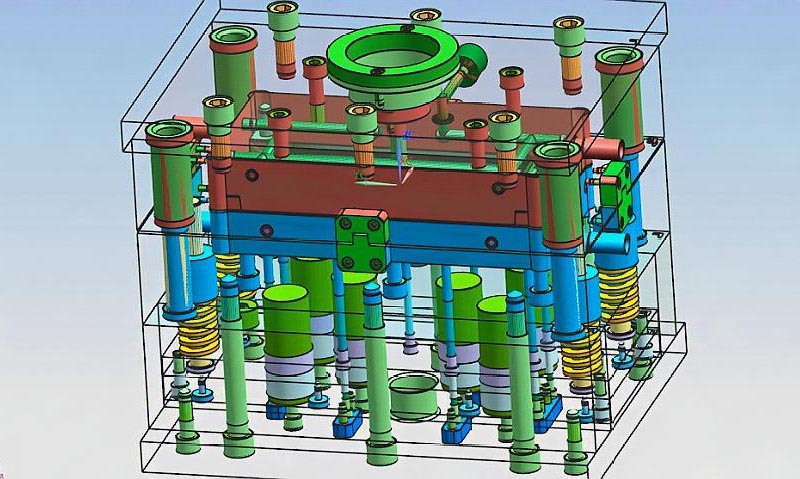
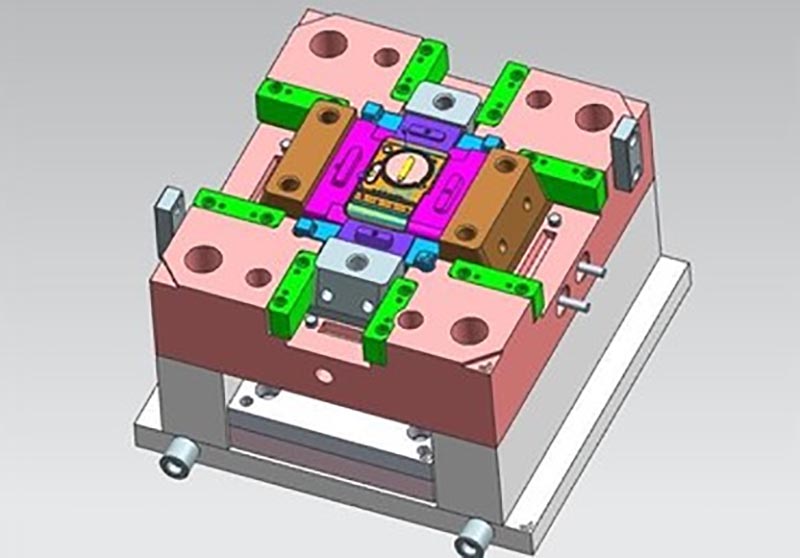
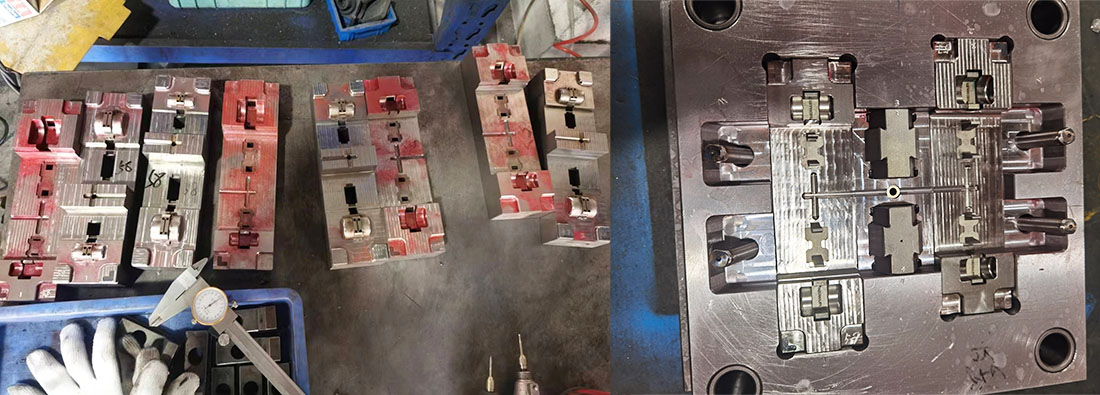
Mold design:
Transaction process:
Mold testing:

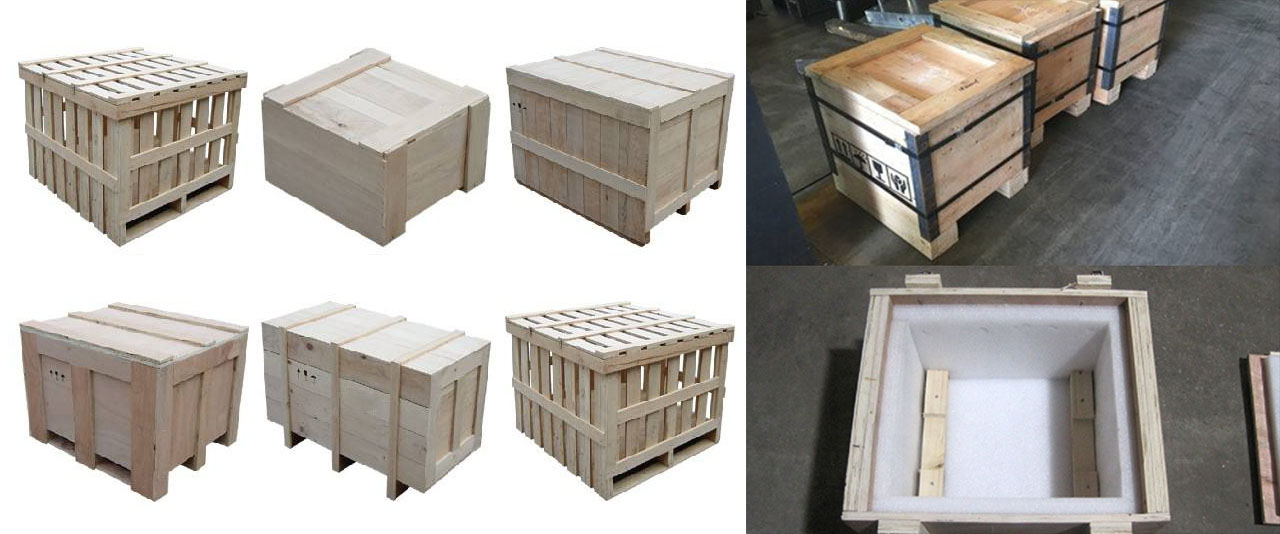
Product packaging
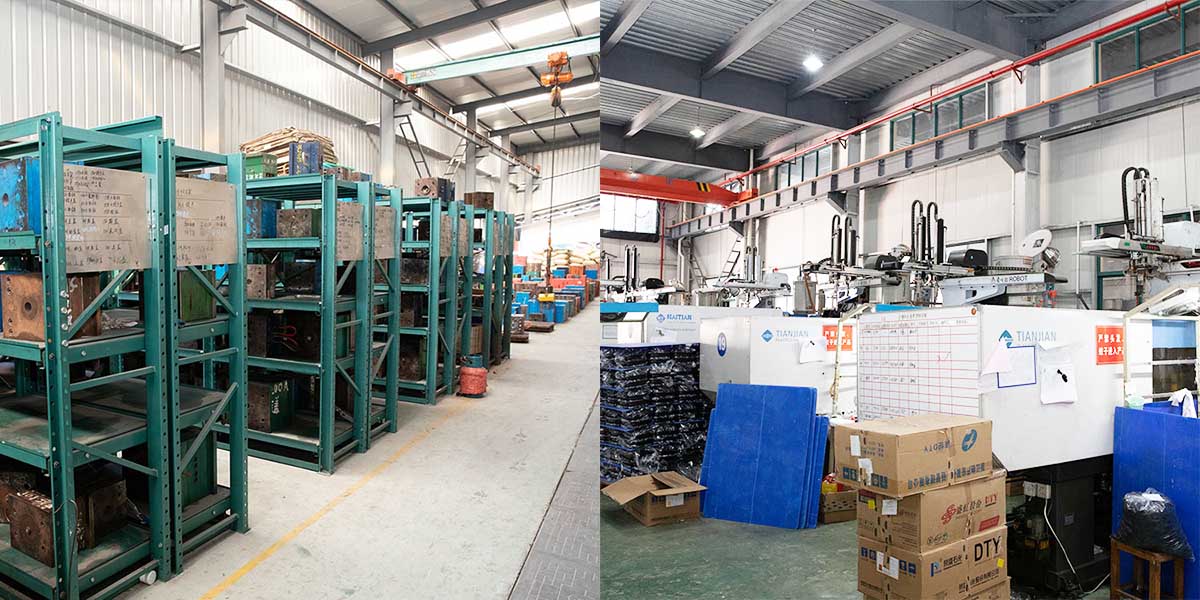
Factory
We are Custom Plastic Mold factory. Our factory is plastic injection mold maker. we has 17 years of experience in professional custom plastic mold and 10 years of foreign trade experience. We are custom Plastic Mold supplier. We can provide custom Plastic Mold service. Our factory can make the Injection molded plastic parts, and the quality of the products will satisfy you.
We have more than 50 high-end machines and hundreds of engineers and designers. We can provide one-stop service, from product design - mold making - product production - product packaging - transportation. We have a complete production chain. We can meet all your requirements.
Services we provide:
Professional custom mold service, Plastic mold design and manufacturing .plastic product production, product design, mold design, blow mold customization, rotational mold customization, die-casting mold customization. 3D printing services, CNC manufacturing services, product packaging, customized packaging, shipping services.
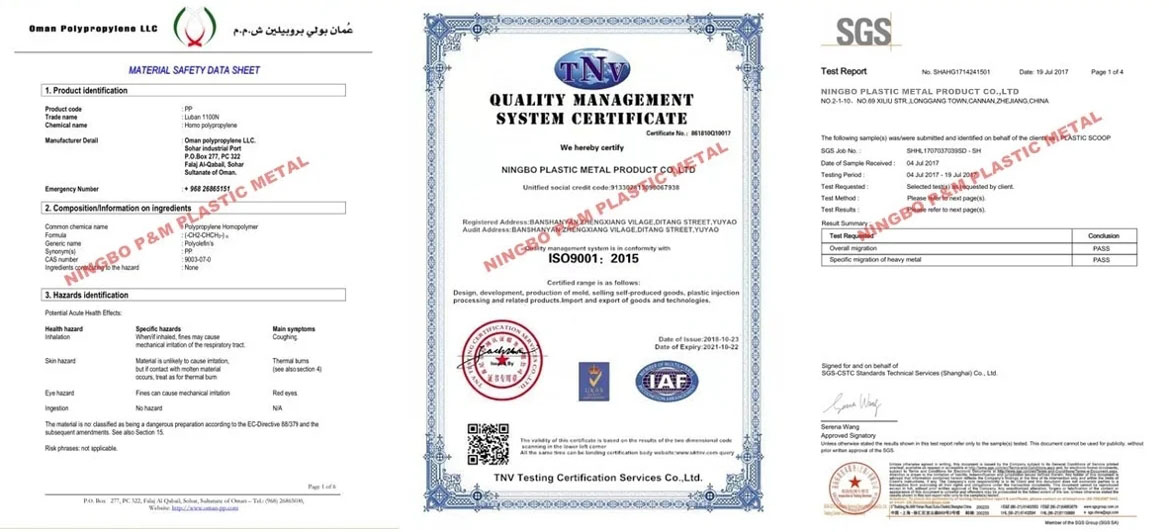

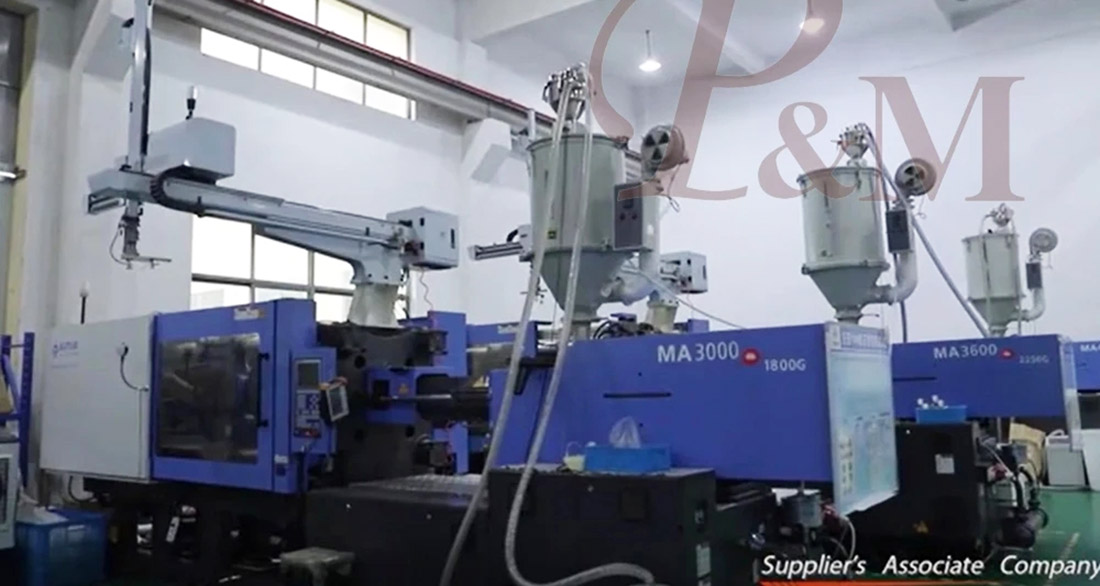
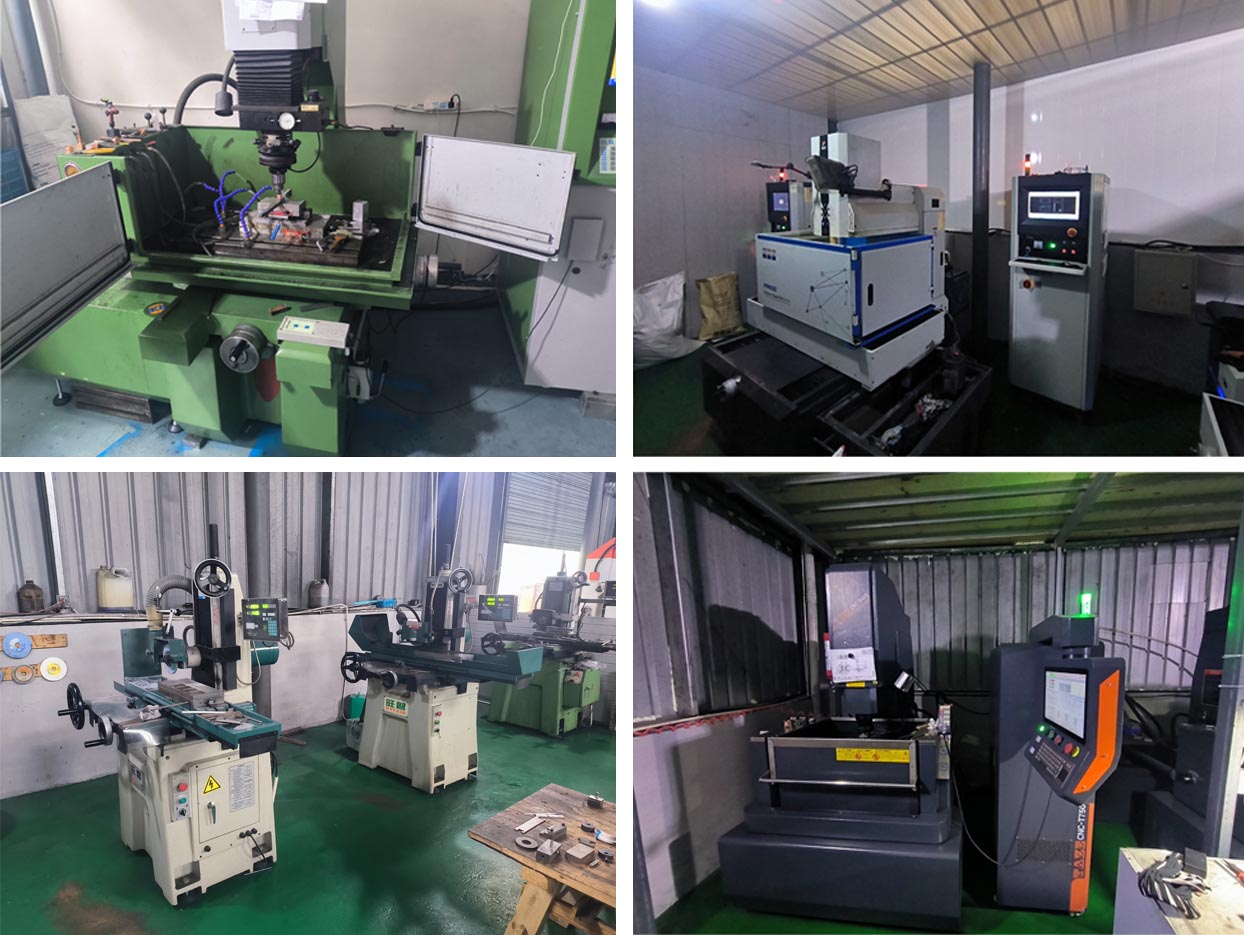
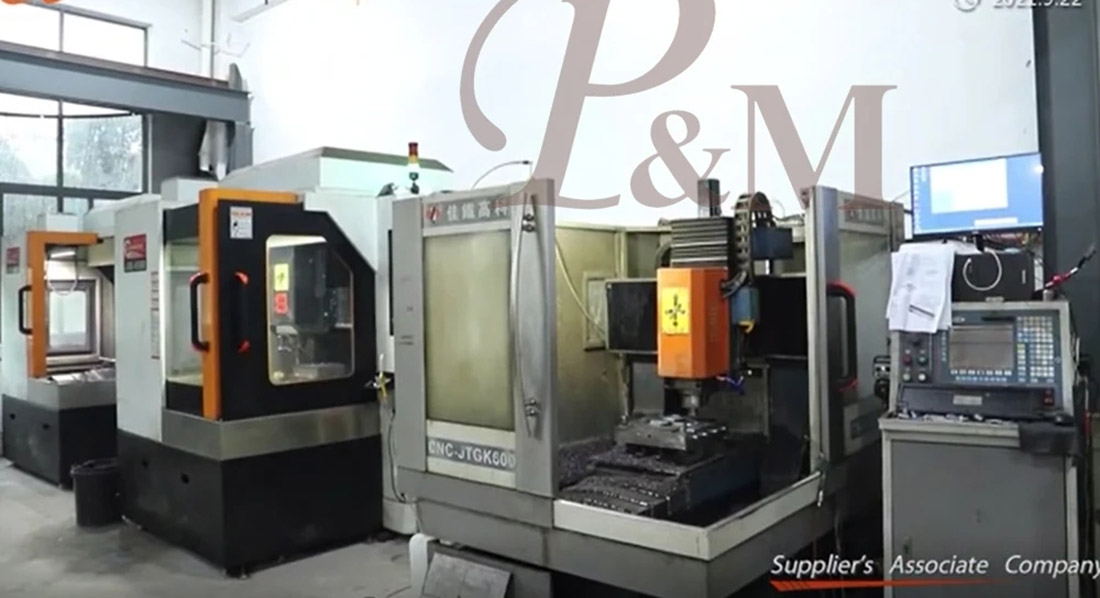
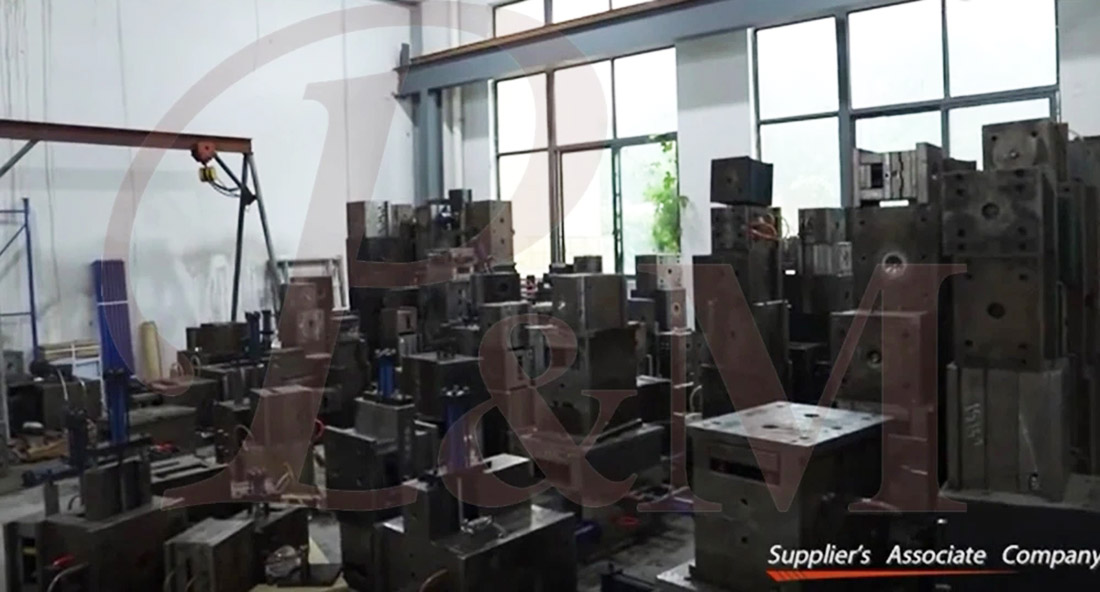
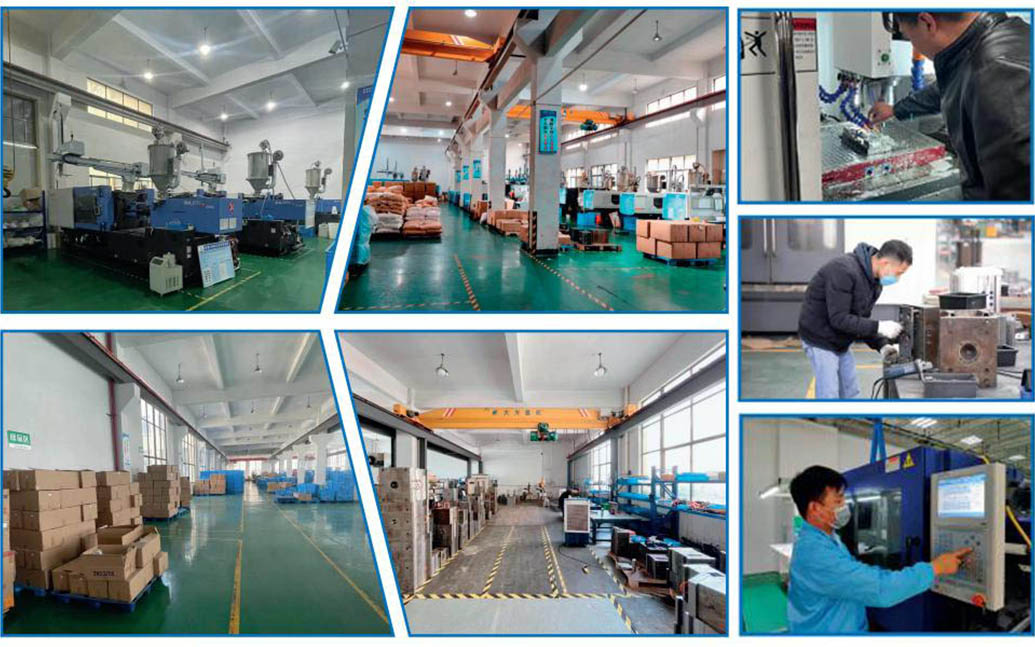
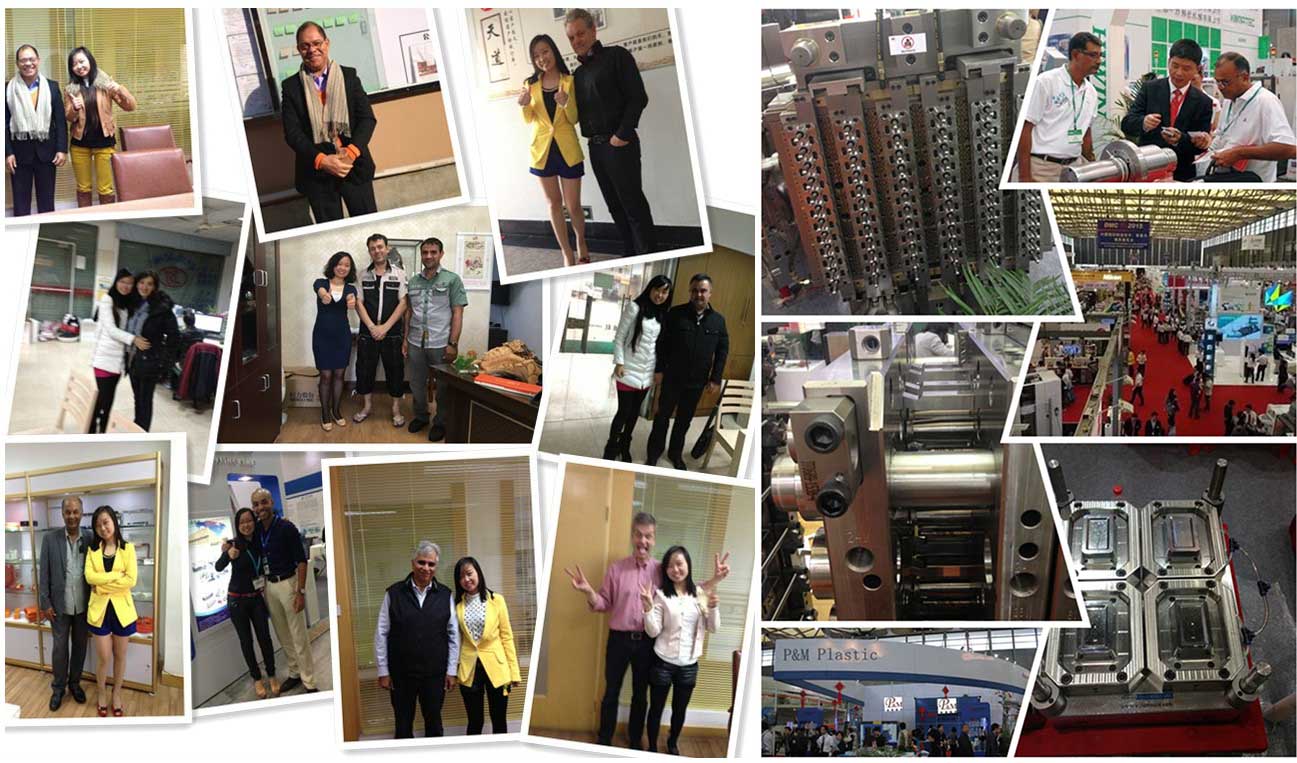
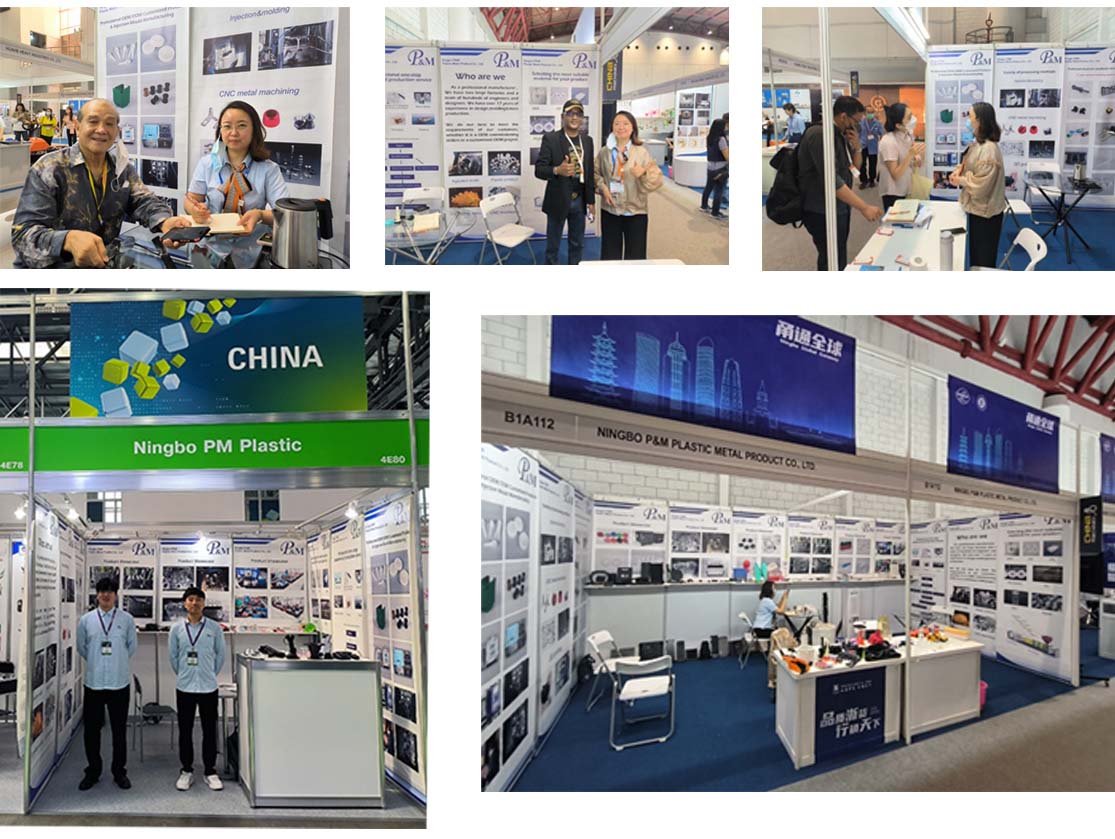
We always adhere to the principles of quality first and time first. While providing customers with the highest quality products, try to maximize the production efficiency and shorten production time. We are proud to tell every customer that our company has not lost any customer since its establishment.If there is a problem with the product, we will seek a solution actively and take responsibility to the end.

FAQ
Q1: Are you trading company or manufacturer ?
A: We are manufacturers.
Q2. When can I get the quotation?
A: We usually quote within 2 days after we get your inquiry.
If you are very urgent, please call us or tell us in your email so that we can quote for you first.
Q3. How long is the lead-time for mold?
A: It all depends on the products' size and complexity. Normally, the lead time is 25 days.
Q4. I have no 3D drawing, how should I start the new project?
A: You can supply us a molding sample, we will help you finish the 3D drawing design.
Q5. Before shipment, how to make sure the products quality?
A: If you don't come to our factory and also don't have the third party for inspection, we will be as your inspection worker.
We will supply you a video for production process detail include process report, products size structure and surface detail, packing detail and so on.
Q6. What is your payment terms?
A: Mold Payment: 40% deposit by T/T in advance, 30% second mold payment before sending out the first trial samples, 30% mold balance after you agree the final samples.
B:Production Payment: 50% deposit in advance, 50% before sending out the final goods.
Q7: How do you make our business long-term and good relationship?
A:1. We keep good quality and competitive price to ensure our customers benefit for best quality products.
2. We respect every customer as our friend and we sincerely do business and make friends with them, no matter where they come from.
Related Category
Send Inquiry
Please feel free to give your inquiry in the form below. We will reply you in 24 hours.