
Home
>
Product > Core Customization Service > Custom Molding > Injection Molded Kitchen Drain Basket Moulding
Product
- Core Customization Service
- Health Care
- Electronic Appliances and Instruments
- Maternal and Child Supplies Molds
- Recreational Sports
- Home Furnishing Art
- Auto Accessories
- Transportation and Warehousing
- Lighting Fixtures
- Construction Equipment
- Packaging Product
- Educational & Laboratories
- Clothing Luggage Accessories
- Care and Cleaning Products
- Agriculture & Forestry
- Mechanical Equipment
- Pet Supplies
- Kitchenware
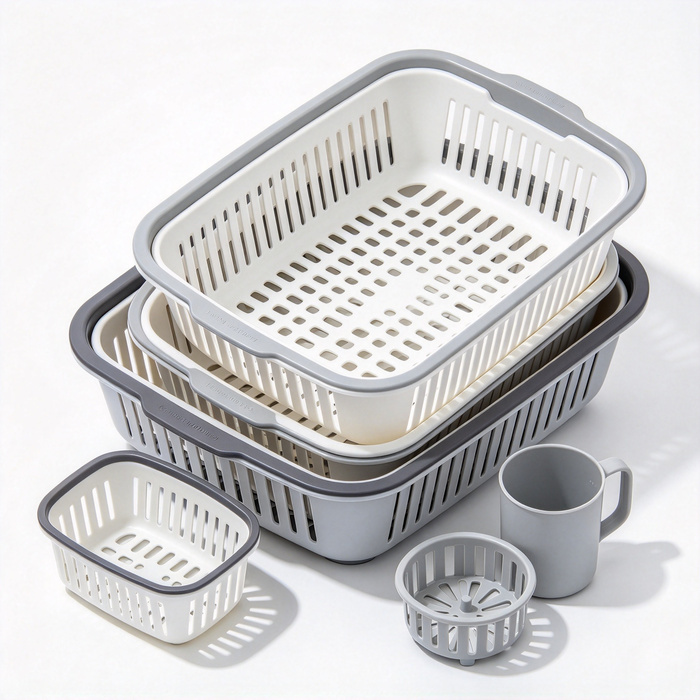
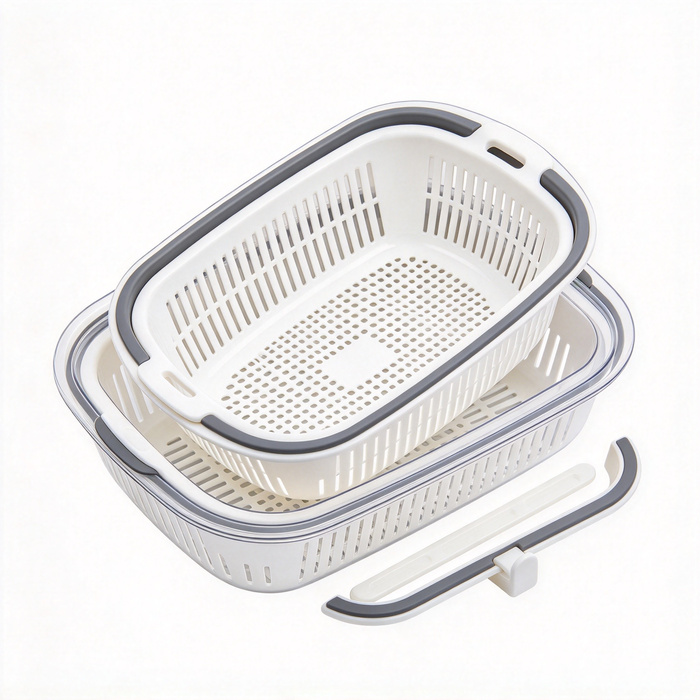
Injection Molded Kitchen Drain Basket Moulding
Ningbo (P&M) Plastic Metal Products Co., Ltd. has 17 years of mold manufacturing technology and can customize Injection Molded Kitchen Drain Basket moulding. We provide professional customized Injection Molded Kitchen Drain Basket moulding services, and we are a professional Injection Molded Kitchen Drain Basket moulding manufacturer. We have sufficient experience in selecting product raw materials and mold materials. In the process of customizing Injection Molded Kitchen Drain Basket moulding, our factory can provide one-stop service. We have design and production capabilities related to Injection Molded Kitchen Drain Basket moulding, such as: CAD design, mold manufacturing, injection molding, plastic product production, assembly and other technologies.
Send Inquiry
Product Description
In addition, our company has established cooperative relationships with plastic raw material suppliers, printing manufacturers, etc. to ensure the supply of raw materials and printing quality. Through our rich experience and perfect supply chain, our company can provide customers with high-quality customized Injection Molded Kitchen Drain Basket moulding products to meet their specific needs. At the same time, we have 10 years of professional foreign trade service experience, understand the foreign trade process, and better serve our customers. For Injection Molded Kitchen Drain Basket moulding products, we can make corresponding plastic parts, which is mainly done through injection molds.
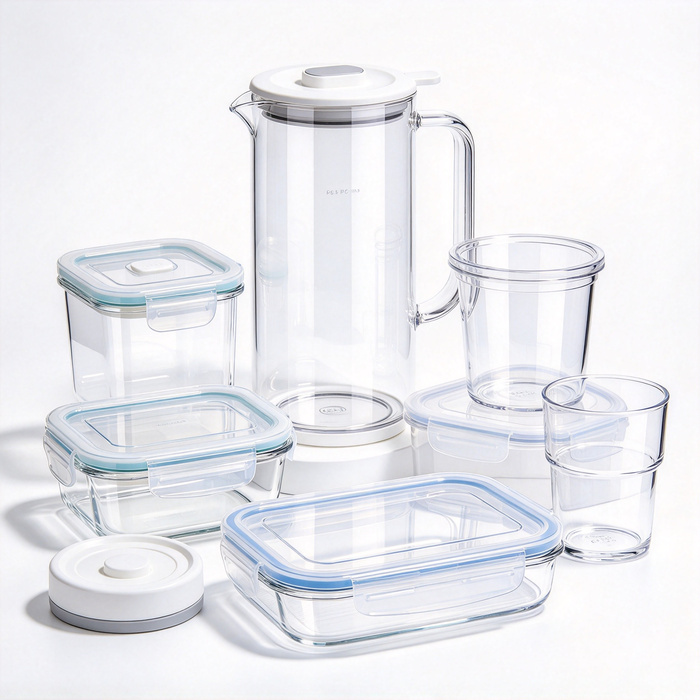
Colanders fall under the category of **food-contact, porous PP components** (or occasionally transparent Tritan). Unlike standard storage containers, they present unique challenges: they feature a large surface area covered in drainage holes, thin walls, long flow paths, a high risk of trapped air and weld lines, a tendency to deform or soften, sink marks around the holes, and stress points at the handles. Furthermore, they must comply with standards such as GB 4806.7 or EU 10/2011 and demonstrate resistance to hot water and dishwashing detergents.
The preferred material is **food-grade copolymer PP**; homopolymer PP is not recommended due to its high shrinkage and susceptibility to warping.
>
> Key technical challenges: venting through a dense array of small holes, ensuring the strength of weld lines between holes, preventing deformation of the rim, avoiding sink marks around the holes, and preventing breakage at the base of the handles.
## I. Product DFM (Design for Manufacturing) Essentials
### 1. Wall Thickness
- Side walls: **1.4–1.8 mm**. The rim (top edge) should be thickened to **1.8–2.2 mm** to resist deformation, as colander rims are highly prone to outward flaring or becoming oval-shaped.
- Ribs between drainage holes: The thickness should be **≤0.6 times the main wall thickness**, with a root radius (R) of **0.3–0.5 mm**.
>
> ❌ Common Pitfall: If the ribs between holes are too thick, visible sink marks will appear on the outer surface of the colander—a defect immediately noticeable to the end user.
- Base: Incorporate circular or cross-shaped reinforcing ribs. A flat base is insufficient, as it may collapse or sag when exposed to hot water.
### 2. Drainage Hole Design (Critical)
1. Hole shape: Prefer **rounded-corner oblong or elliptical holes** over small circular ones. These facilitate better plastic flow and more efficient air venting; small holes with sharp corners are prone to trapped air, which can lead to scorching (burn marks).
2. Hole spacing: Ensure sufficient material (plastic) between the holes. If the holes are too densely packed, the resulting ribs will be too thin, leading to concentrated weld lines and structural fragility—causing the material to break easily under stress. 3. Demolding of Holes:
- Through-holes: Use mold pins (inserts). These pins must have a draft angle of ≥1°. The pins should be polished; otherwise, issues such as sticking, stress whitening, or burrs around the hole edges may occur.
- For designs with a large number of small-diameter pins: Consider the structural strength of the pins, as thin pins are prone to bending or breaking.
4. Avoid arranging holes in a straight line across the direction of material flow; this creates a continuous weld line, weakening the structural integrity of the entire circumference. Instead, use a staggered arrangement to disperse the weld lines.
### 3. Handle Structure
The handle of a draining basket is a high-stress area:
- Incorporate a large radius (R ≥ 0.6mm) at the base of the handle for a smooth transition.
- The base of the handle **must not be positioned on a weld line**.
- Add localized reinforcing ribs where the handle connects to the basket body; ensure these ribs do not cause sink marks on the outer surface.
- Avoid thin, unsupported (cantilevered) handle designs, as they are prone to breaking when the basket is filled with water.
### 4. Draft Angles
- Outer surfaces: ≥1° for PP.
- Draft angle for drainage hole pins: ≥1.2°.
- For the deep cavity of the basket, increase the draft angle on the inner walls to prevent the part from gripping the core and becoming deformed during ejection.
### 5. Shrinkage and Symmetry
For copolymer PP, use a shrinkage factor of **1.2%–1.5%**. Draining baskets are typically circular or elliptical; maintain a symmetrical structure whenever possible. Asymmetrical placement of drainage holes can lead to uneven shrinkage, causing the rim of the basket to warp into an elliptical shape.
>
> Key areas for mold flow analysis: locations where melt fronts converge (weld lines), potential air traps, and the tendency for the basket rim to warp.
## II. Mold Design Essentials
1. **Steel Selection**
For cavities, visible surfaces (such as the basket rim), and drainage pins: Use S136 steel, hardened to HRC 48–52. This material offers excellent rust resistance and polishability, and is suitable for food-grade applications.
Pins should be heat-treated individually to ensure wear resistance and rigidity; small-diameter pins require anti-rotation positioning features. 2. **Gating Strategy**
- For high aesthetic requirements: Use a **bottom-center valve-gated hot runner system**. Injecting from the center of the base allows the material to flow outward, ensuring that weld lines are distributed uniformly.
- For a low-cost approach: Use multiple submarine gates located at the base. **Injection from the rim (the basket opening) is strictly prohibited**; direct injection at the rim creates high shear stress, which leads to deformation of the opening when exposed to hot water.
>
> Prohibited: Do not position gates to inject directly toward the base of the handle or areas with a high density of drainage holes.
3. **Venting (The primary challenge for colander molds!)**
Colanders feature numerous drainage pins; the clearance between these pins and the cavity can easily trap air. Furthermore, as multiple melt fronts converge between the holes, air entrapment becomes a common issue, often resulting in scorching, black spots, or brittle weld lines.
- Vent depth (for PP): **0.015–0.02 mm**
- Vent placement:
✅ At every point where melt fronts converge.
✅ At the base and around the perimeter of the drainage pins (many molds only include vents at the parting line, neglecting the areas around the pins).
✅ At the end of the flow path (the final fill points) and along the entire parting line around the rim.
- In areas with a high density of holes, consider using **venting inserts** to facilitate the cleaning and polishing of the vent channels.
>
> Scorching or black spots are considered critical defects for food-contact items like colanders.
4. **Ejection System**
Because a colander is a deep-cavity, multi-perforated part, it exerts significant gripping force on the mold. Relying on isolated ejection points can easily cause stress marks ("whitening"), deformation, or bowing of the basket base.
- Preferred method: Use an **ejector plate combined with ejector pins** to ensure synchronized, uniform ejection across the entire part.
- Position ejector pins along the reinforcing ribs at the base or along the rim, avoiding visible exterior surfaces and drainage holes.
- In areas with small, closely spaced drainage holes, avoid placing ejector pins directly against the edges of the holes. 5. **Insert Pin Maintenance Design**
Given the large number of insert pins for the drainage holes—which are prone to flash and wear during long-term production—the mold is designed to allow for the individual replacement of these pins. This eliminates the need to disassemble the entire cavity assembly, thereby saving time during mold maintenance.
We are a Injection Molded Kitchen Drain Basket moulding manufacturer, providing high-quality Injection Molded Kitchen Drain Basket moulding manufacturing. As long as you want to customize/develop Injection Molded Kitchen Drain Basket moulding products, you can find us. We have professional injection mold design and mature manufacturing technology, providing you with one-stop service, from product design-mold making-product production-product packaging-product transportation, we can help you in every link. As long as you come to us, we will provide you with the ultimate service and satisfy you in terms of product quality, production time, information dialogue, etc.
|
Product Name |
Treadmill moulding |
|
Pls provide |
2D, 3D, samples, or the size of the multi-angle pictures |
|
Mould Time |
20-35 Days |
|
Product time |
7-15 Days |
|
Mould precision |
+/-0.01mm |
|
Mould life |
50-100 million shots |
|
Producing Process |
Audit drawings - mold flow analysis - design validation - Custom Materials - mold processing - core processing - electrode machining - Runner system processing - parts processing and procurement - machining acceptance - cavity surface treatment process - complex mode Die - The entire mold surface coating - Mounting plate - mold sample - sample test - sending samples |
|
Mould cavity |
One cavity, multi-cavity or same different products be made together |
|
Mould material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Runner system |
Hot runner and cold runner |
|
Base material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Finish |
Pitting the word, mirror finish, matte surface, striae |
|
Standard |
HASCO, DME or dependent upon |
|
Main technology |
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes, surface Finish, etc. |
|
Software |
CAD,PRO-E,UG Design Time: 1-3 days (normal circumstances) |
|
Product material |
ABS,PP,PC,PA6,PA66,TPU,POM,PBT,PVC,HIPS,PMMA,TPE,PC/ABS,TPV,TPO,TPR,EVA,HDPE,LDPE,CPVC,PVDF,PPSU.PPS. |
|
Quality system |
ISO9001:2008 |
|
Establish time |
20days |
|
Equipment |
CNC,EDM,Cutting off Machine,plastic machinery,etc plastic suitcase mould zhe jiang |
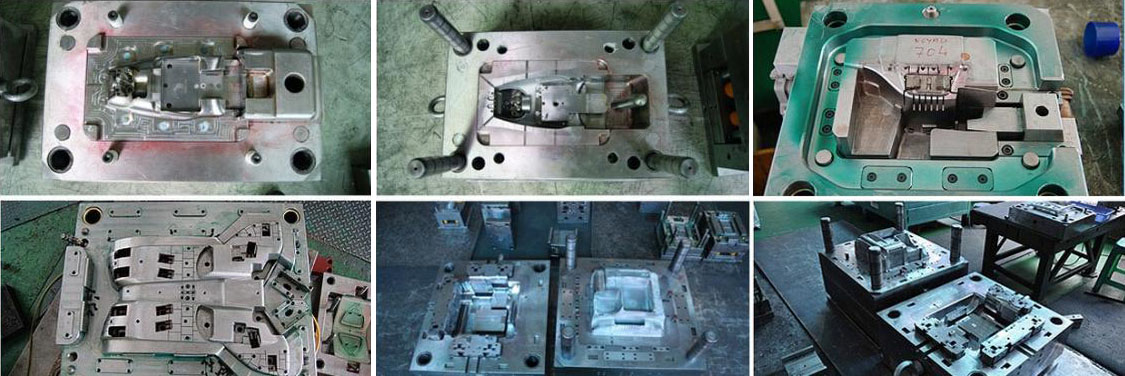
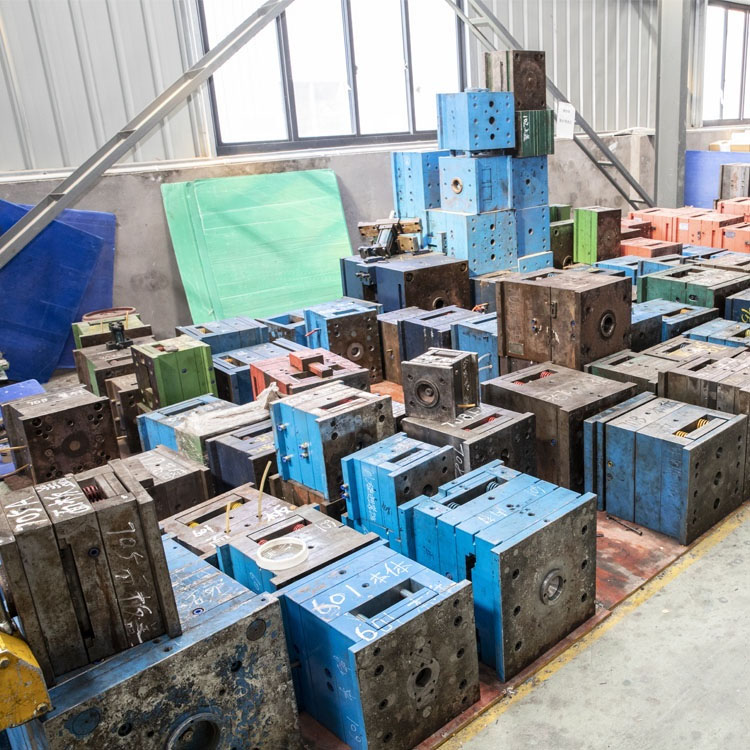
Plastic Injection Mould making
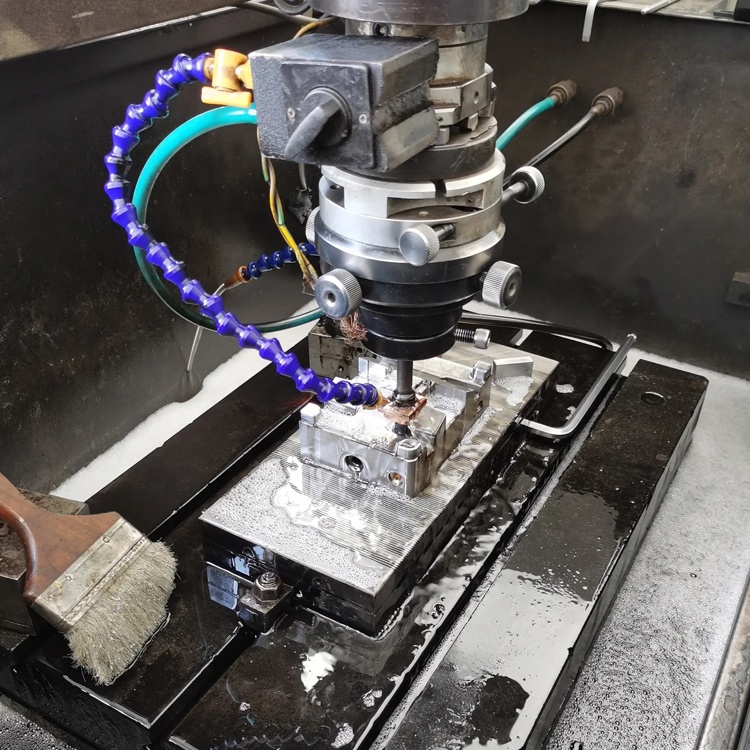
Plastic molding specifications
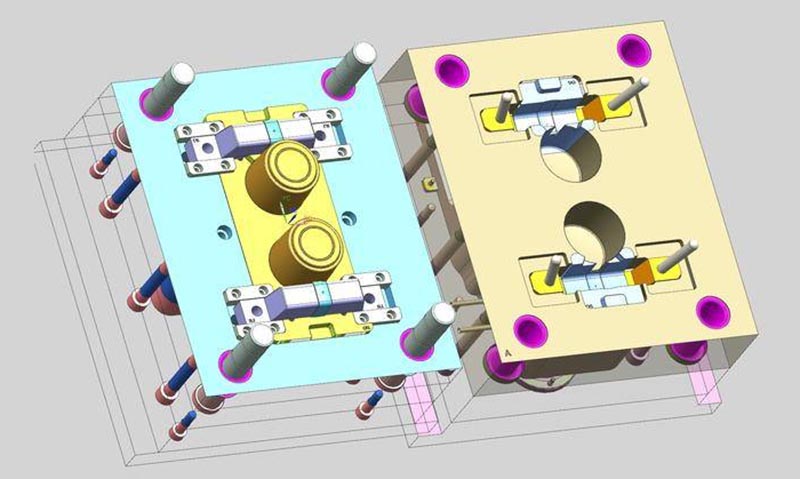
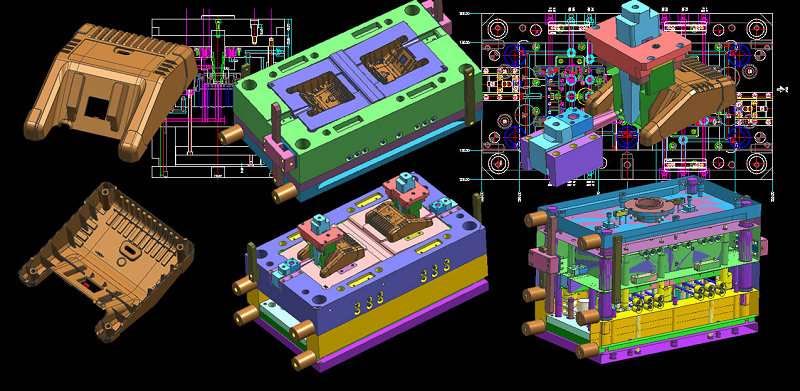
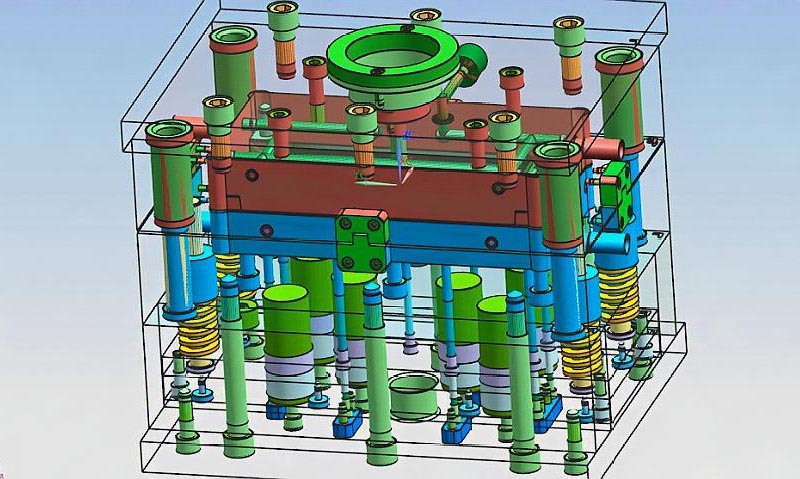
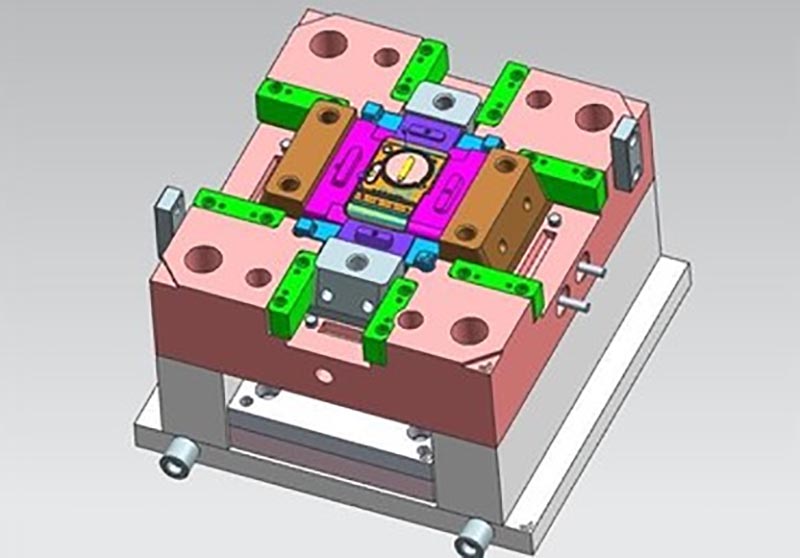
Mold design:
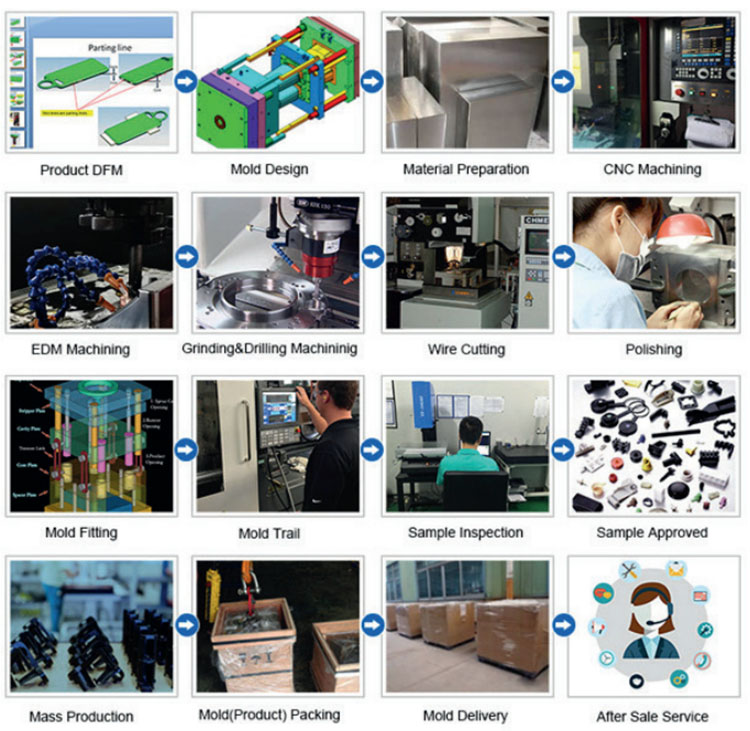
Transaction process:
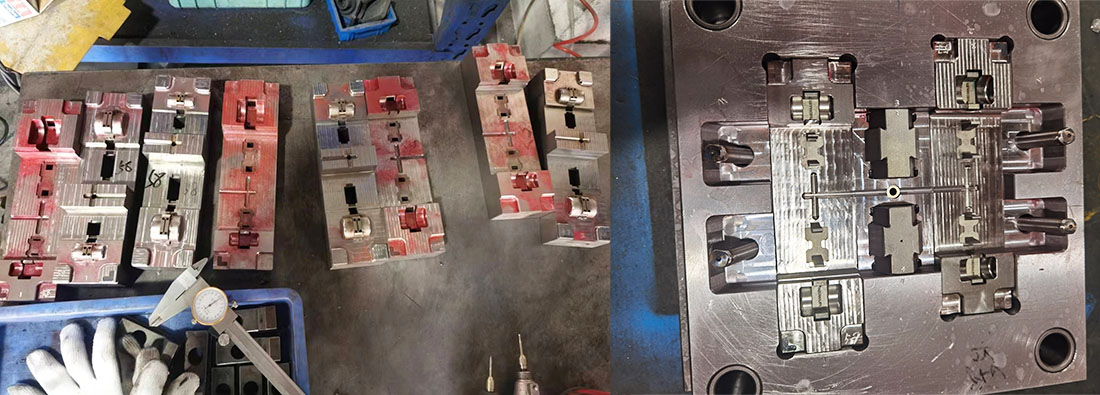
Mold testing:

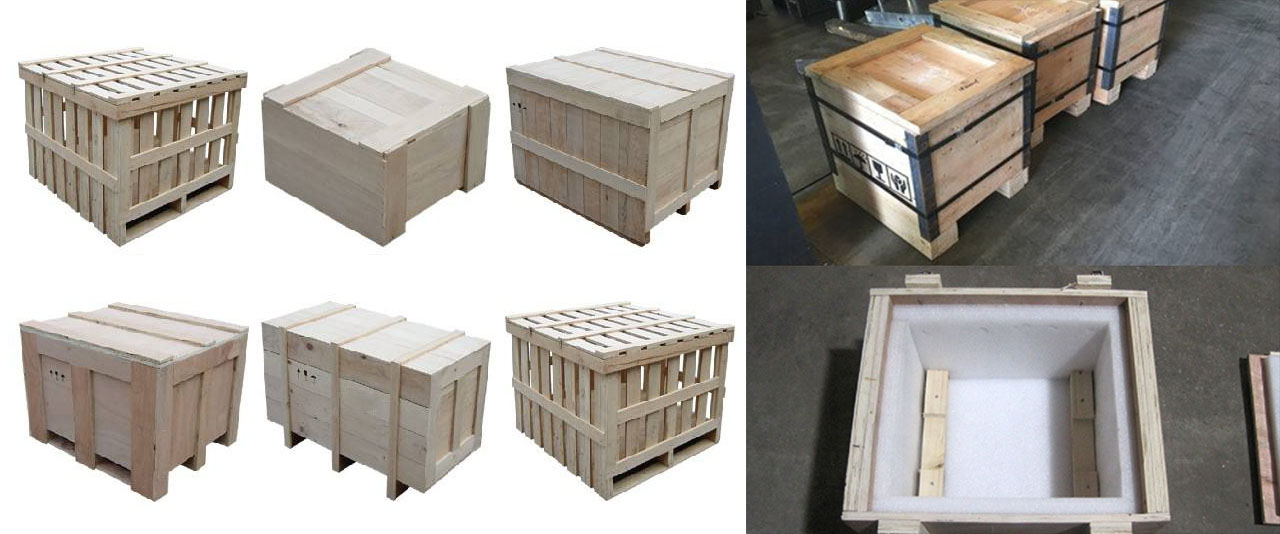
Product packaging
Factory
We are Custom Plastic Mold factory. Our factory is plastic injection mold maker. we has 17 years of experience in professional custom plastic mold and 10 years of foreign trade experience. We are custom Plastic Mold supplier. We can provide custom Plastic Mold service. Our factory can make the Injection molded plastic parts, and the quality of the products will satisfy you.
We have more than 50 high-end machines and hundreds of engineers and designers. We can provide one-stop service, from product design - mold making - product production - product packaging - transportation. We have a complete production chain. We can meet all your requirements.
Services we provide:
Professional custom mold service, Plastic mold design and manufacturing .plastic product production, product design, mold design, blow mold customization, rotational mold customization, die-casting mold customization. 3D printing services, CNC manufacturing services, product packaging, customized packaging, shipping services.
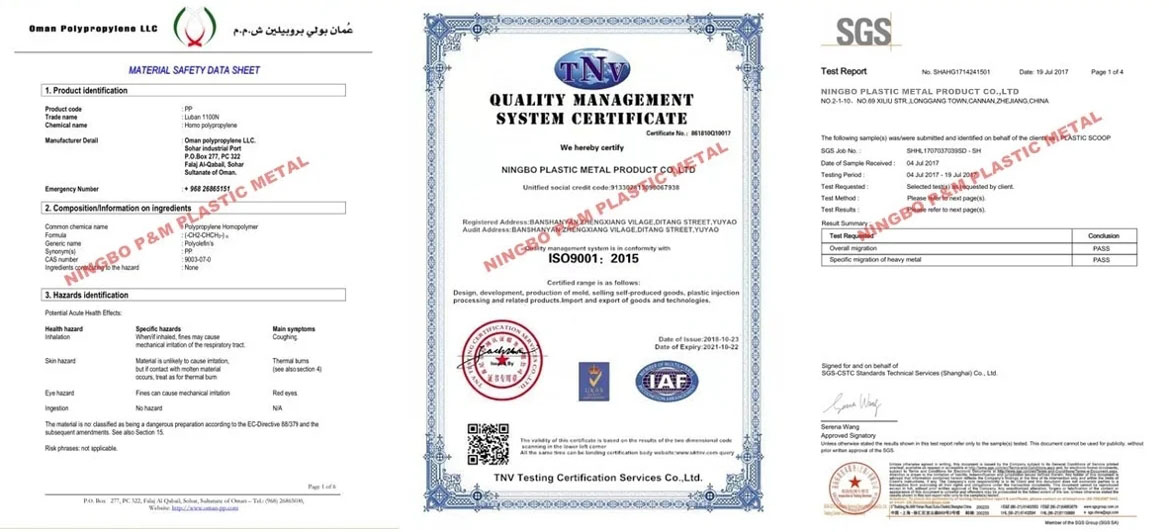

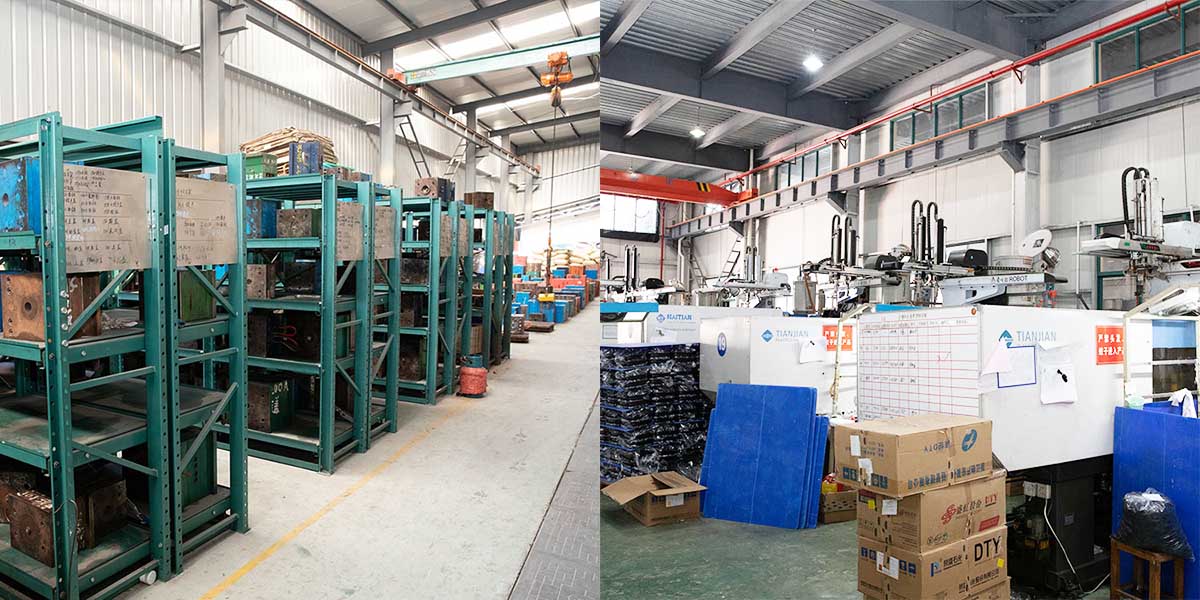
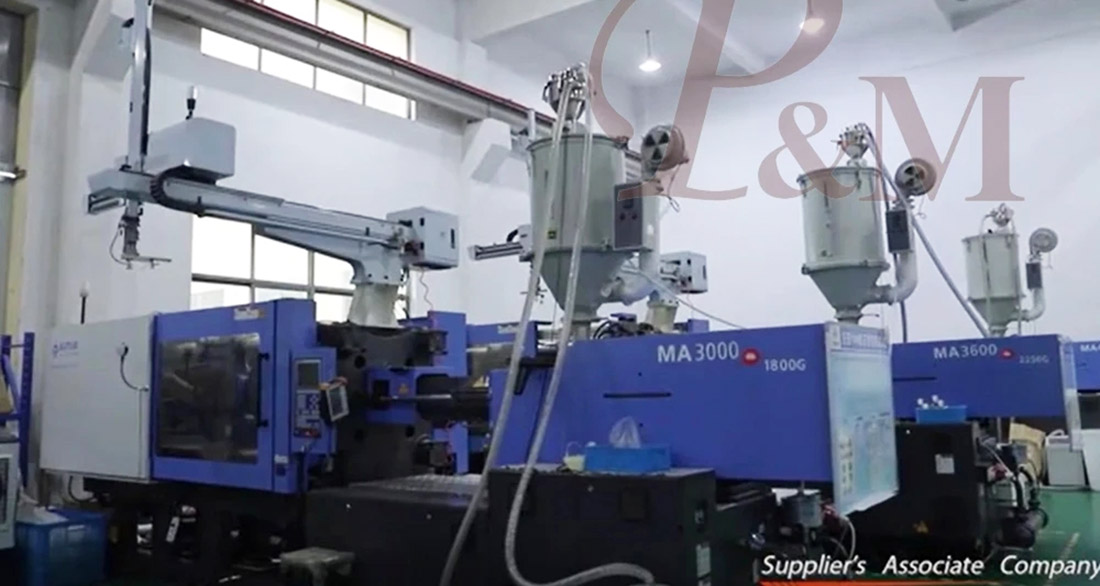
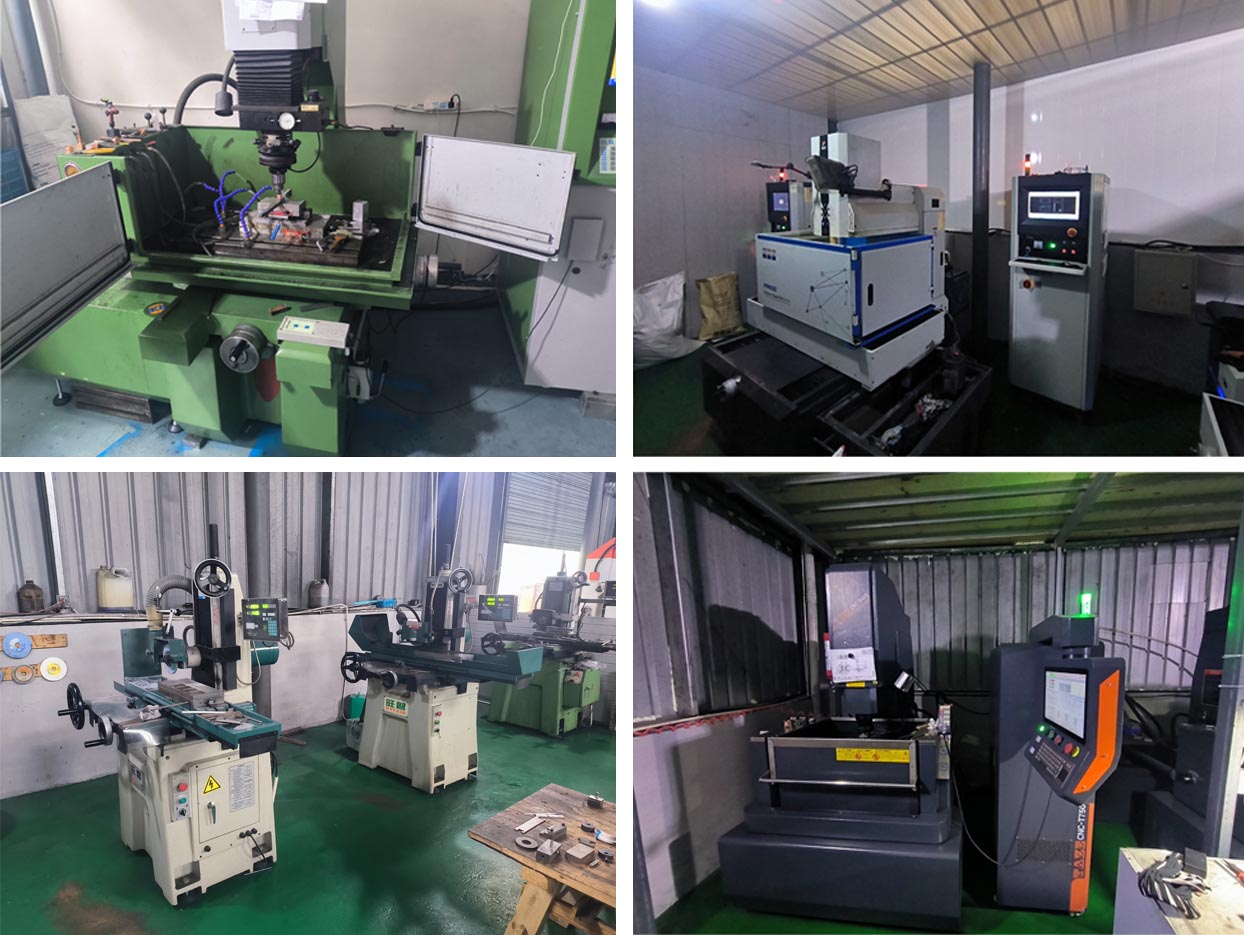
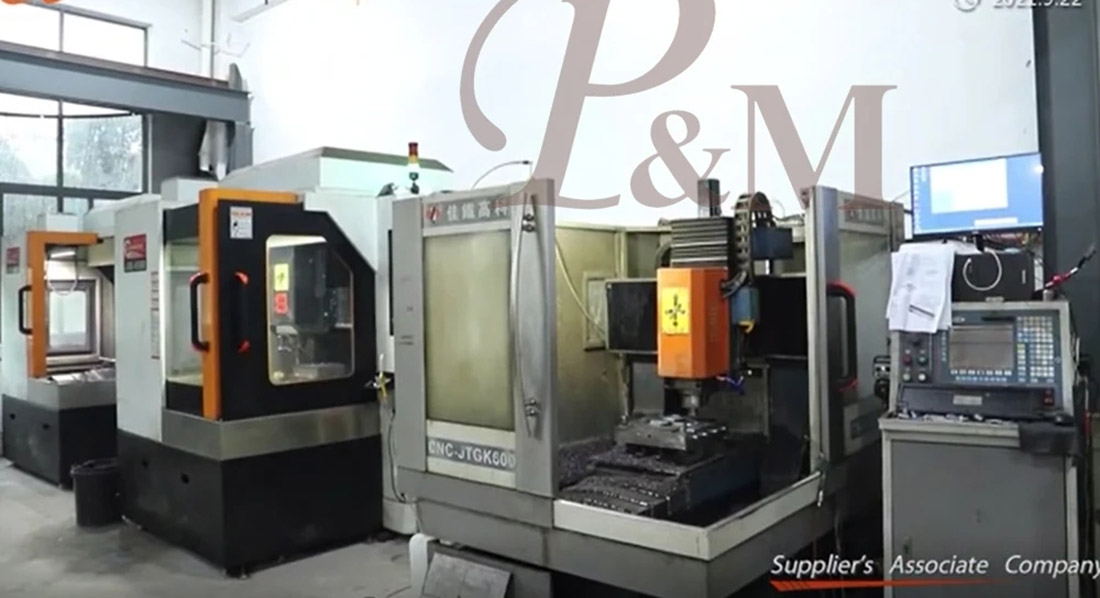
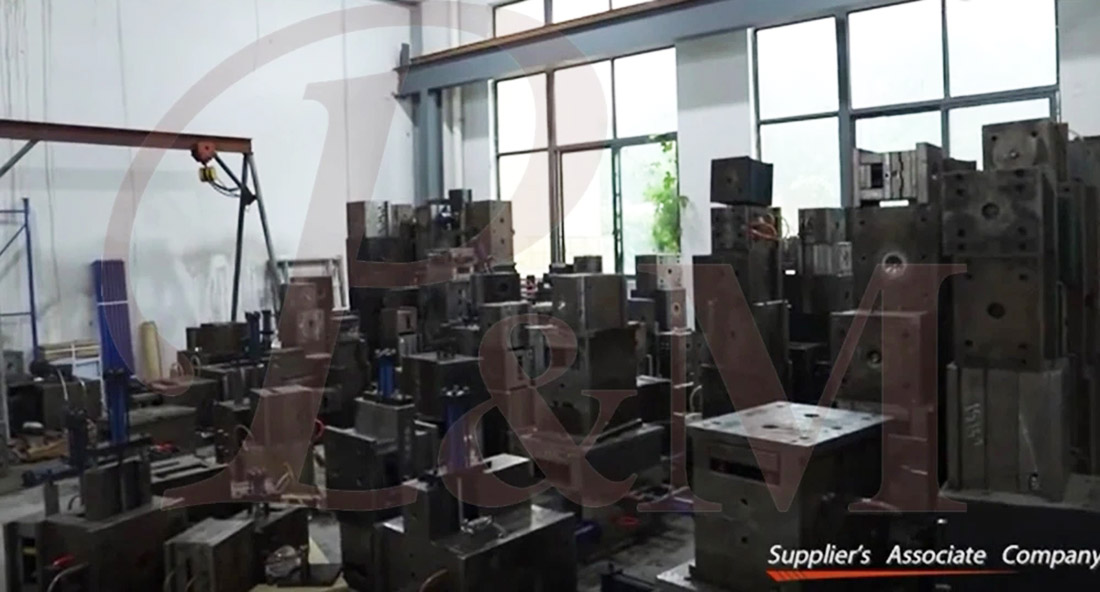
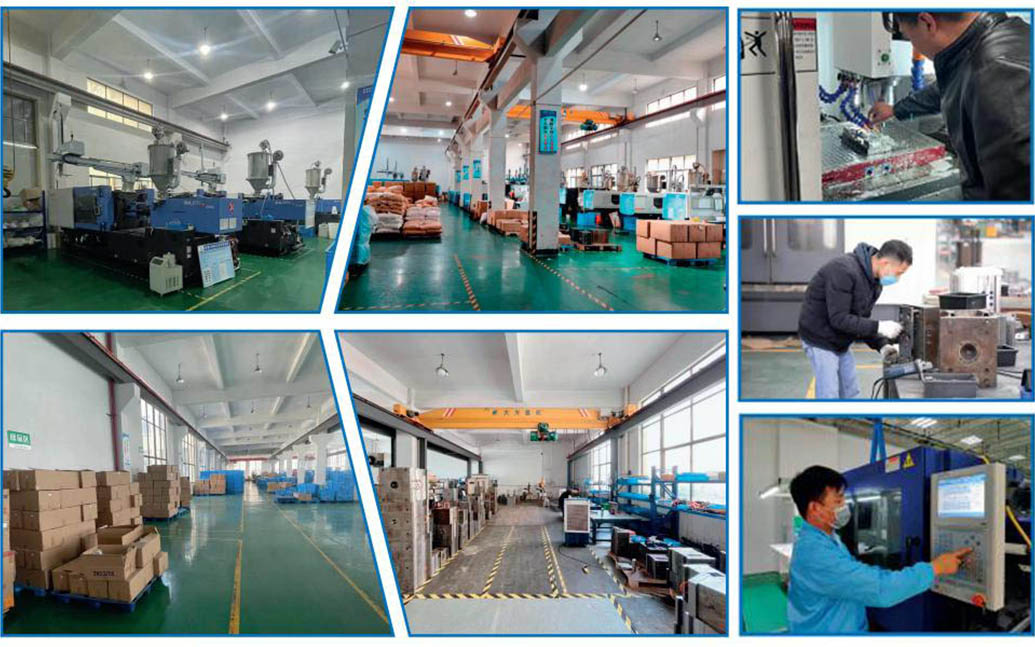
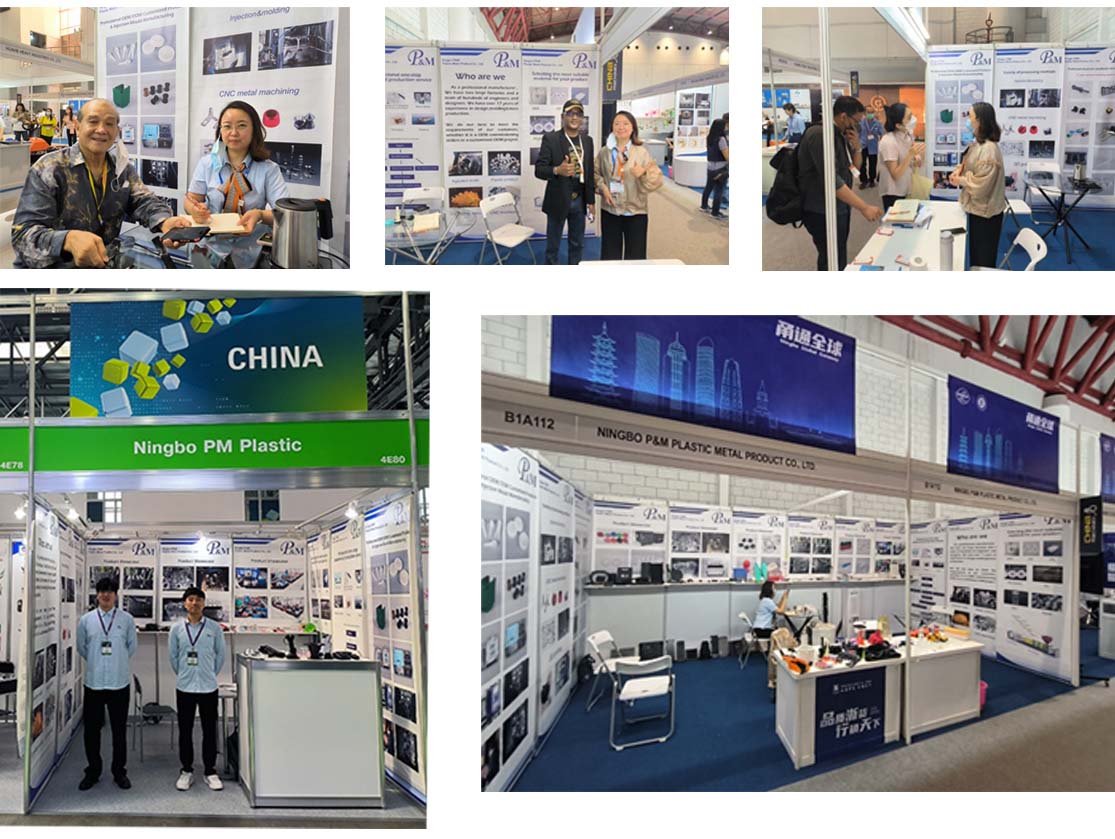
We always adhere to the principles of quality first and time first. While providing customers with the highest quality products, try to maximize the production efficiency and shorten production time. We are proud to tell every customer that our company has not lost any customer since its establishment.If there is a problem with the product, we will seek a solution actively and take responsibility to the end.

FAQ
Q1: Are you trading company or manufacturer ?
A: We are manufacturers.
Q2. When can I get the quotation?
A: We usually quote within 2 days after we get your inquiry.
If you are very urgent, please call us or tell us in your email so that we can quote for you first.
Q3. How long is the lead-time for mold?
A: It all depends on the products' size and complexity. Normally, the lead time is 25 days.
Q4. I have no 3D drawing, how should I start the new project?
A: You can supply us a molding sample, we will help you finish the 3D drawing design.
Q5. Before shipment, how to make sure the products quality?
A: If you don't come to our factory and also don't have the third party for inspection, we will be as your inspection worker.
We will supply you a video for production process detail include process report, products size structure and surface detail, packing detail and so on.
Q6. What is your payment terms?
A: Mold Payment: 40% deposit by T/T in advance, 30% second mold payment before sending out the first trial samples, 30% mold balance after you agree the final samples.
B:Production Payment: 50% deposit in advance, 50% before sending out the final goods.
Q7: How do you make our business long-term and good relationship?
A:1. We keep good quality and competitive price to ensure our customers benefit for best quality products.
2. We respect every customer as our friend and we sincerely do business and make friends with them, no matter where they come from.
Related Category
Send Inquiry
Please feel free to give your inquiry in the form below. We will reply you in 24 hours.