
Product
- Core Customization Service
- Health Care
- Electronic Appliances and Instruments
- Maternal and Child Supplies Molds
- Recreational Sports
- Home Furnishing Art
- Auto Accessories
- Transportation and Warehousing
- Lighting Fixtures
- Construction Equipment
- Packaging Product
- Educational & Laboratories
- Clothing Luggage Accessories
- Care and Cleaning Products
- Agriculture & Forestry
- Mechanical Equipment
- Pet Supplies
- Kitchenware
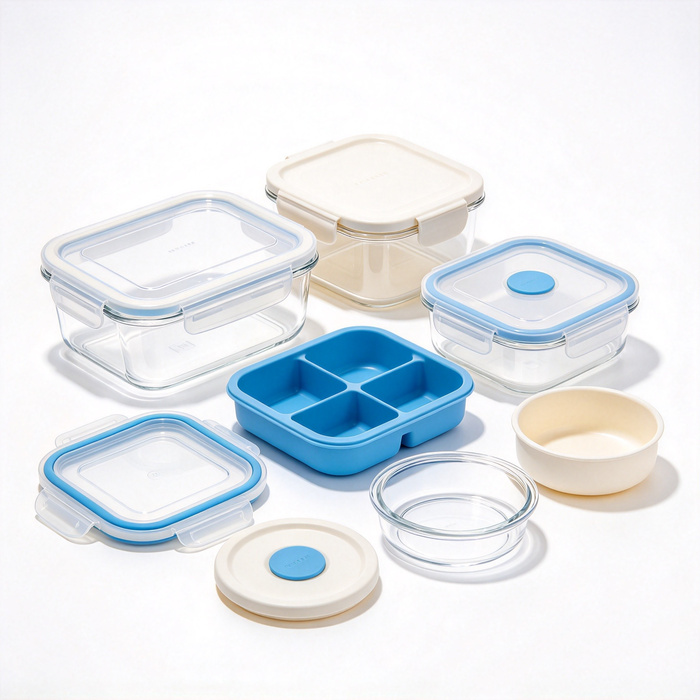
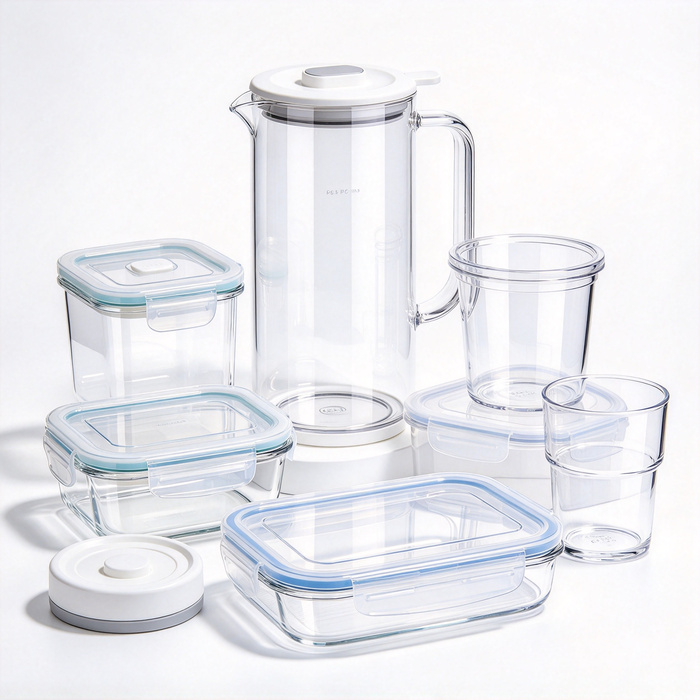
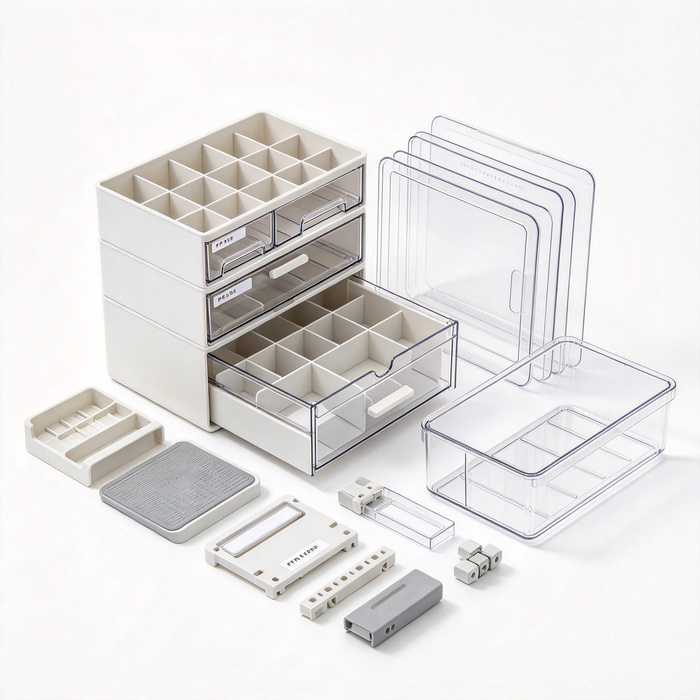
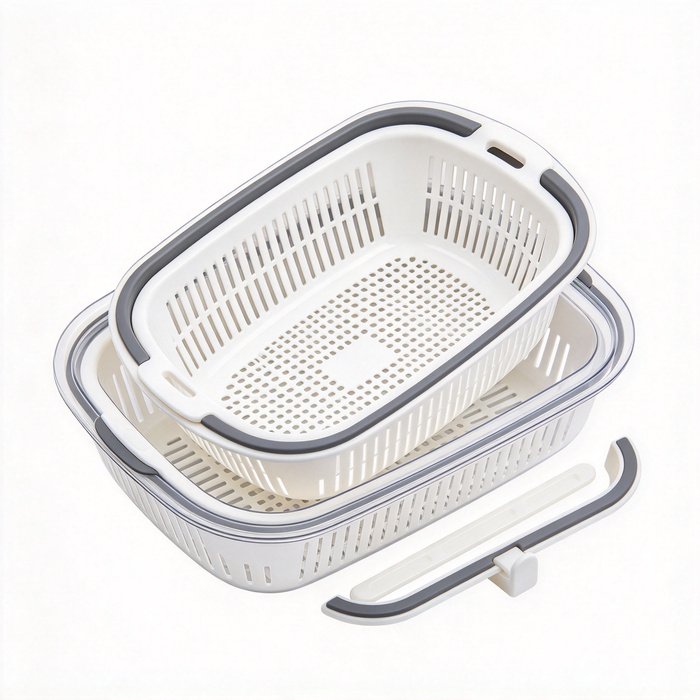
Transparent Container Body moulding
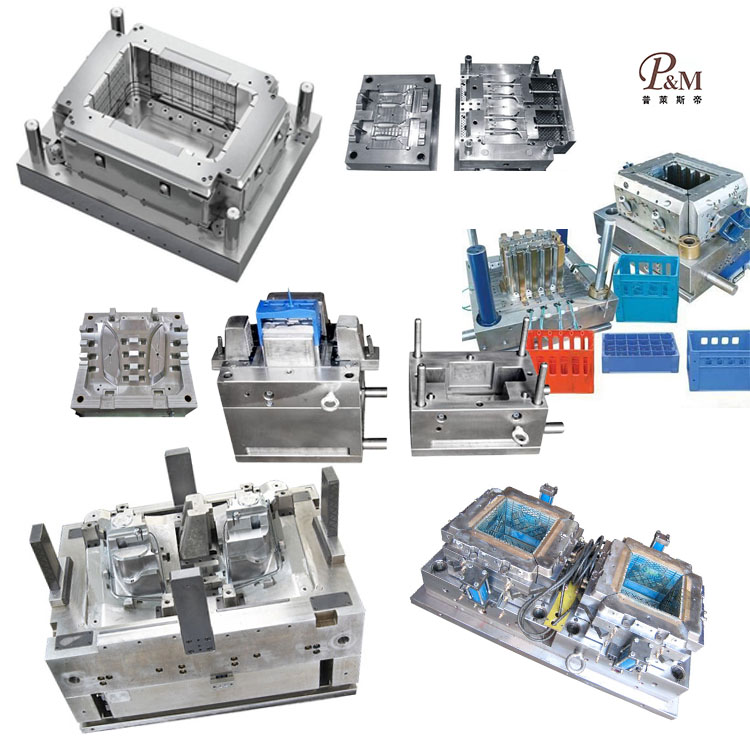
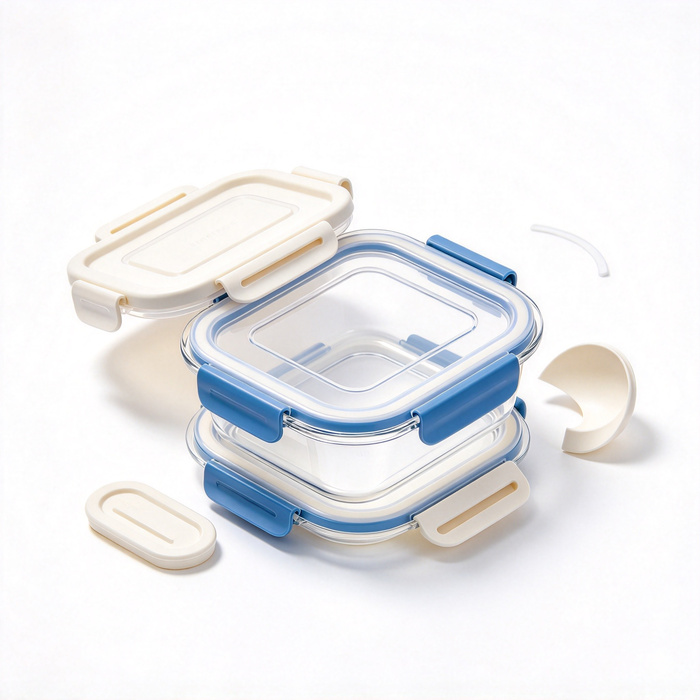
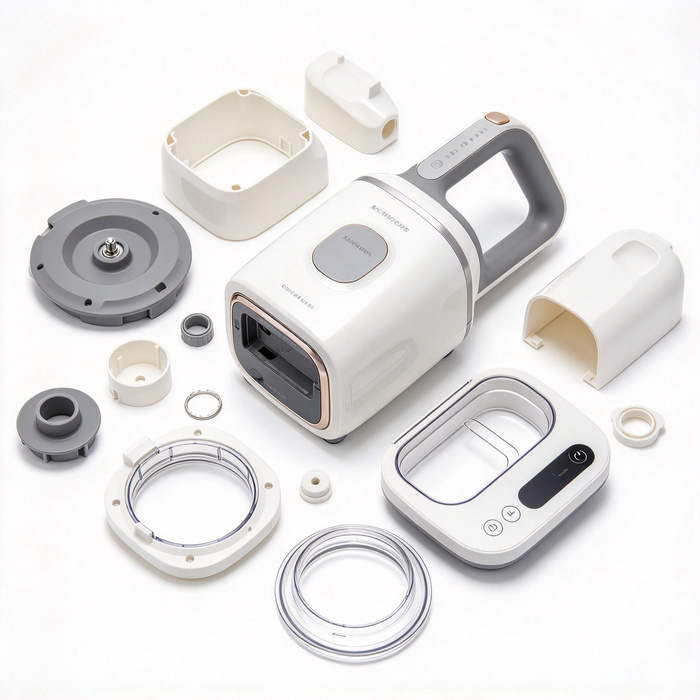
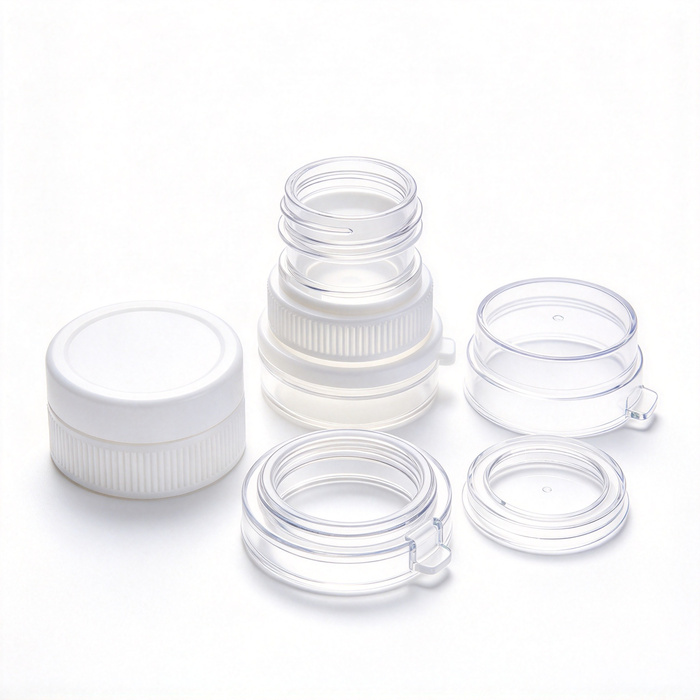
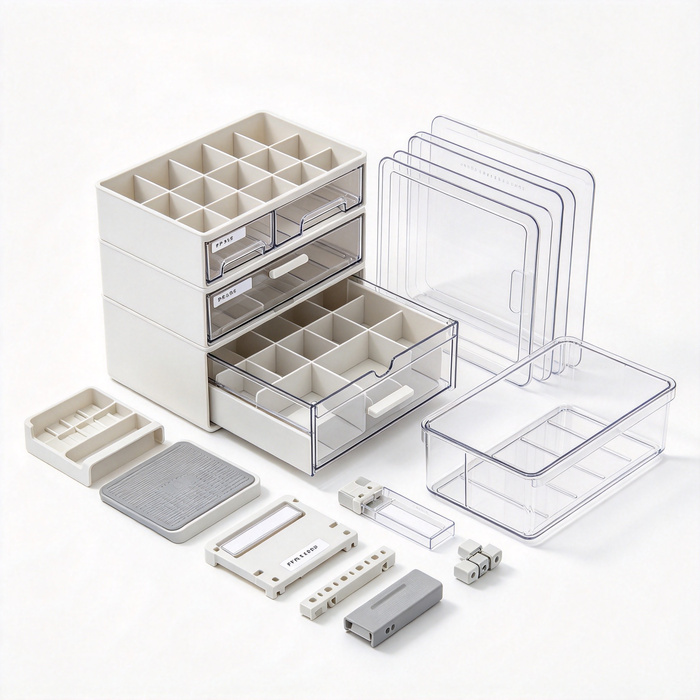
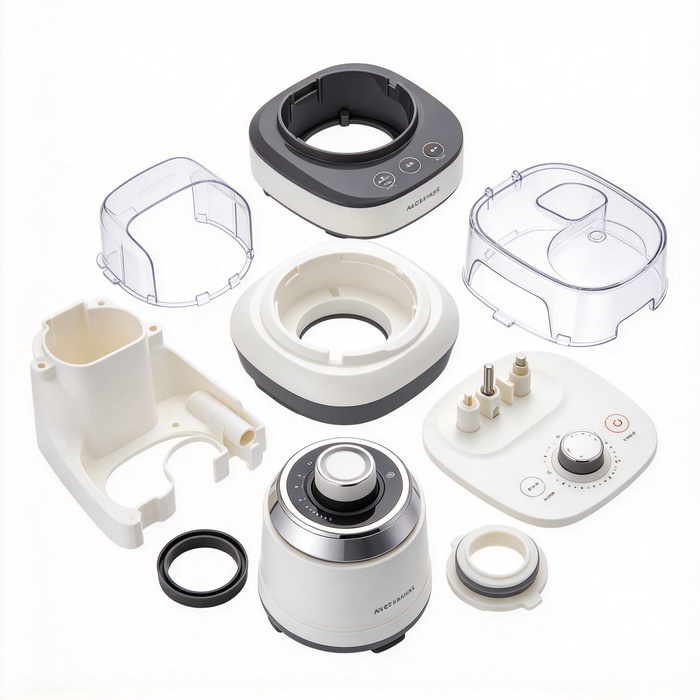
Ningbo (P&M) Plastic Metal Products Co., Ltd. has 17 years of mold manufacturing technology and can customize Transparent Container Body moulding. We provide professional customized Transparent Container Body moulding services, and we are a professional Transparent Container Body moulding manufacturer. We have sufficient experience in selecting product raw materials and mold materials. In the process of customizing Transparent Container Body moulding, our factory can provide one-stop service. We have design and production capabilities related to Transparent Container Body moulding, such as: CAD design, mold manufacturing, injection molding, plastic product production, assembly and other technologies.
Send Inquiry
Product Description
In addition, our company has established cooperative relationships with plastic raw material suppliers, printing manufacturers, etc. to ensure the supply of raw materials and printing quality. Through our rich experience and perfect supply chain, our company can provide customers with high-quality customized Transparent Container Body moulding products to meet their specific needs. At the same time, we have 10 years of professional foreign trade service experience, understand the foreign trade process, and better serve our customers. For Transparent Container Body moulding products, we can make corresponding plastic parts, which is mainly done through injection molds.
## Preliminary Phase: DFM + Material Validation (The Critical Starting Point for Transparent Parts)
### Common Materials (for Transparent Kitchen Containers)
- **Tritan (PCTG):** The industry standard. Dishwasher-safe, heat-resistant (100–110°C), resistant to stress cracking, and exhibits low birefringence. The preferred choice for kitchen appliances intended for export.
- **PETG:** Cost-effective with excellent light transmission; however, it has lower heat resistance and is unsuitable for prolonged exposure to high temperatures.
- **PC (Polycarbonate):** Offers high heat resistance (120°C+) and strong impact resistance. It is prone to stress cracking (requiring annealing) and may be subject to restrictions in certain markets due to Bisphenol A (BPA) content.
- **AS (SAN):** Highly transparent and rigid; however, it is brittle and lacks resistance to long-term exposure to hot water or detergent cycles.
- **Transparent PP:** Semi-transparent and microwave-safe, though its light transmission is inferior to the materials listed above.
>
> Compliance: Must meet standards such as GB 4806.7, FDA 21 CFR, or EU (No.) 10/2011. Raw materials must be accompanied by a Certificate of Analysis (COA), Technical Data Sheet (TDS), and migration test reports. Production must take place on a dedicated food-grade line; cross-contamination with standard-grade or recycled materials is strictly prohibited. If recycled material is used, it must be managed separately and subjected to ongoing migration testing.
### Structural DFM (Key Considerations for Transparent Containers)
1. **Uniform Wall Thickness:** Typically 1.2–2.0 mm. Abrupt changes in thickness easily lead to flow marks, internal stress, and "rainbow" patterns (birefringence). Rib thickness should be ≤ 50–60% of the main wall thickness.
2. **Corner Radii (R) ≥ 0.8 mm:** Prevents stress concentration at sharp corners.
3. **Draft Angles:** ≥ 2° for external (visible) surfaces; ≥ 2.5° for internal surfaces. Even minor surface scuffing or dragging is immediately visible on transparent parts.
4. **Gating Strategy:** Prefer fan gates or side gates to minimize shear. Avoid small pin-point gates, which can cause shear-induced whitening or yellowing. Position gates on non-primary viewing surfaces.
5. **Weld lines should ideally be positioned in areas that are neither visible nor subject to mechanical stress**; for parts with multiple injection gates, mold-flow simulation is mandatory.
6. Venting: Incorporate venting channels (0.01–0.03 mm deep) at the ends of the melt flow paths and in corners. (This depth is shallower than that used for standard plastics to prevent flash while effectively avoiding trapped air and burn marks.)
## II. Mold Preparation (Standards for molds producing transparent parts are significantly higher than those for general-purpose containers.)
- **Steel Selection**: Use 718H or S136H, hardened and tempered. Cavities must be polished to a mirror finish (A2/A3 grade, Ra ≤ 0.02 μm); any scratches or surface textures will be replicated on the final product.
- **Cooling Channels**: Arrange symmetrically, following the contour of the container to ensure uniform cooling; this helps control internal stress and the formation of "rainbow" patterns (birefringence).
- **Hot Runner System**: For multi-cavity molds or large-capacity containers, a valve-gated hot runner system is preferred. Ensure hot runner nozzles are polished and temperature control is precise to prevent "cold slugs" (solidified material spots) and yellowing.
- **Ejection System**: Use stripper plates or large-diameter ejector pins to distribute force; avoid single-point, high-pressure ejection, which can cause "whitening" (stress marks) or localized stress.
- **Parting Lines and Inserts**: All surfaces must be polished. Implement regular mold maintenance, including rust prevention and dust removal.
## III. Raw Material Pre-treatment (The stage most prone to failure)
For hygroscopic transparent resins (PC, PCTG, PETG), **drying is a mandatory process**. Inadequate drying will lead to silver streaks, bubbles, and hydrolytic degradation:
- PCTG (Tritan): 70–80°C, 4–6 hours; dew point ≤ -40°C
- PETG: 65–75°C, 4–6 hours
- PC: 120°C, 4–6 hours
- AS: 80°C, 2–4 hours
Operational Best Practices:
- Keep the drying hopper insulated. Once dried, avoid prolonged exposure of the material to the ambient air, as it may re-absorb moisture.
- - Implement enclosed dust-removal systems for raw material feeding; thoroughly clean the barrel, screw, and nozzle before switching materials (as these are the primary sources of black specks and impurities).
- Utilize a specialized low-shear screw with a length-to-diameter (L/D) ratio of 20–22:1 to minimize shear-induced heating, which can cause yellowing and an increase in haze.
We are a Transparent Container Body moulding manufacturer, providing high-quality Transparent Container Body moulding manufacturing. As long as you want to customize/develop Transparent Container Body moulding products, you can find us. We have professional injection mold design and mature manufacturing technology, providing you with one-stop service, from product design-mold making-product production-product packaging-product transportation, we can help you in every link. As long as you come to us, we will provide you with the ultimate service and satisfy you in terms of product quality, production time, information dialogue, etc.
|
Product Name |
Treadmill moulding |
|
Pls provide |
2D, 3D, samples, or the size of the multi-angle pictures |
|
Mould Time |
20-35 Days |
|
Product time |
7-15 Days |
|
Mould precision |
+/-0.01mm |
|
Mould life |
50-100 million shots |
|
Producing Process |
Audit drawings - mold flow analysis - design validation - Custom Materials - mold processing - core processing - electrode machining - Runner system processing - parts processing and procurement - machining acceptance - cavity surface treatment process - complex mode Die - The entire mold surface coating - Mounting plate - mold sample - sample test - sending samples |
|
Mould cavity |
One cavity, multi-cavity or same different products be made together |
|
Mould material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Runner system |
Hot runner and cold runner |
|
Base material |
P20,2738,2344,718,S136,8407,NAK80,SKD61,H13 |
|
Finish |
Pitting the word, mirror finish, matte surface, striae |
|
Standard |
HASCO, DME or dependent upon |
|
Main technology |
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes, surface Finish, etc. |
|
Software |
CAD,PRO-E,UG Design Time: 1-3 days (normal circumstances) |
|
Product material |
ABS,PP,PC,PA6,PA66,TPU,POM,PBT,PVC,HIPS,PMMA,TPE,PC/ABS,TPV,TPO,TPR,EVA,HDPE,LDPE,CPVC,PVDF,PPSU.PPS. |
|
Quality system |
ISO9001:2008 |
|
Establish time |
20days |
|
Equipment |
CNC,EDM,Cutting off Machine,plastic machinery,etc plastic suitcase mould zhe jiang |
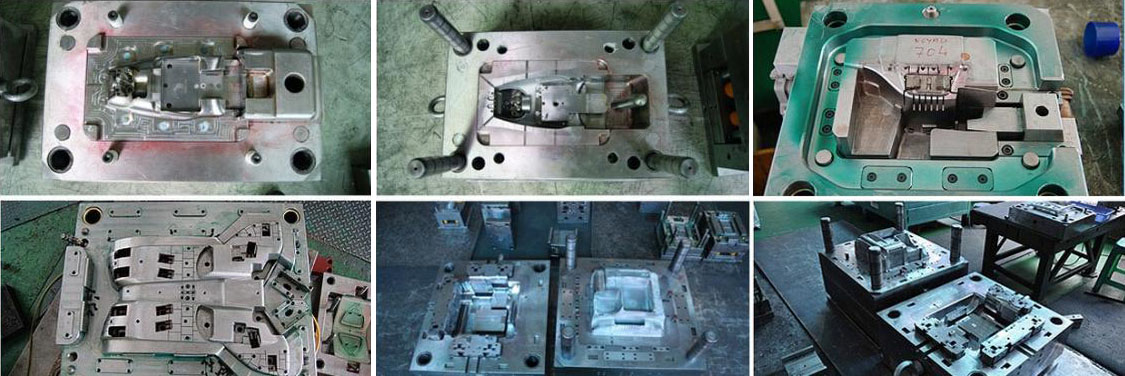
Plastic Injection Mould making
Plastic molding specifications
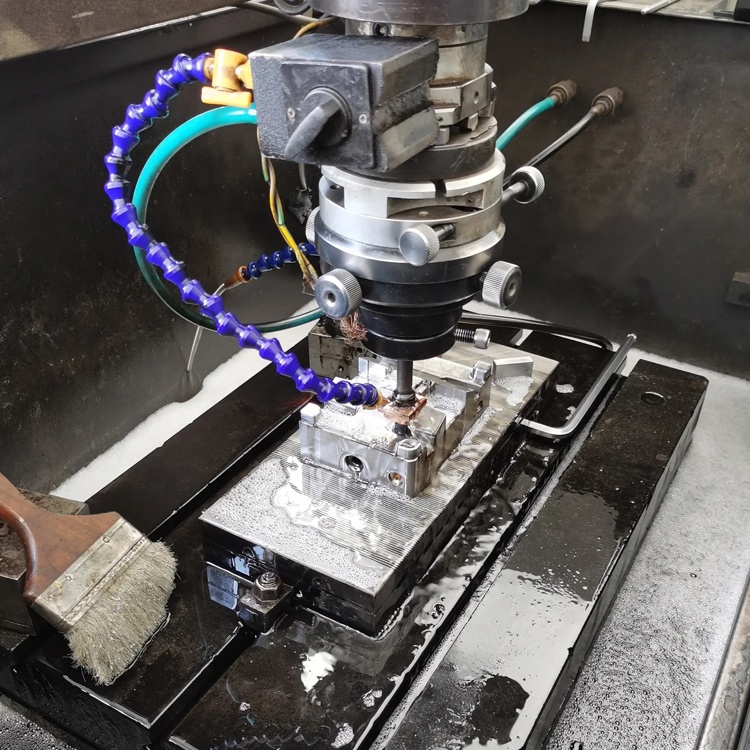
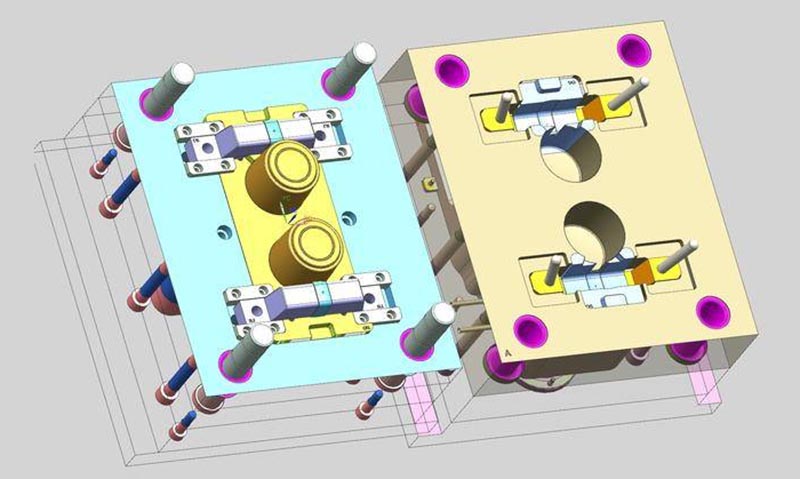
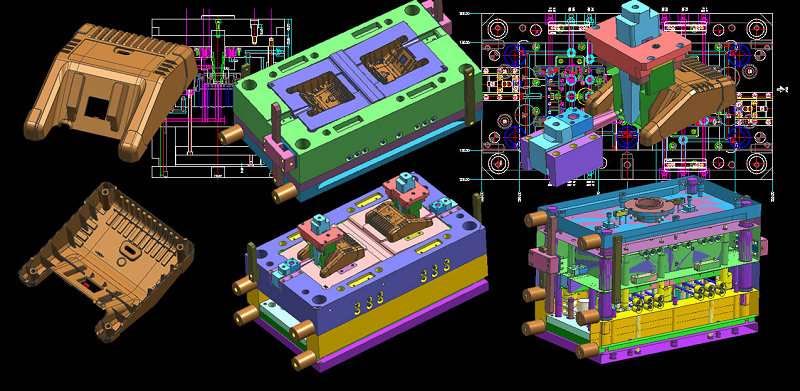
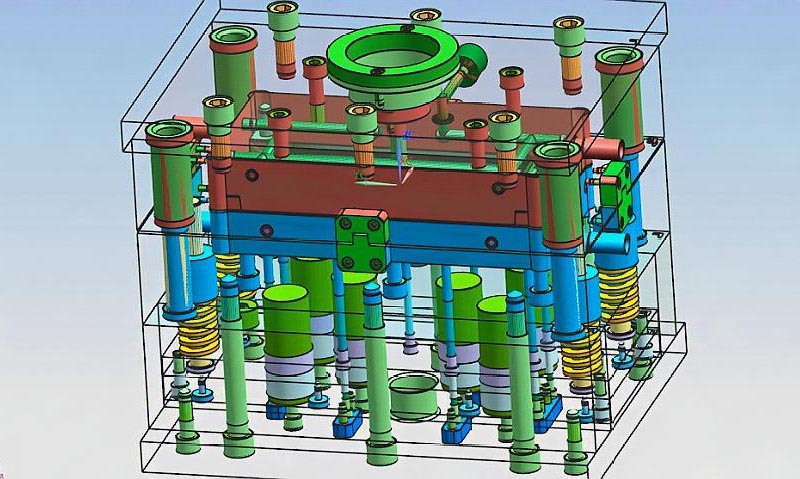
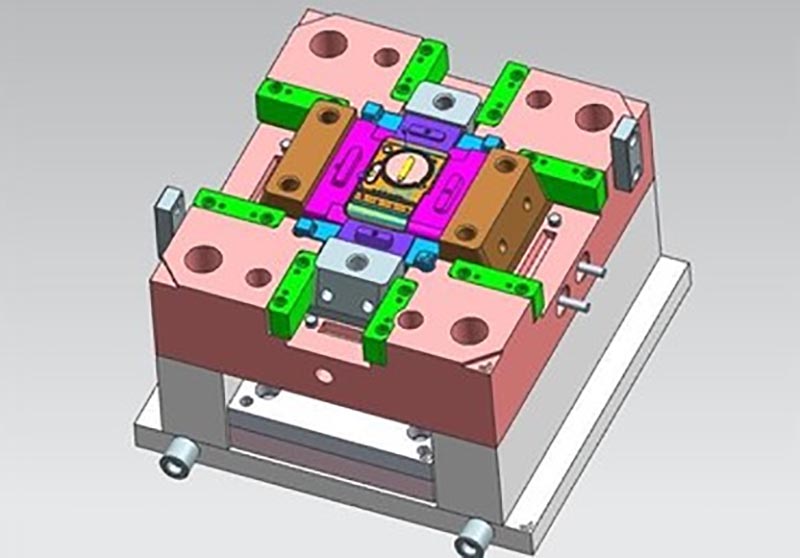
Mold design:
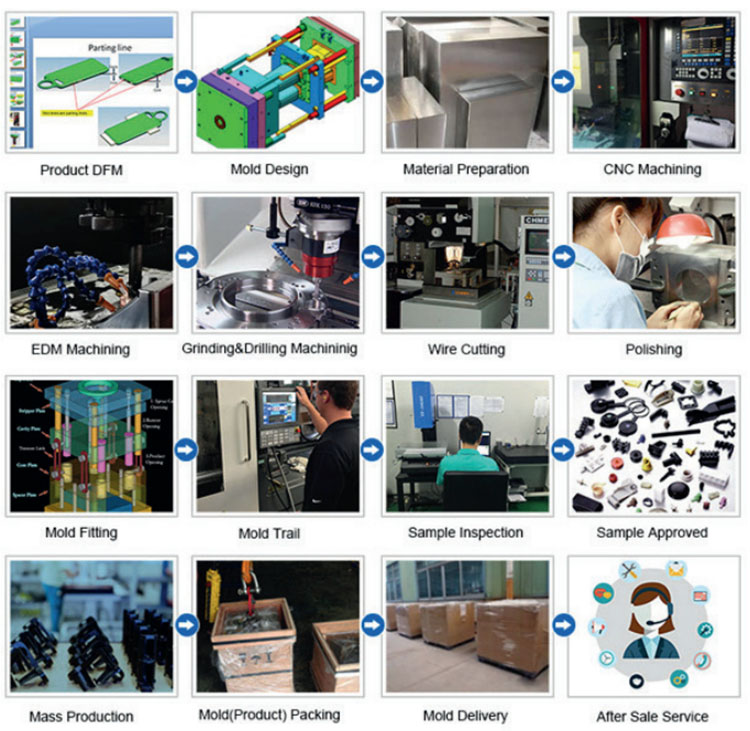
Transaction process:
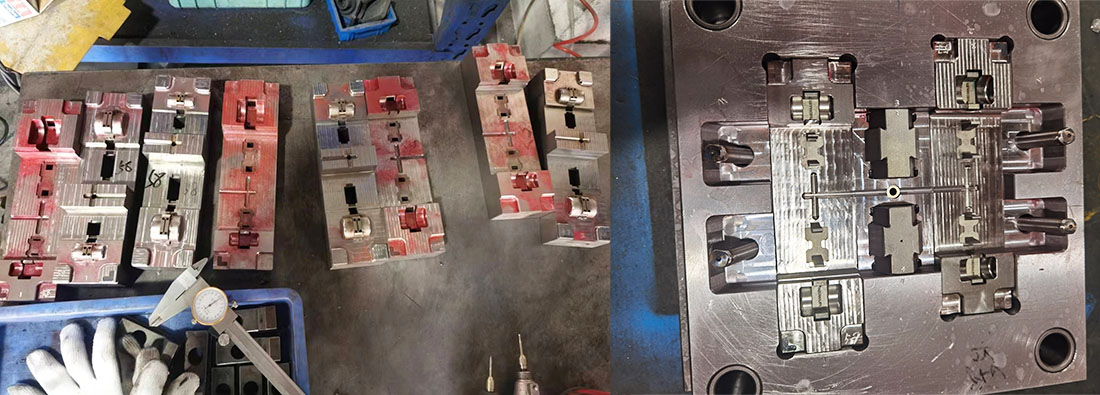
Mold testing:

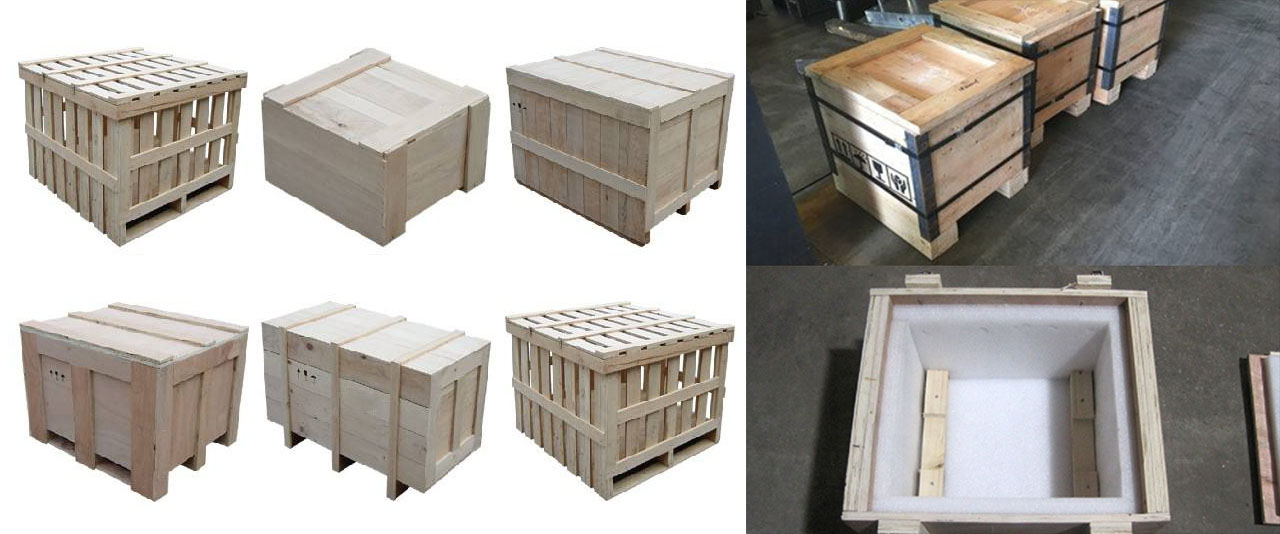
Product packaging
Factory
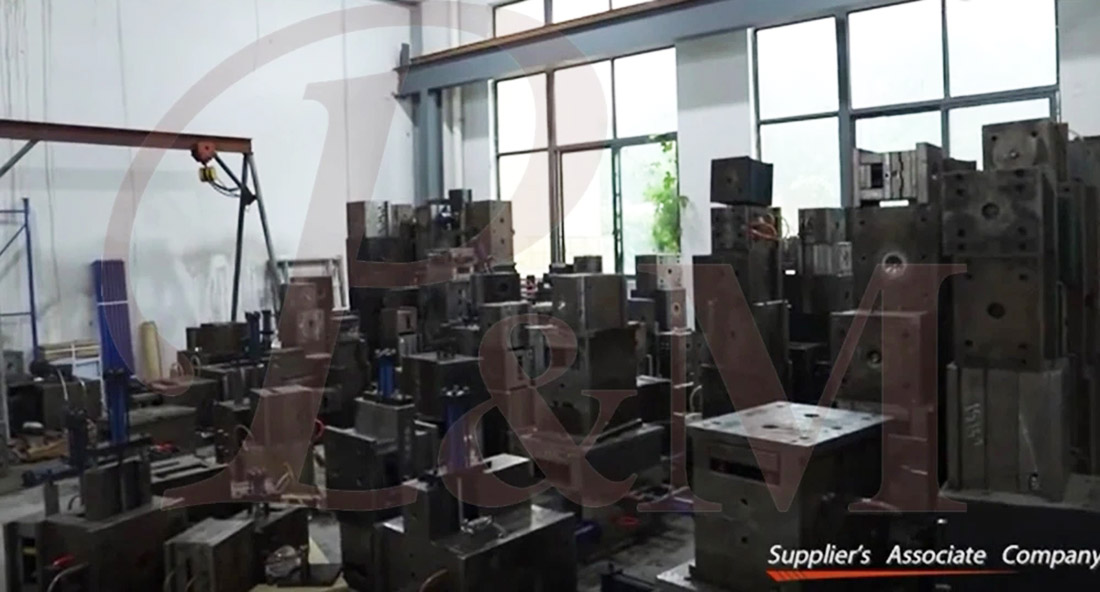
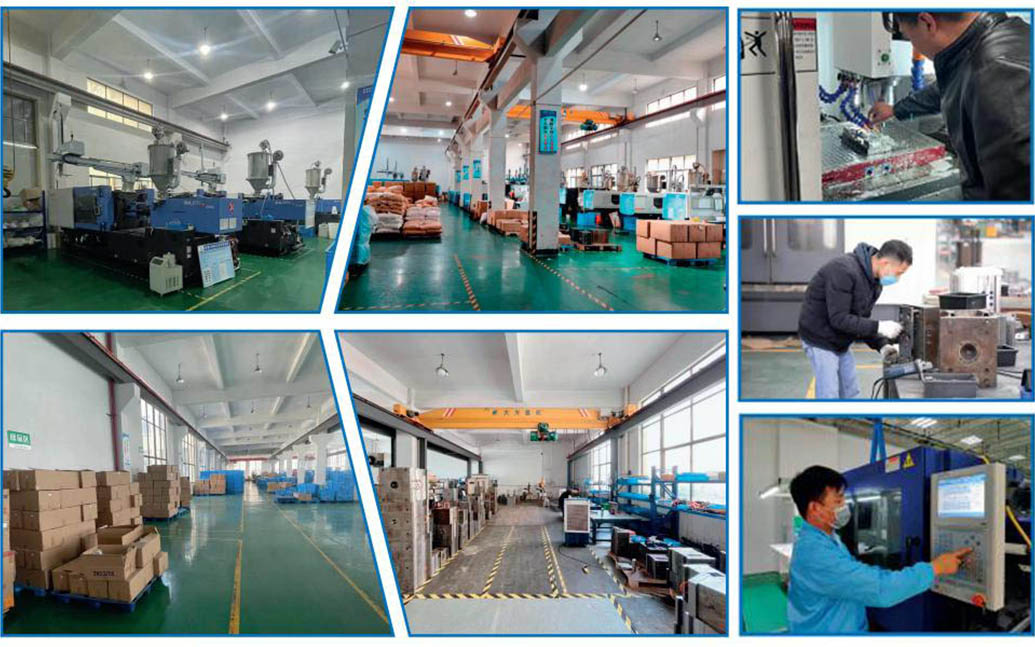
We are Custom Plastic Mold factory. Our factory is plastic injection mold maker. we has 17 years of experience in professional custom plastic mold and 10 years of foreign trade experience. We are custom Plastic Mold supplier. We can provide custom Plastic Mold service. Our factory can make the Injection molded plastic parts, and the quality of the products will satisfy you.
We have more than 50 high-end machines and hundreds of engineers and designers. We can provide one-stop service, from product design - mold making - product production - product packaging - transportation. We have a complete production chain. We can meet all your requirements.
Services we provide:
Professional custom mold service, Plastic mold design and manufacturing .plastic product production, product design, mold design, blow mold customization, rotational mold customization, die-casting mold customization. 3D printing services, CNC manufacturing services, product packaging, customized packaging, shipping services.
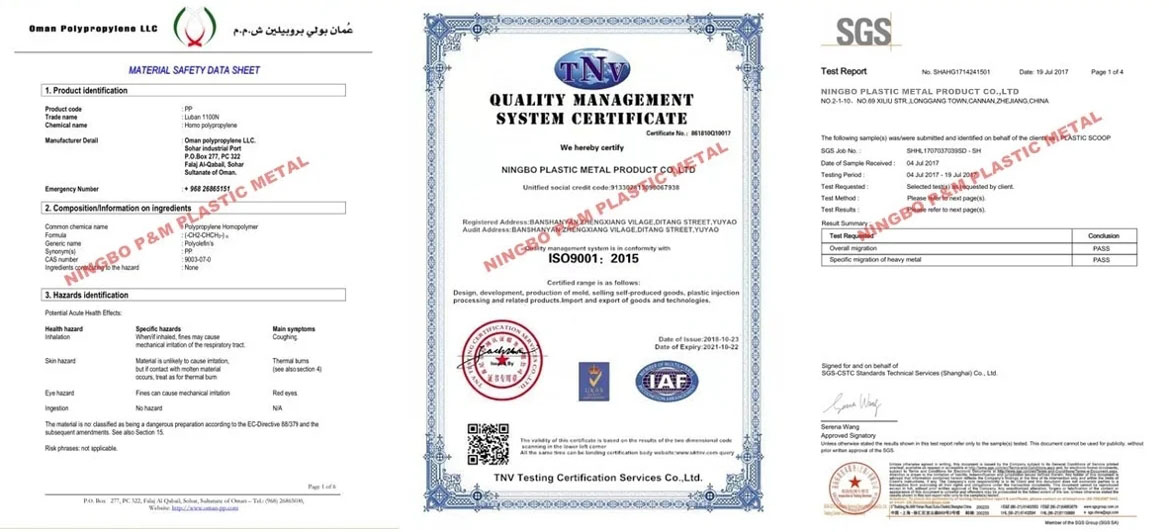

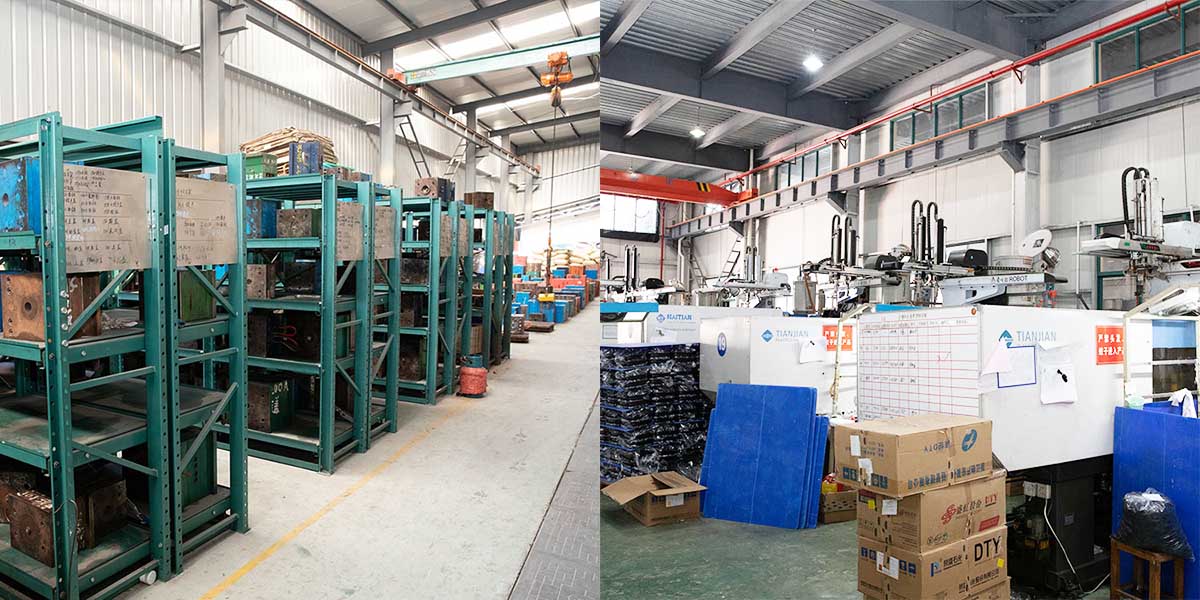
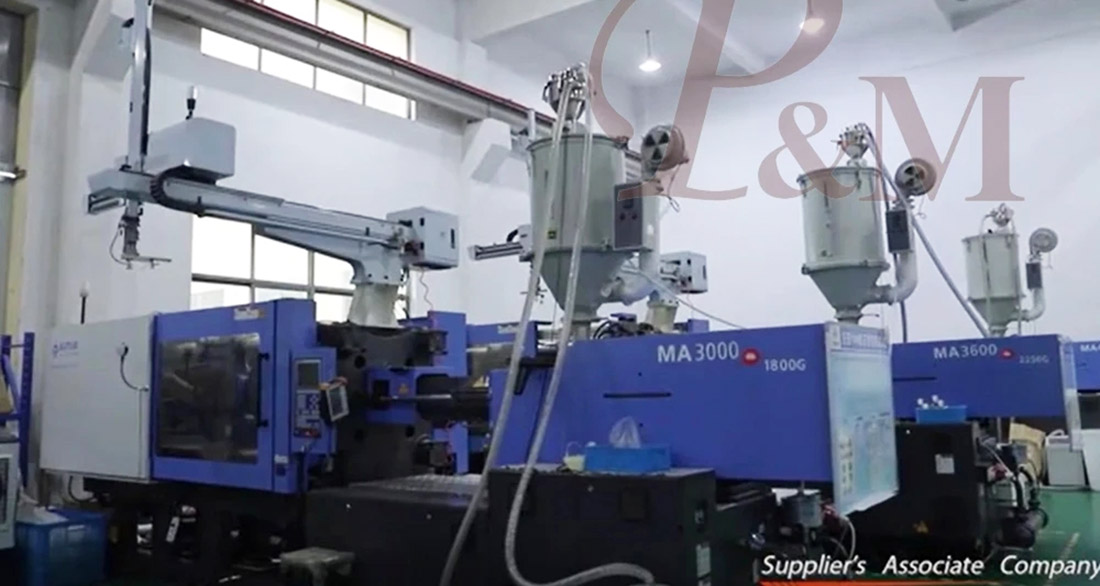
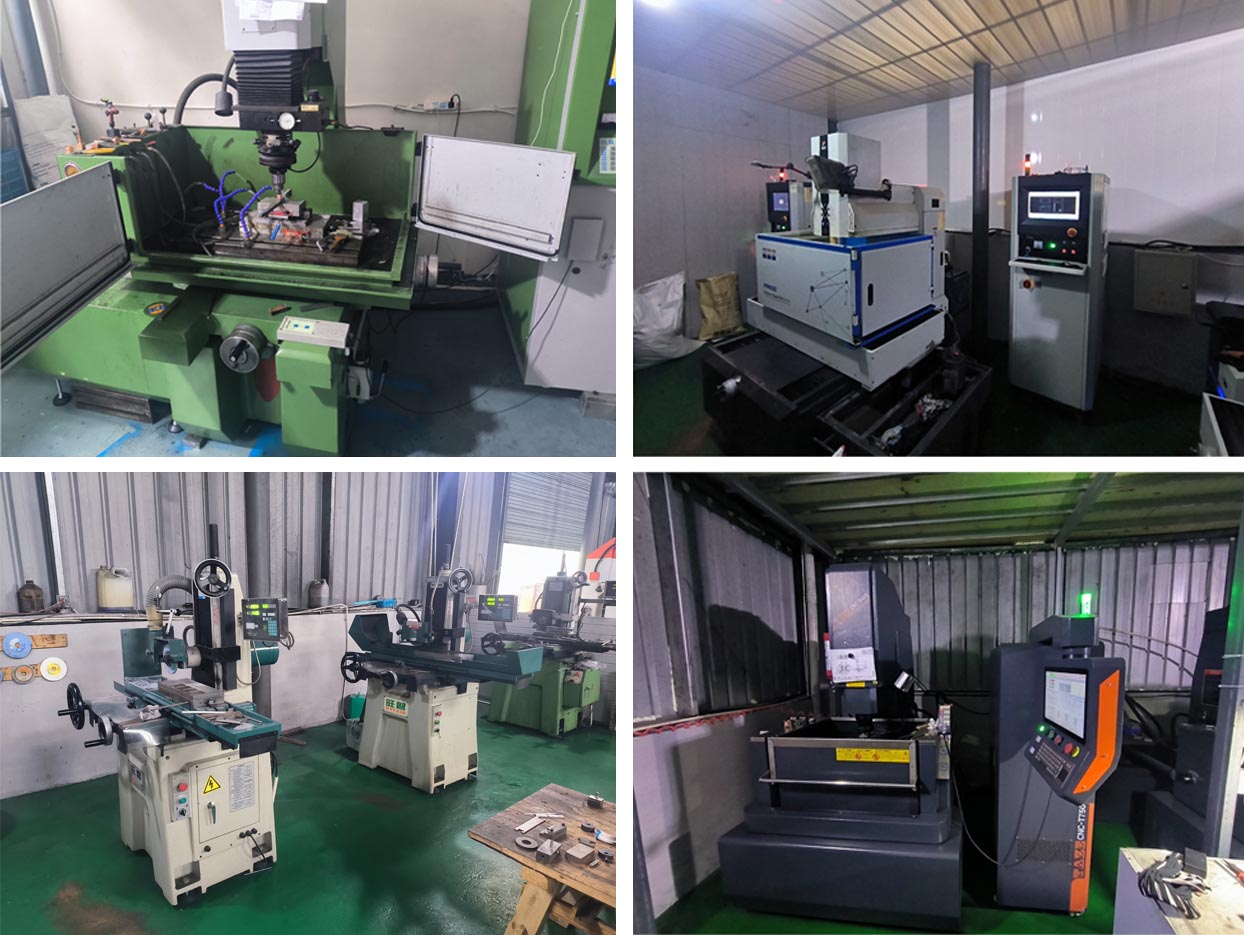
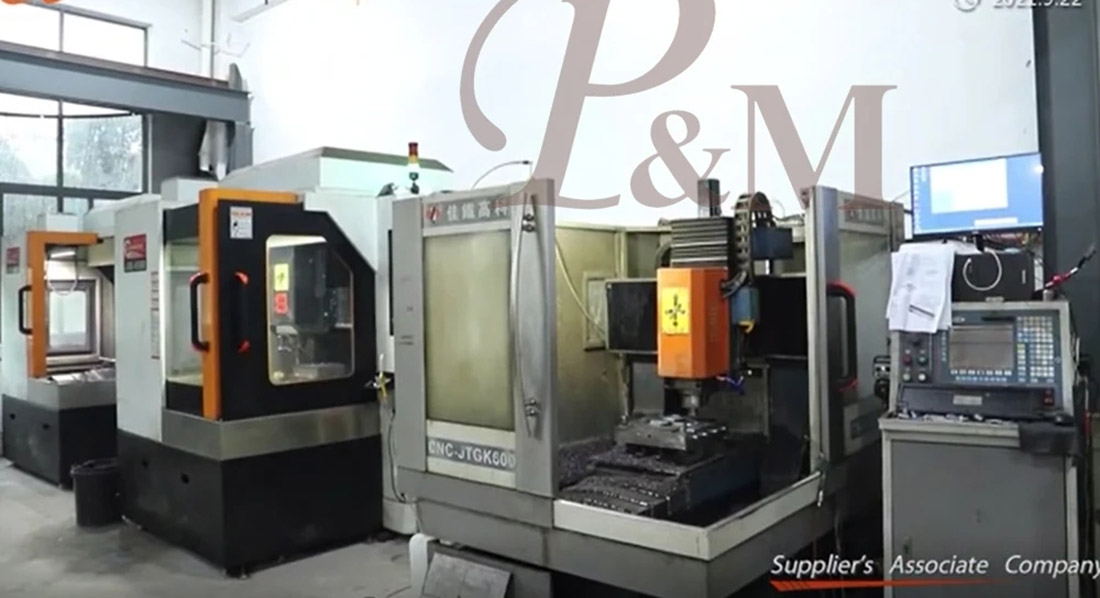
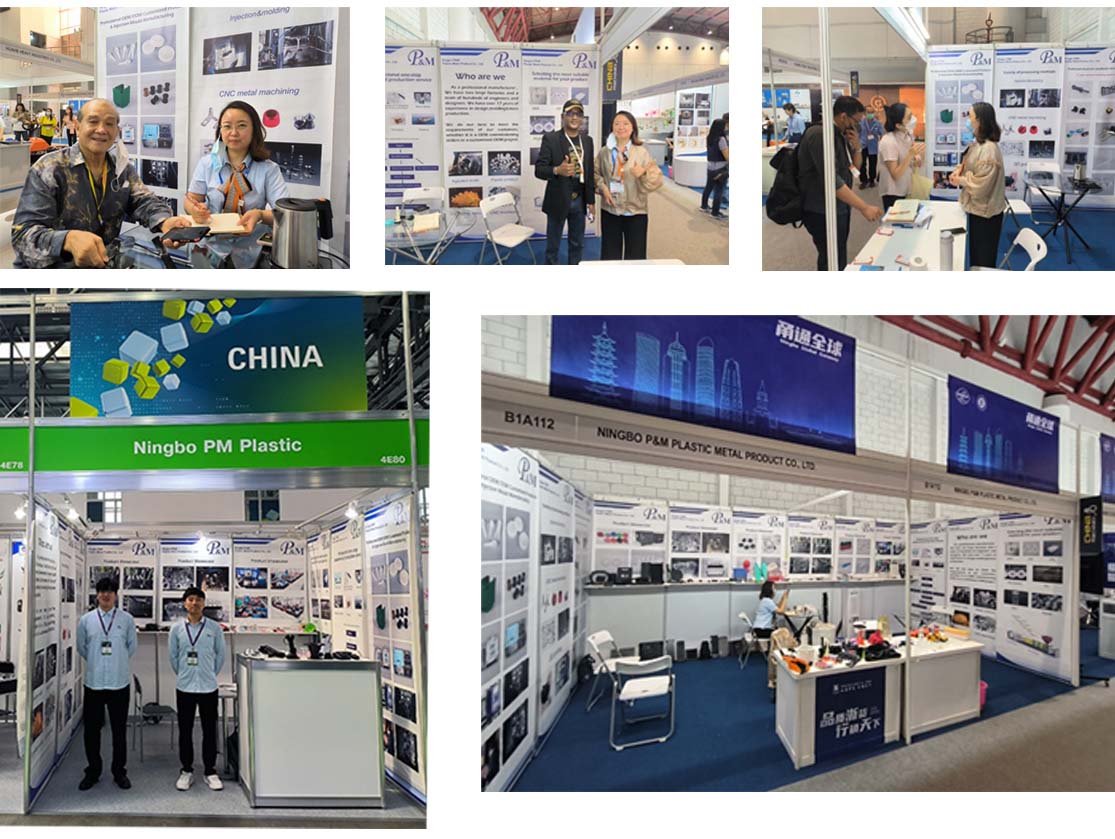
We always adhere to the principles of quality first and time first. While providing customers with the highest quality products, try to maximize the production efficiency and shorten production time. We are proud to tell every customer that our company has not lost any customer since its establishment.If there is a problem with the product, we will seek a solution actively and take responsibility to the end.

FAQ
Q1: Are you trading company or manufacturer ?
A: We are manufacturers.
Q2. When can I get the quotation?
A: We usually quote within 2 days after we get your inquiry.
If you are very urgent, please call us or tell us in your email so that we can quote for you first.
Q3. How long is the lead-time for mold?
A: It all depends on the products' size and complexity. Normally, the lead time is 25 days.
Q4. I have no 3D drawing, how should I start the new project?
A: You can supply us a molding sample, we will help you finish the 3D drawing design.
Q5. Before shipment, how to make sure the products quality?
A: If you don't come to our factory and also don't have the third party for inspection, we will be as your inspection worker.
We will supply you a video for production process detail include process report, products size structure and surface detail, packing detail and so on.
Q6. What is your payment terms?
A: Mold Payment: 40% deposit by T/T in advance, 30% second mold payment before sending out the first trial samples, 30% mold balance after you agree the final samples.
B:Production Payment: 50% deposit in advance, 50% before sending out the final goods.
Q7: How do you make our business long-term and good relationship?
A:1. We keep good quality and competitive price to ensure our customers benefit for best quality products.
2. We respect every customer as our friend and we sincerely do business and make friends with them, no matter where they come from.
Related Category
Send Inquiry
Please feel free to give your inquiry in the form below. We will reply you in 24 hours.